Auto-Reversing
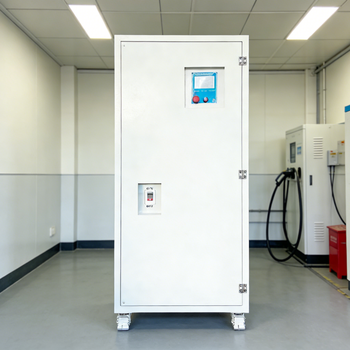
48V 625A 30kW Auto-Reversing Supply
- Output Voltage0–48V DC Adjustable
- Current Range0–625A High Current
- Reversal ControlSolid-State H-Bridge Timer
- InterfaceRS485 Modbus-RTU
MOQ: 1 Set (OEM Available)
In cooling towers, central HVAC systems, reverse osmosis pre-treatment, and high-salinity industrial loops, limescale formation and microbial biofilms cause massive heat transfer penalties, energy losses, and unscheduled shutdowns. A water treatment descaling power supply provides the electro-catalytic backbone required to extract scale without chemicals.
Modern industrial plants have rapidly transitioned away from environmental-hostile chemical scale inhibitors, anti-scalants, and harsh hydrochloric acid flushes. The core mechanism of electrolytic descaling harnesses an exact, constant-current DC field delivered to mixed metal oxide (MMO) coated titanium anodes and stainless-steel or titanium cathode mesh.
As cooling water passes through the reactor cell, the regulated electric field splits water molecules at the cathode: 2H₂O + 2e⁻ → H₂↑ + 2OH⁻. This drives localized boundary pH above 9.5, transforming soluble calcium bicarbonate [Ca(HCO₃)₂] into insoluble calcium carbonate precipitate: Ca²⁺ + HCO₃⁻ + OH⁻ → CaCO₃↓ + H₂O. Hardness crystallizes on the collection electrode instead of choking the chiller bundle.
Concurrently, at the anode, trace natural chloride ions are converted into active chlorine, hypochlorous acid, ozone, and hydroxyl free radicals (·OH), destroying legionella, filamentous algae, and microbial slime matrices automatically.
Guangdong Fenvix Technology Co., Ltd. supplies fully tested, high-frequency IGBT-based DC power supplies tailored for variable conductivity wastewater, industrial cooling water, and zero-liquid-discharge (ZLD) systems.


As international environmental regulations tighten and zero-liquid-discharge mandates accelerate, procurement managers and EPC system integrators must align their equipment specifications with several decisive industrial market shifts.
Historically, heavy water electrolysis systems utilized bulky 50/60Hz silicon-controlled rectifiers (SCR). SCR units present serious drawbacks: massive iron-core footprints, power factors dropping below 0.70 during partial loads, and sluggish step-response times. Modern municipal and commercial procurement mandates require high-frequency IGBT switching (20kHz to 50kHz), providing compact installations, power factor correction (>0.95), and energy savings in excess of 18% per cubic meter treated.
Raw water chemistry changes dynamically due to seasonal evaporation, blowdown intervals, rainwater dilution, and variable chemical makeup. A static voltage power supply causes destructive over-current tripping when conductivity surges, or zero scale precipitation when water is resistive. Sourcing requirements now mandate digital microprocessor intelligence that dynamically monitors cell impedance (V/I), maintaining precise current density without manual intervention.
Mechanical transfer switches inevitably suffer from arc pitting, mechanical wear, and slow reversal latency under load. The global procurement consensus strictly specifies solid-state electronic H-bridge inversion with programmable dead-band ramp-down. This prevents cathode passivation, eliminates contactor failures, and triples electrode working lifespan.
Verify that the power supply features minimum 2.5kV galvanic isolation between AC mains and DC electrolytic outputs to guard against line surges and earth faults.
Water treatment plants harbor saturated relative humidity, chlorine gas, and sulfate vapours. Demand anti-corrosion cabinet coatings and conformal coated PCBA.
Prevent interference with municipal SCADA PLCs, smart meters, and campus electronics by requesting active PFC and low ripple output filters.
The electrochemical descaling sector is rapidly evolving from basic DC power delivery toward fully integrated, intelligent water management solutions.
Next-generation wide-bandgap SiC semiconductors allow switching speeds surpassing 100kHz, cutting thermal dissipation in half and enabling smaller transformer geometries.
Switching from basic square waves to high-frequency pulse-reversal waveform modulation dislodges microscopic aragonite crystals before dense calcification forms on titanium plates.
Direct integration of pH, ORP, and conductivity sensors into the rectifier's CPU allows real-time current modulation, optimizing power draw based on actual scaling load.
Hermetically sealed liquid-cooled cabinets eliminate outside air intake altogether, providing unconditional immunity to ambient hydrogen sulfide, moisture, and chlorine vapors.
Use our field-validated matrix to determine voltage, current, and reversal frequency for your industrial water treatment project.
| Application Scenario | Raw Water Conductivity | Recommended Voltage Compliance | Current Density per Cell Area | Optimal Polarity Cycle | Recommended Model Architecture |
|---|---|---|---|---|---|
| Central Chiller Cooling Towers | 400 – 1,500 µS/cm | 24V – 36V DC | 100 – 180 A/m² | Forward 2h / Reverse 5min | Fenvix 36V 300A Auto-Reverse IGBT |
| High Hardness Deep Well Water | 800 – 2,500 µS/cm | 36V – 48V DC | 150 – 250 A/m² | Forward 90min / Reverse 8min | Fenvix 48V 625A Heavy-Duty System |
| RO Brine & High Salinity Wastewater | > 5,000 µS/cm | 12V – 24V DC | 250 – 450 A/m² | Forward 60min / Reverse 10min | Fenvix 24V 1000A Water-Cooled Unit |
| District Heat Exchange Circuits | 300 – 800 µS/cm | 48V – 64V DC | 80 – 140 A/m² | Forward 3h / Reverse 5min | Fenvix 64V 500A High-Voltage Rectifier |
Need a custom voltage or multiple independent output zones? Guangdong Fenvix Technology Co., Ltd. customizes transformer windings, firmware parameters, and busbar layouts to meet your exact electrochemical requirements.
Answers to technical, operational, and commercial questions frequently posed by plant engineers, system integrators, and procurement teams.
Engineering excellence, advanced in-house metalworking, and comprehensive quality assurance since 2013.
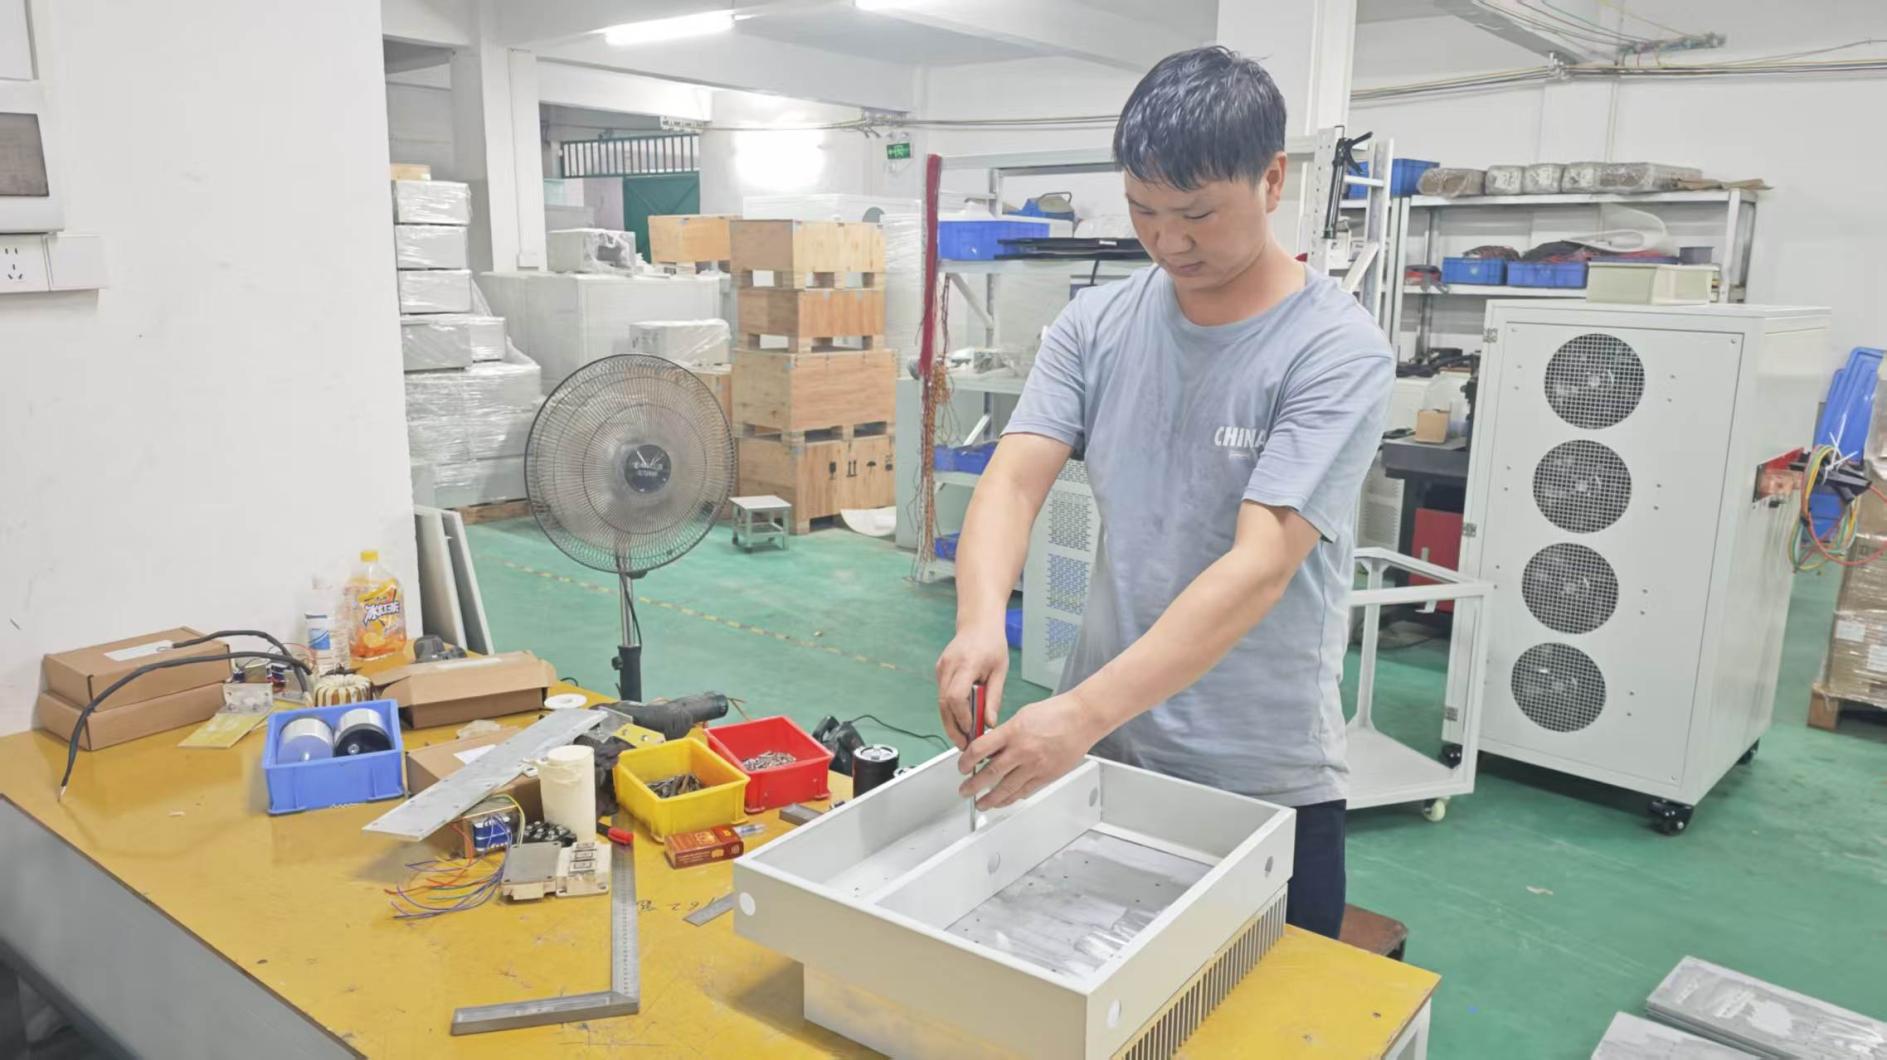
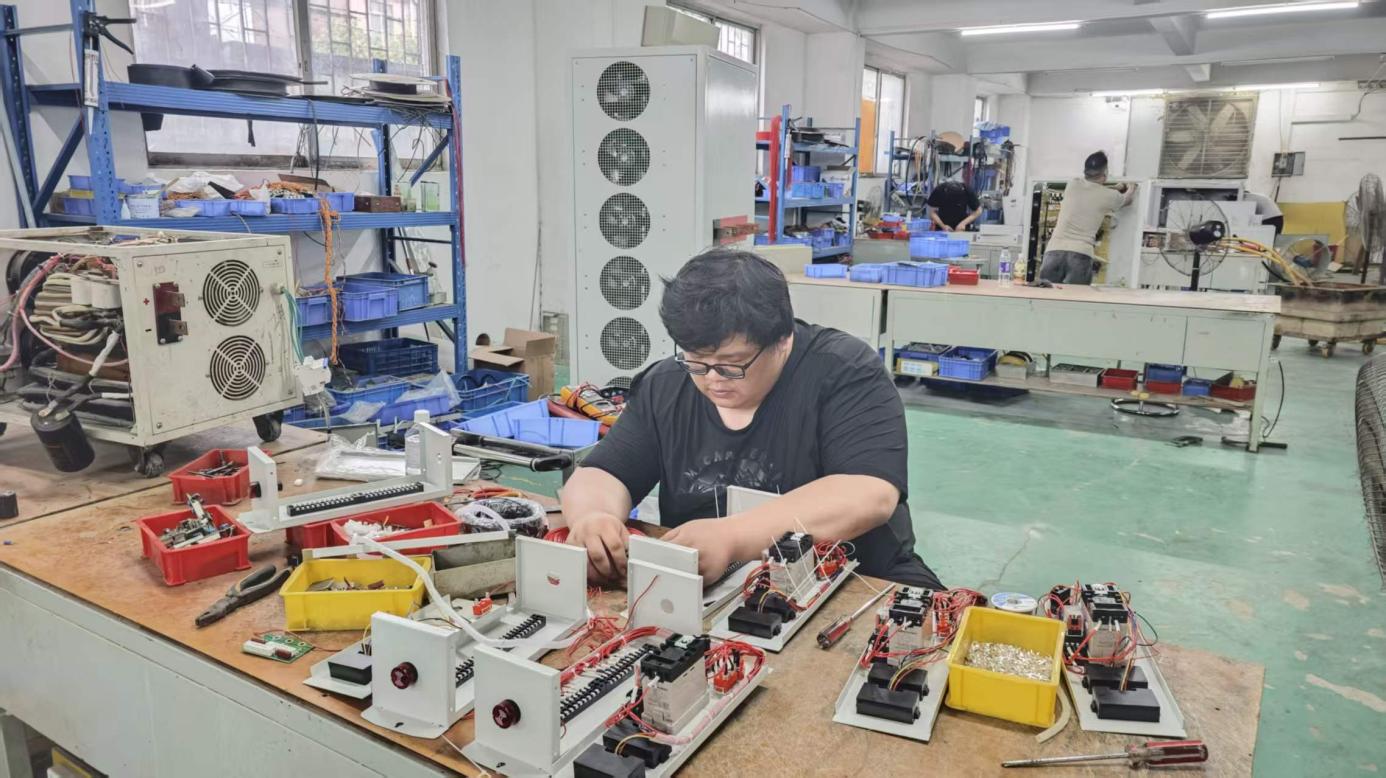
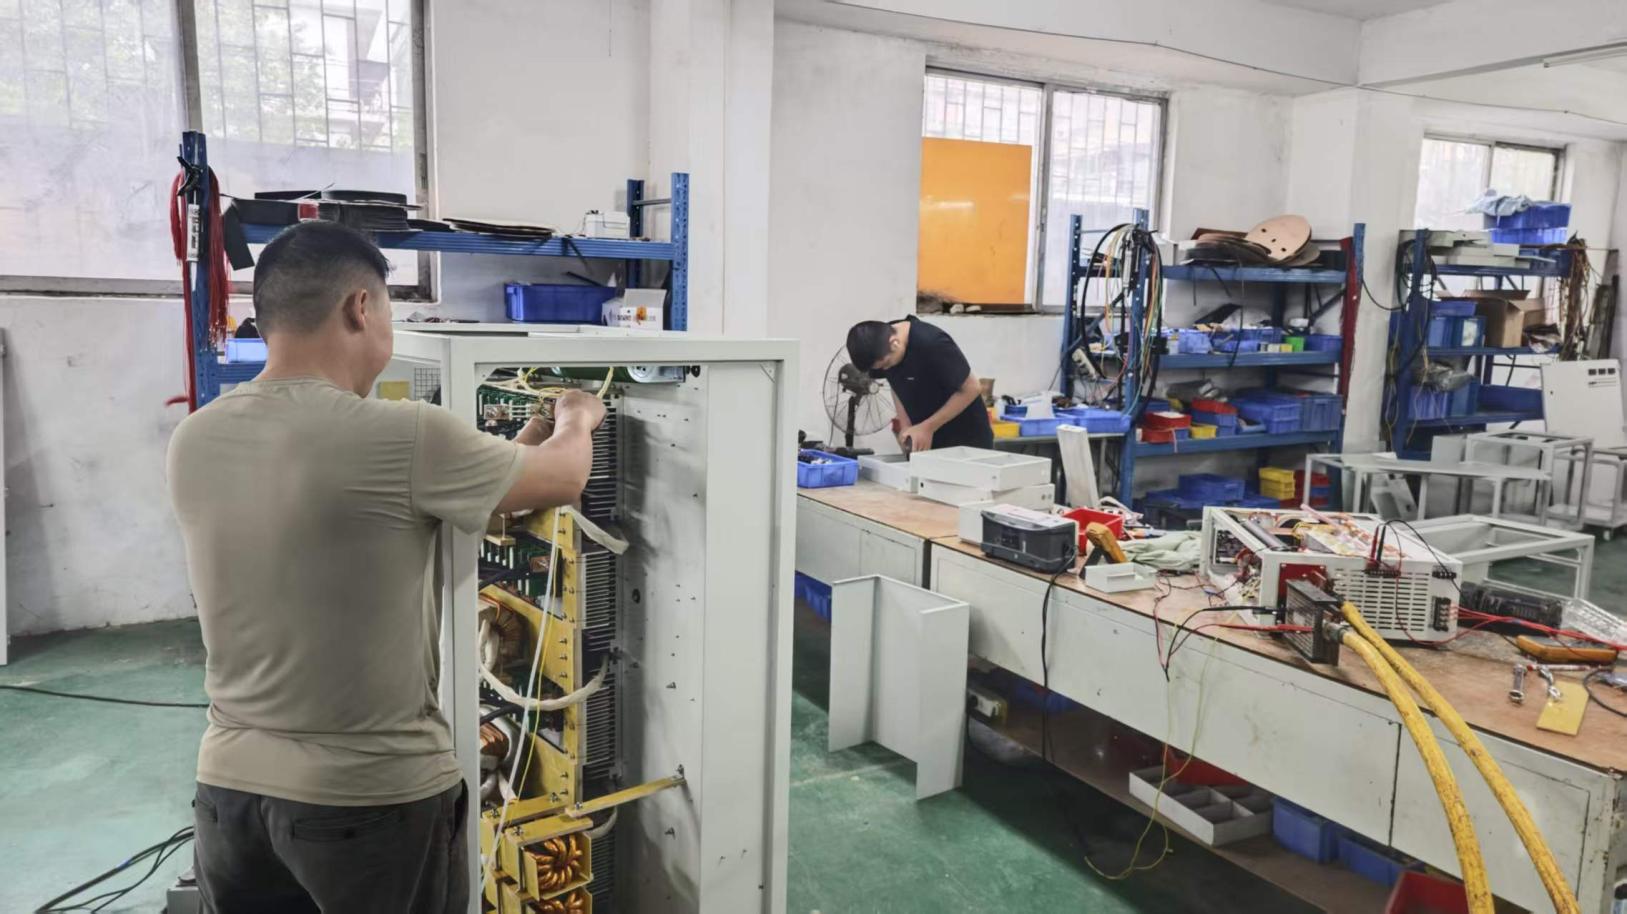
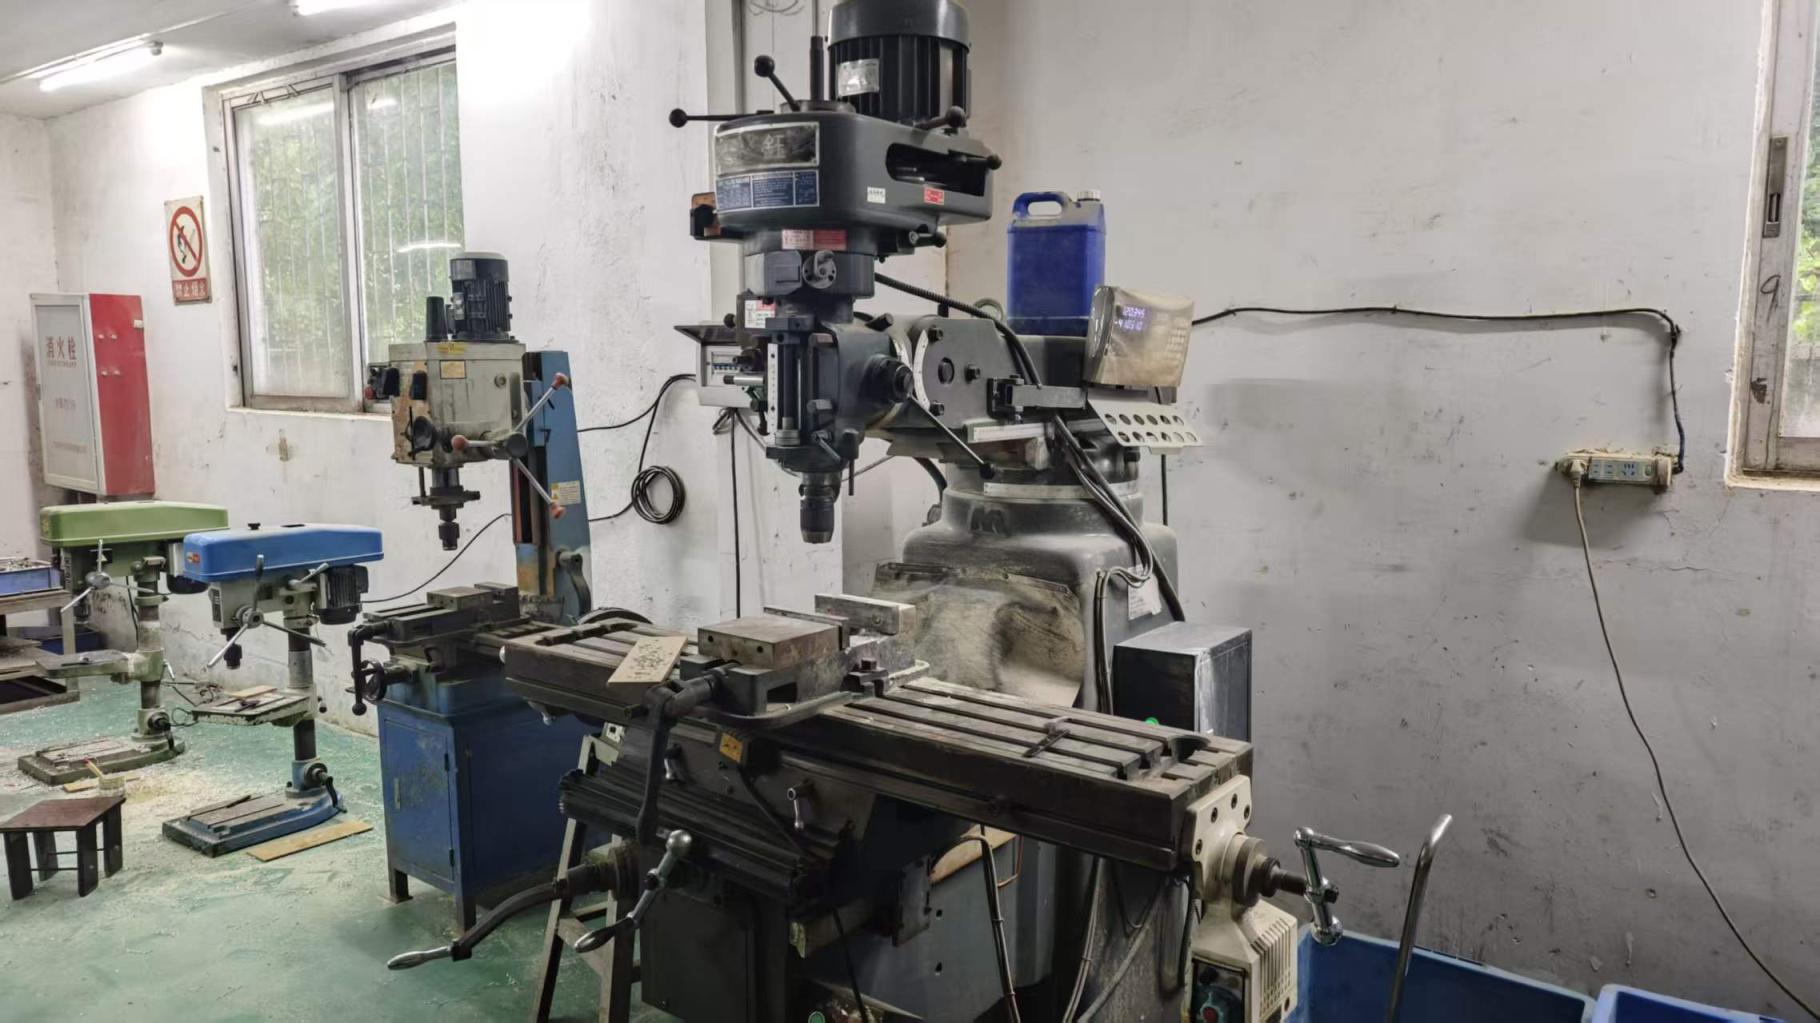
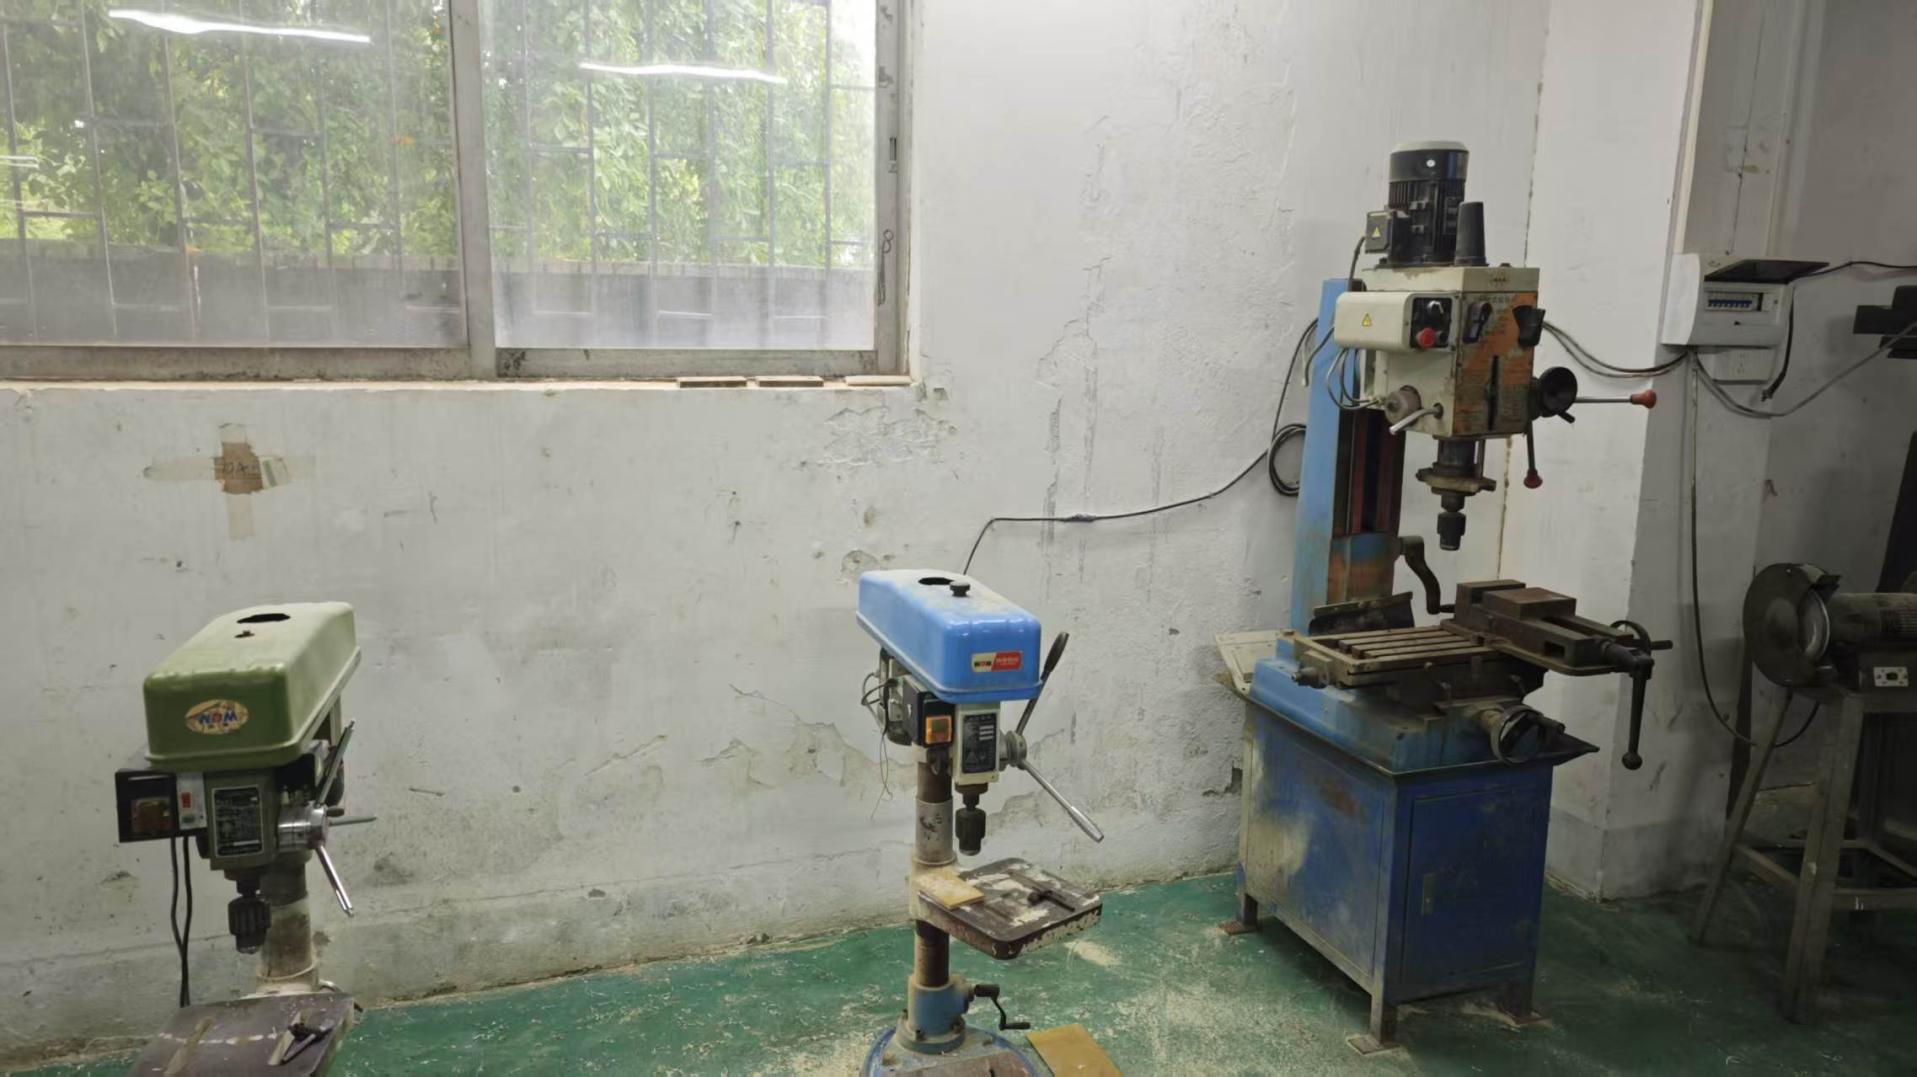
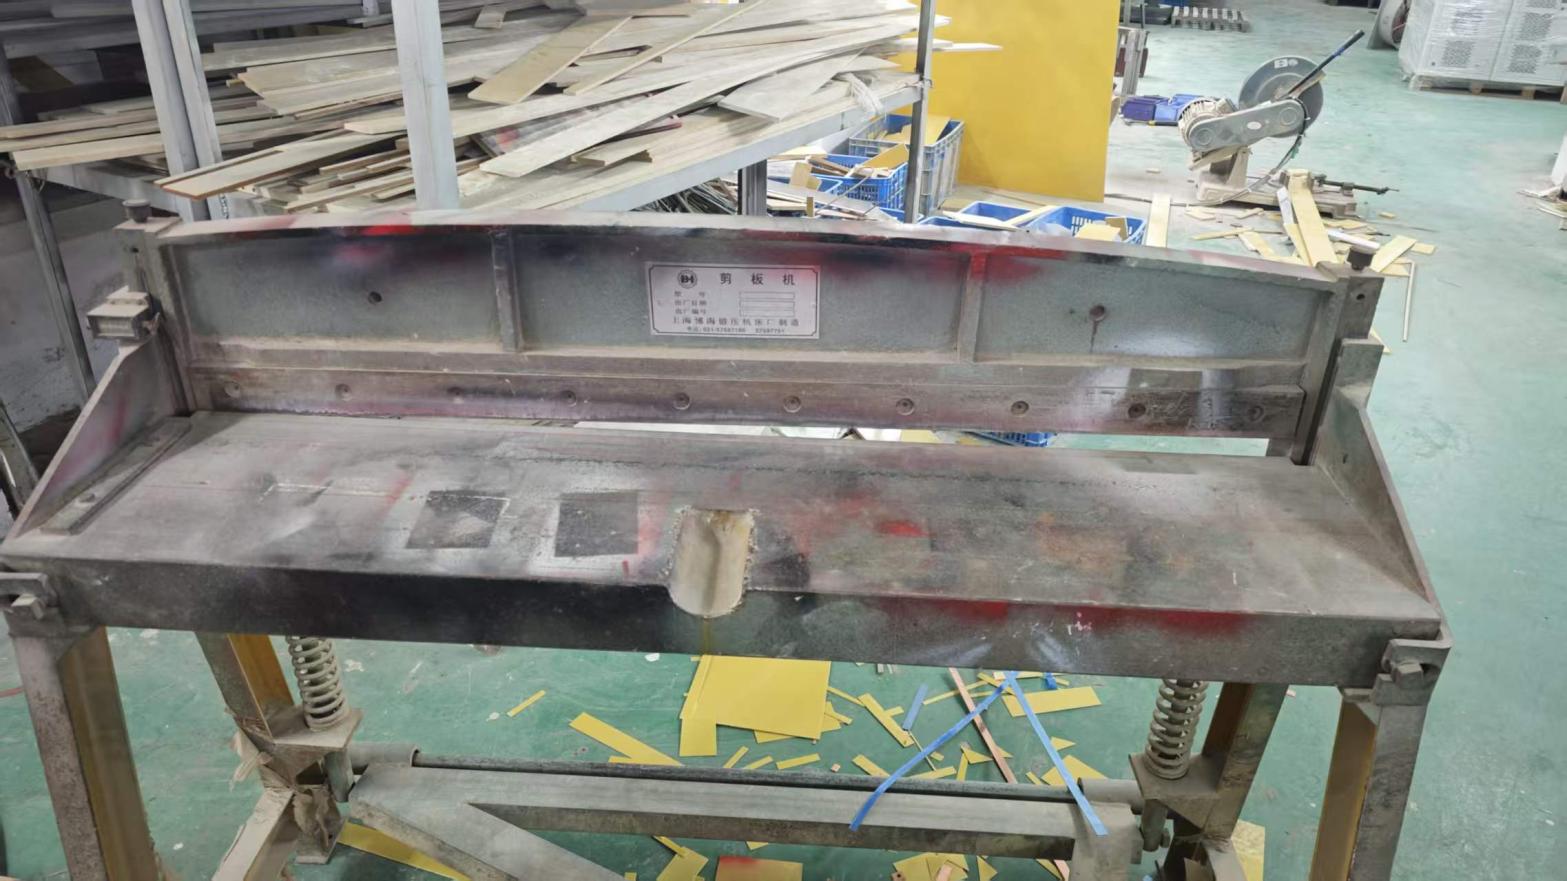
Unlike commercial trading companies or assemblers reliant on third-party fabricators, Guangdong Fenvix Technology Co., Ltd. maintains full vertical control over mechanical and electrical manufacturing. Inside our modern 3,000m² factory floor, precision CNC machines craft robust cabinet enclosures and silver-plated copper busbars to withstand the rigors of industrial water treatment environments.
Our dedicated engineering department conducts 100% incoming raw component screening, multi-layer conformal coating against corrosion, high-voltage dielectric insulation verification, and full-load burn-in testing on specialized resistive and reactive load banks prior to shipment.



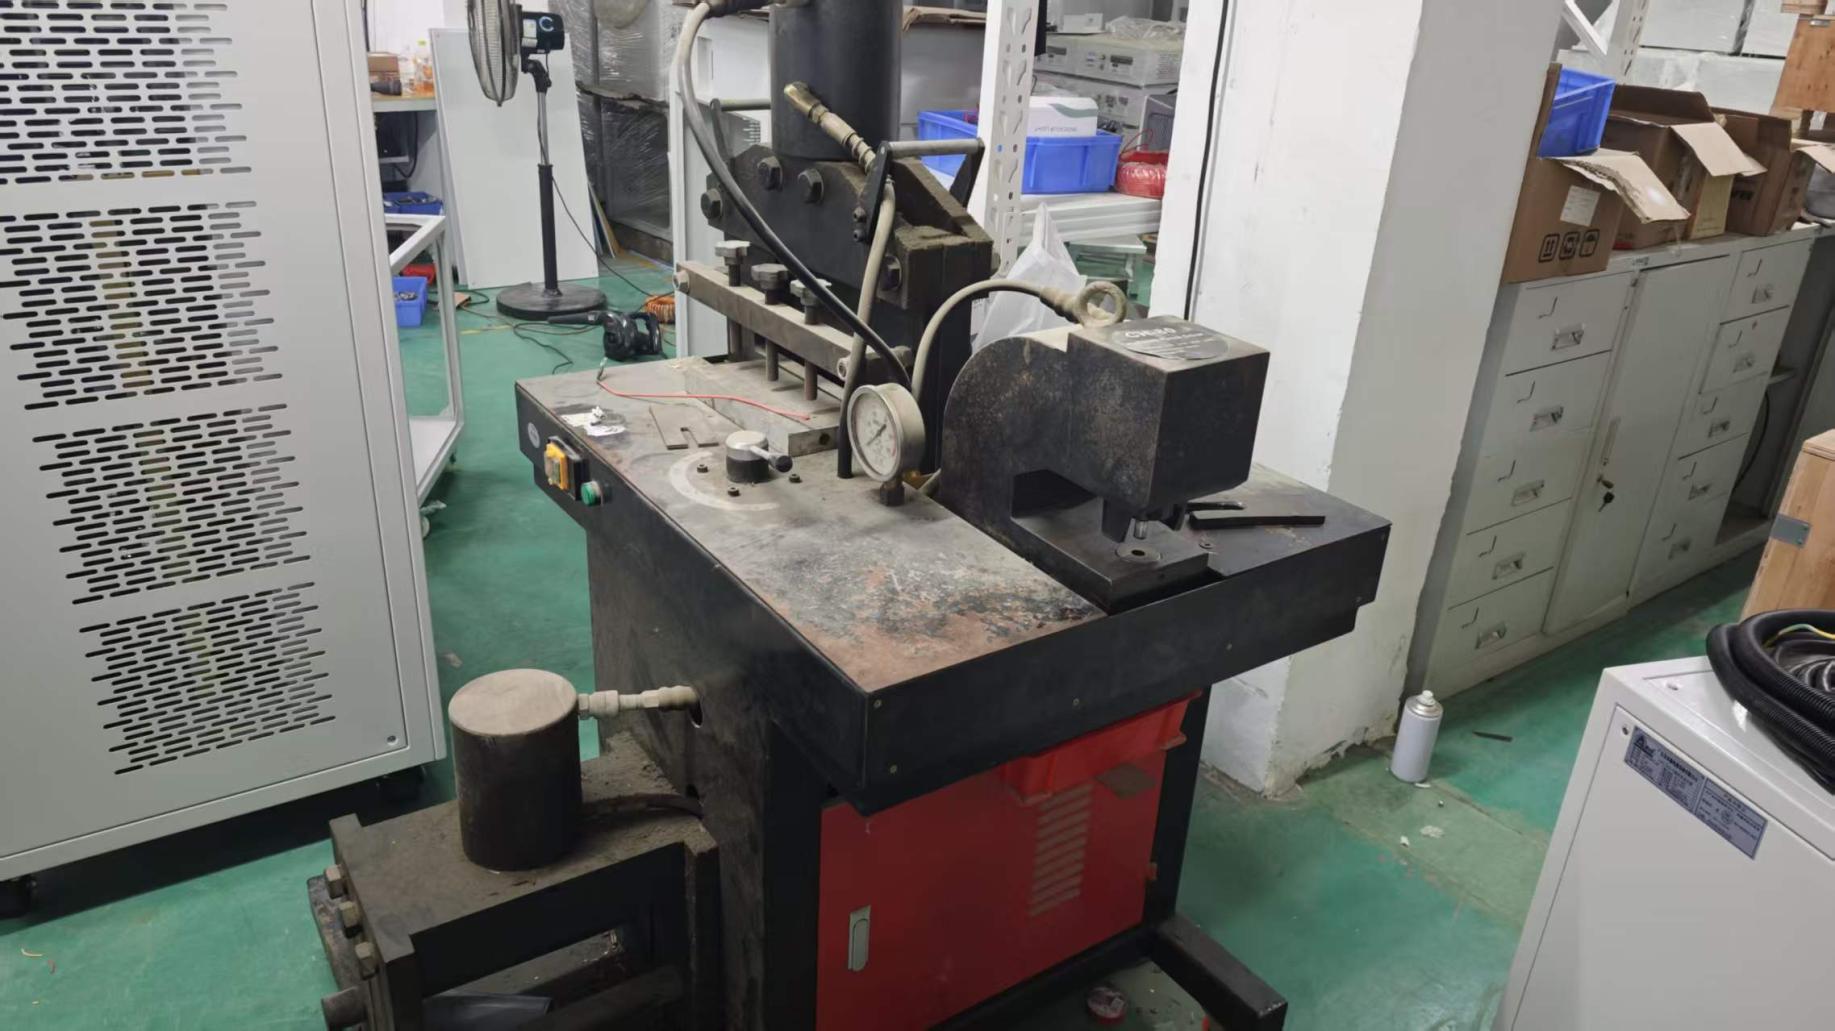

Trusted across global water utilities, multinational manufacturing plants, and heavy industrial facilities.
Certified Quality System
LVD & EMC Directives
Audited Factory Facility
DDP, CIF, FOB Terms
Engineer-to-Engineer
Bespoke Systems Sizing

Consult with our electrochemical engineering team for precise descaling load matching and fast quoting.
[email protected]