Industrial Electrochemical DC Rectifiers & Power Units
Engineered for continuous 24/7 duty cycles under corrosive industrial environments, equipped with RS485/Modbus telemetry, ripple suppression below 2%, and full EU Low Voltage & EMC directive conformity.

75kW 12V/15V 5000A–6000A Water-Cooled DC Rectifier
- Rated Output: 12V–15V / 5000A–6000A
- Cooling Topology: Direct Deionized Water
- Control Architecture: Dual CV / CC Digital Switch
- Protection: IP54 Sealed Cabinet, Over-Temp

48V 625A 30kW Polarity-Reversing Descaling Supply
- Operating Range: 0–48V DC / 0–625A
- Reversal Interval: 1s to 999m Programmable
- Automation: RS485 Modbus RTU / 4-20mA
- Primary Field: Electrocoagulation / Descaling

8000A 12V Heavy-Duty Water-Cooled Electrolysis Rectifier
- Output Rating: 12V Continuous / 8000A
- Efficiency Factor: ≥ 91.5% at Full Load
- Harmonic Distort.: THDi < 5% with Active Filter
- Typical Process: Metal Scavenging & Electrowinning

300kW 20V 15,000A High-Current Multi-Module Rack
- System Power: 300kW Modular N+1 Redundant
- DC Output: 0–20V / Up to 15000A
- Mains Input: 380V/400V/415V 50Hz 3-Phase
- Application: Municipal & Chemical Digestion

12V 150A High-Frequency Compact Electrochemical Unit
- DC Range: 0–12V / 0–150A Regulated
- Cooling System: Forced Low-Noise Air Flow
- Current Ripple: ≤ 1% RMS Full Spectrum
- Suitability: Pilot Water Skids & Lab Cells

48kW 12V 4000A Constant Current Plating & Clarification
- DC Output: 12V Constant Voltage / 4000A CC
- Switching Frequency: 20kHz IGBT Inverter Core
- Interface Protocol: Isolated 0–10V / PLC Terminals
- Target Sector: Automotive E-Coat Wastewater

20kW 400V–800V 50A Advanced Oxidation DC Source
- Voltage Window: 400V to 800V Continuous Trim
- Peak Current: 50A with Microsecond Fast Step
- Topology: High-Voltage Resonant Bridge
- Process Match: BDD Electrode Advanced Oxidation
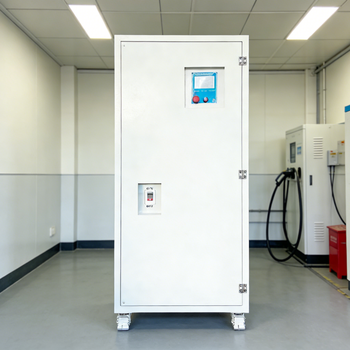
160kW 64V 2500A Industrial Electrodialysis Generator
- Power Configuration: 160kW Cabinet / 64V / 2500A
- Current Stability: ± 0.5% Load Regulation
- Control Response: < 5ms Dynamic Load Transition
- Primary Utility: Membrane Desalination & ZLD
High-Current Electrochemical Power Supplies in Industrial Effluent Neutralization
A rigorous examination of switch-mode power topologies, ionic boundary polarization, and current ripple constraints within modern European wastewater remediation infrastructures.
Modern industrial wastewater remediation has transitioned aggressively from conventional chemical flocculation and passive settling ponds toward targeted electrochemical transformations. Within the industrialized corridor of Western Slovakia—anchored prominently by the city of Nitra—this transition is driven by stringent implementation of the European Union Water Framework Directive (2000/60/EC) and the Industrial Emissions Directive (IED 2010/75/EU). These regulatory frameworks impose demanding ceilings on Chemical Oxygen Demand (COD), persistent organic contaminants, fluorides, and heavy metal concentrations discharging into municipal collectors and natural tributaries such as the Nitra River catchment basin.
The electrochemical degradation of refractory compounds fundamentally relies on the precise injection of electrical energy into electrolytic reactor vessels. Technologies including Electrocoagulation (EC), Electro-Fenton oxidation, Electrodialysis Reversal (EDR), and Boron-Doped Diamond (BDD) anodic electro-oxidation require power supplies capable of delivering stable, ripple-controlled direct current across fluctuating ionic resistances. Guangdong Fenvix Technology Co., Ltd., leveraging over 13 years of specialized power conversion manufacturing, provides Nitra's industrial skids and municipal environmental engineers with ruggedized switch-mode DC power supply systems designed specifically to conquer challenging solution conductivity, fluctuating pH gradients, and severe cathode passivation.
Electrochemical Dynamics: Why Precision DC Regulation Governs Reaction Kinetics
In electrochemical reactor chambers, the rate of pollutant destabilization is governed directly by Faraday's Law of Electrolysis, where the stoichiometric liberation of coagulant ions (such as Fe2+, Fe3+, or Al3+) is proportional to the total charge passed ($Q = I \times t$). When utilizing legacy silicon-controlled rectifiers (SCR/Thyristor systems), high output ripple frequencies (100Hz to 300Hz harmonics) generate instantaneous peak currents that lead to unwanted side reactions: excessive water hydrolysis into hydrogen and oxygen gas. This parasitically inflates kilowatt-hour consumption, accelerates destructive anode passivation, and escalates chemical sludge volumes.
Guangdong Fenvix utilizes high-frequency Insulated Gate Bipolar Transistor (IGBT) pulse-width modulation (PWM) topologies switching between 18kHz and 30kHz. By converting the 400V 50Hz three-phase European electrical mains into a micro-filtered DC rail, our power supplies preserve a smooth current profile with RMS ripple strictly beneath 2%. For operators in Nitra, this translates to predictable sacrificial anode dissolution, maximized hydroxyl radical ($\cdot\text{OH}$) production rates during electro-oxidation, and significant reductions in annual energy expenditure per cubic meter of treated industrial effluent.
Tailored Deployment Across Nitra's Manufacturing Landscape
Specific operational profiles designed for automotive assembly clusters, Tier-1 surface coating lines, electronic component manufacturing, and local agro-industrial facilities.
Automotive Surface Finishing & E-Coat Effluent
Nitra's automotive footprint—dominated by massive vehicle assembly plants and tier-level stamping and coating facilities—generates vast volumes of rinse water burdened with phosphates, emulsified oils, electrophoretic resins, and dissolved zinc/nickel. Fenvix constant-current rectifiers power continuous electrocoagulation cells, destabilizing high-molecular polymers and dropping heavy metals beneath Slovak municipal sewer intake standards.
Automotive Ecosystem • Nitra NorthElectroplating Drag-Out Heavy Metal Recovery
Commercial hardware, mechanical component plating, and decorative metal shops in the Nitra and Trnava regions require closed-loop metal recovery. Our high-amperage, low-voltage water-cooled rectifiers (0–15V, up to 10,000A) energize electrowinning cells, selectively precipitating copper, chromium, and cadmium from spent bath rinse rinses, transforming hazardous sludge liabilities into recyclable metallic cathodes.
Zero Toxic Sludge StrategyRefractory COD Destruction via Advanced Oxidation (AOP)
Chemical synthesizers and packaging manufacturers in Western Slovakia face non-biodegradable, recalcitrant chemical oxygen demand. Utilizing Fenvix high-voltage DC supplies (up to 800V DC), automated systems energize Mixed Metal Oxide (MMO) or Boron-Doped Diamond (BDD) anode stacks to generate localized hydroxyl radicals, splitting complex aromatic rings and chlorinated surfactants directly at the boundary layer.
High-Voltage Electrochemical AOPCooling Tower Blowdown Descaling & Disinfection
The heavy production facilities in Nitra circulate millions of liters of process cooling water. Calcium carbonate ($\text{CaCO}_3$) and silica precipitation severely throttle heat exchangers. Fenvix automated polarity-reversing power supplies operate electrolytic precipitation chambers, removing scale hardness while concurrently synthesizing in-situ hypochlorous acid ($\text{HClO}$) to eliminate legionella risk without chemical additives.
Automated Polarity ReversalZero Liquid Discharge (ZLD) Electrodialysis Reversal
With industrial water extraction charges increasing under Slovak environmental ministries, facilities are deploying Electrodialysis Reversal (EDR) to drive brine concentration to saturation limits. Our programmable switch-mode rectifiers deliver sub-millisecond polarity switching under high voltage loads, neutralizing membrane fouling and maintaining continuous ion migration without system shutdown.
ZLD Concentration TrainsTechnological Trajectories Shaping Nitra's Water Treatment Infrastructure
The industrial wastewater ecosystem across Central and Eastern Europe is rapidly consolidating around three technological imperatives: decarbonization of operating energy, mitigation of hazardous chemical handling, and integration of Industrial Internet of Things (IIoT) telemetry. In Slovakia, where energy intensive manufacturing represents a high fraction of national GDP, wastewater plants are no longer viewed merely as cost sinks; they are evaluated as critical nodes of resource recovery.
1. Decarbonization via High-Efficiency Power Stages: Traditional line-frequency SCR rectifiers incur total system efficiencies lingering between 75% and 82%, generating massive thermodynamic losses that mandate separate air-conditioning systems. In contrast, Fenvix IGBT platforms regularly achieve ≥91.5% to 94% overall electrical conversion efficiency. For a facility running a 150kW continuous electrocoagulation cell 8,000 hours per annum, the delta in thermodynamic efficiency yields substantial electrical savings, directly aligning with corporate Scope 2 carbon emissions targets under EU ESG reporting mandates.
2. In-Situ Disinfection Eliminating Biocide Transport: Strict European ADR transport laws for hazardous chemicals have caused chlorine and biocide logistical costs to surge. High-current DC electrolysis rectifiers empower on-site, on-demand chlor-alkali and mixed-oxidant generation directly from the native chloride content of wastewater, completely eliminating tanker deliveries of toxic sodium hypochlorite to production plants in Nitra.
3. Advanced Fieldbus Automation: Disconnected, analog potentiometer control has become obsolete in modern European manufacturing execution systems (MES). Fenvix integrates isolated RS485 (Modbus-RTU), Profibus, Profinet, and analog 0–10V / 4–20mA interfaces directly onto the motherboard. This enables environmental supervisory systems in Nitra control rooms to autonomously dynamically throttle rectifier output based on real-time upstream turbidity, conductivity, and dissolved oxygen probes.
Comparative Engineering Matrix: Legacy SCR vs. Fenvix High-Frequency IGBT
A side-by-side performance audit illustrating conversion topology, electrode life impact, and harmonic distortion profiles on the Slovak 400V 50Hz grid.
| Performance Characteristic | Legacy SCR / Thyristor Rectifier | Fenvix High-Frequency IGBT System | Impact on Nitra Industrial Operator |
|---|---|---|---|
| Conversion Efficiency | 72% – 82% (High transformer losses) | 90% – 94% (High-frequency conversion) | Saves 12–18% electrical energy per m³ of treated effluent. |
| DC Current Ripple (RMS) | 5% to >15% at phase-angle throttle | ≤ 2.0% across full dynamic range | Prevents parasitic water electrolysis; extends MMO/Fe anode life by 25%. |
| Cabinet Footprint & Mass | Heavy, oil-immersed or bulky air (1.8m³+) | Modular 19" rack or compact skid (0.4m³) | Easily integrated inside containerized wastewater skids with constrained space. |
| Grid Power Factor ($\cos \phi$) | 0.65 – 0.80 (Degrades at partial loads) | ≥ 0.94 across active regulation span | Eliminates reactive power surcharges from Slovak distribution grids (ZSD). |
| Polarity Inversion Mechanism | Bulky mechanical contactors (Wear prone) | Solid-state H-bridge electronic reversal | Sub-second polarity flip; continuous maintenance-free scale descaling. |
| Harmonics (THDi) | High low-order harmonics (5th, 7th, 11th) | Suppressed; compliant with EN 61000-3-4 | No electrical interference with sensitive PLC or automotive robotics. |
Guangdong Fenvix Technology Co., Ltd.
Founded in 2013 in Guangzhou, Guangdong, China, Fenvix has operated for over 13 years as an elite direct manufacturer of extreme-duty industrial DC power systems, heavy-current electrolysis rectifiers, high-voltage programmable sources, and 400Hz static aviation converters. Unlike export trading intermediaries, every critical component is engineered, machined, assembled, and burn-in tested inside our own 3,000m² production complex.
- In-House Metal Fabrication & Pure Copper Busbars: Precision plate shearing, CNC punching, milling, and specialized silver/nickel-plated busbar bending to withstand severe corrosive wastewater atmospheres.
- Zero Minimum Order Quantity (MOQ = 1 Unit): Direct engineering customization for pilot environmental engineering prototypes through multi-megawatt wastewater plant extensions.
- Exhaustive Quality Assurance Protocols: Incoming raw material verification, circuit board conformal coating against humid acid-gas ingress, and 100% full-load thermal chamber burn-in prior to dispatch.
- Verified Global Track Record: Independent on-site inspection verified by TÜV Rheinland, operating under certified ISO 9001 quality systems with broad CE, LVD, and EMC conformity for EU integration.
 CE European Conformity
 EN 61010 / LVD Directive
 Industrial EMC Tested
 TÜV On-Site Verified
Frequently Asked Questions by Industrial Engineers in Nitra
Comprehensive operational, electrical, and commercial guidelines for plant managers importing direct factory systems into the Slovak Republic.
How do Fenvix DC power supplies integrate with the standard Slovak 400V 50Hz industrial grid?
Should our Nitra wastewater facility specify water-cooled or forced-air cooling?
Forced Air Cooling: Recommended for amperage ratings up to 1000A located in well-ventilated electrical mezzanine rooms isolated from reactor vapors. All internal printed circuit boards feature multi-layer polyurethane conformal coatings to safeguard against sulfur and acid traces.
Closed-Loop Water Cooling: Mandatory for installations situated directly beside open aeration tanks, electrocoagulation sumps, or electroplating lines where acidic or caustic aerosols are present. Water-cooled units (such as our 5000A–15000A systems) reside in totally sealed IP54/IP55 cabinets, transferring internal heat to titanium or 316L stainless steel plate heat exchangers using chilled plant water or deionized coolant loops. This completely isolates sensitive IGBT power blocks from ambient airborne corrosives.
How does the automated polarity-reversing function prevent electrode scaling?
What documentation and CE certificates accompany shipments cleared through Slovak customs?
Can Fenvix power supplies be coupled with Siemens or Allen-Bradley PLCs on site?
What warranty, spare parts, and after-sales service models are provided for Central European buyers?
Deploy High-Performance Electrochemical Power in Nitra
Consult directly with Fenvix power design engineers. Send us your electrolyte parameters, required voltage/amperage envelope, duty cycle, and control specifications to receive an engineered technical quotation within 24 hours.