Featured Industrial & Electronic Aging Test Power Supplies
Engineered for continuous 24/7 accelerated life cycle burn-in testing, component validation, and high-precision laboratory stress test routines. Each unit is custom-calibrated to European grid standards (380V/400V 50Hz) and CE compliance.

800V 50A 20kW EV Charging & Battery Aging Test DC Supply
- Output Range: 0–800V / 0–50A / 20kW
- Control Modes: CC / CV / CP Programmable
- Interface: RS485 / Modbus-RTU / LAN
- Compliance: CE, LVD, EMC, RoHS
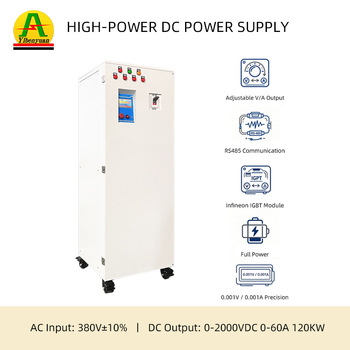
90kW–120kW 2000V High-Voltage Programmable Test Source
- Output Range: 0–2000V / 0–60A / 120kW
- Voltage Ripple: ≤ 0.2% RMS Full Scale
- Protection: OVP, OCP, OTP, Short Circuit
- Duty Cycle: 100% 24/7 Continuous
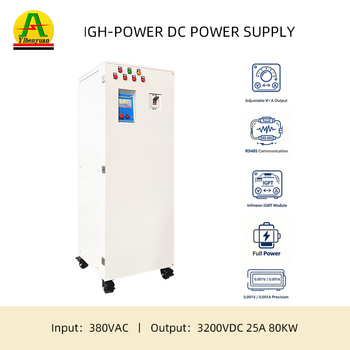
80kW 3200V Precision Component & Capacitor Aging Supply
- Output Range: 1000V–3200V / 16A–25A
- Technology: Resonant IGBT Inverter
- Transient Rise: < 15ms Programmable Ramp
- Application: Power Dielectrics & HV Relays
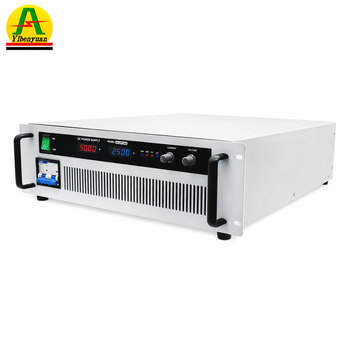
1.5kW–5kW Programmable Bench DC Burn-In Power Supply
- Output: Multi-Range 0–300V / 0–100A
- Efficiency: ≥ 90% at Rated Load
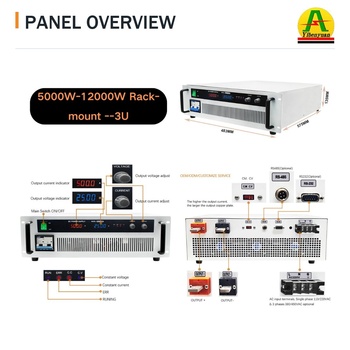
- Form Factor: 19" Standard Rack 2U/3U
- Display: High-Resolution Digital LED/LCD
6kW 0–60V 100A Digital Display Laboratory DC Source
- Output Range: 0–60V / 0–100A / 6000W
- Setting Accuracy: ± 0.1% of Set Value
- Sensing: Remote Voltage Drop Sensing
- Cooling: Smart Fan Speed Temperature Control

75kW 12V/15V 5000A/6000A Water-Cooled DC Rectifier
- Current Rating: 5000A / 6000A High Current
- Cooling Mode: Deionized Closed-Loop Liquid
- Enclosure: IP54 Sealed Anti-Corrosion
- Use Case: Electrolysis & High-Current Stress
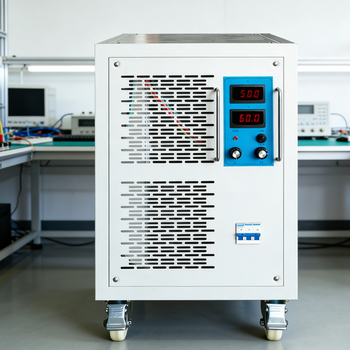
16kW 0–4000V Adjustable HV Insulation Aging Power Supply
- Output: 0–4000V / 1A–4A Continuous
- Isolation: > 100MΩ @ 5000V DC
- Protection: Arc Detection & Spark Quenching
- Automation: Analog 0-10V & Digital RS485

48V 625A 30kW Heavy-Duty Endurance Burn-In DC Source
- Output Power: 30kW Continuous Stable Output
- Features: Programmable Dynamic Load Cycling
- Efficiency: 92% High Efficiency IGBT Topology
- Application: Inverter & Motor Driver Aging
Empowering Poznań's High-Reliability Electronics & E-Mobility Manufacturing Hub
As the capital of the Wielkopolska (Greater Poland) region, Poznań is at the epicenter of Central Europe's automotive supply chain, power electronics innovation, and advanced contract electronics manufacturing (EMS). Discover how high-efficiency DC aging test power supplies eliminate infant mortality in mission-critical hardware.
The Critical Role of Accelerated Life Testing (ALT) in Modern European Supply Chains
Modern industrial equipment operating in Poland's demanding manufacturing environment cannot afford unexpected downtime. High-power DC-DC converters, electric vehicle (EV) onboard chargers, automotive battery management systems (BMS), solar inverters, and industrial motor drives undergo severe operational stresses. Accelerated Burn-in and Aging testing subject these electronic assemblies to elevated thermal, electrical, and cyclic stress profiles, deliberately precipitating early component failures before finished systems reach OEM assembly floors in Poznań, Swarzędz, or Tarnowo Podgórne.
Guangdong Fenvix Technology Co., Ltd. delivers high-frequency IGBT-based programmable DC aging test power supplies engineered specifically for long-duration, high-duty testing cycles. Our solutions provide Poznań manufacturers with microsecond-level dynamic transient response, ultra-low ripple (<0.2%), and advanced programmable step-voltage sequencing needed to execute compliant test protocols under EN 60068, ISO 16750, and IEC 61851 standards.
By eliminating middleman margins and trading companies, Fenvix establishes direct engineering collaboration between our Guangdong precision fabrication facility and Polish factory automation managers, ensuring customized physical dimensions, custom communication protocols, and tailor-made thermal configurations.
Engineered for Poznań's Core Industrial Ecosystem
From Tier-1 automotive manufacturing plants along the A2 motorway to high-density cleanroom semiconductor assembly facilities in the Wielkopolska region, our aging test power supplies provide the foundational DC power infrastructure.
Automotive & EV Component Burn-in
Poznań and surrounding hubs host extensive automotive stamping, wiring harness, and EV drivetrain component production. Our programmable DC systems simulate real-world battery discharge profiles, cold-cranking pulses, and overvoltage surges.
- DC-DC converters & On-Board Chargers (OBC)
- 48V mild-hybrid and 800V silicon-carbide (SiC) traction inverters
- Automotive lighting, ECUs, and busbar continuous load testing
- ISO 16750-2 electrical disturbance test sequences
Contract Electronics Manufacturing (EMS)
Wielkopolska is home to premier European contract manufacturers assembling complex industrial controllers, IoT gateways, and white-goods control boards requiring long-duration elevated-temperature burn-in rooms.
- Multi-channel burn-in racks with centralized PLC supervision
- Automated fault detection with individual channel latching
- Ultra-low EMI emissions compliant with EN 61000 industrial limits
- Continuous logging of current draw drifts to isolate weak solder joints
Renewable Inverter & BESS Quality Assurance
Poland's massive expansion in distributed solar photovoltaics and industrial battery energy storage systems (BESS) drives continuous testing of solar string inverters, DC combiners, and high-voltage DC contactors.
- Simulation of high-voltage photovoltaic strings up to 1500V DC
- High-capacity capacitor charging and dielectric stress validation
- Continuous current testing of high-power DC disconnect switches
- Thermal-runaway barrier testing for battery modules
Industrial Automation & Robotics Testing
Poznań's high-tech machinery producers require rugged DC sources capable of absorbing regenerative back-EMF from multi-axis servo drives and inductive robotic arm actuators without tripping overvoltage protections.
- Bi-directional regenerative testing eliminating factory heat buildup
- Fast dynamic load regulation during 100% step-load changes
- Modbus-TCP and Profinet compatible communication gateways
- Modular 19" rack-mount configurations for automated test benches (ATE)
Aviation & Specialized Defense Ground Support
Adjacent to Poznań-Ławica Airport and military maintenance facilities in Western Poland, aviation electronics and radar assemblies demand 28.5V DC and 400Hz frequency conversion aging systems.
- Ultra-clean DC outputs matching MIL-STD-704 and STANAG criteria
- High-surge capacity for simulated avionics starter engagement
- Static solid-state converters eliminating rotary maintenance
- Ruggedized mobile castor or stationary hangar cabinet designs
Electrochemistry & Surface Treatment Testing
In addition to electronic burn-in, surface treatment facilities throughout Greater Poland require continuous current rectifiers for hard anodizing, electroplating, and wastewater electrolytic processing.
- Outputs up to 15,000A DC with full CC/CV automatic crossover
- Sealed water-cooled heat exchangers resistant to acidic atmospheres
- Programmable periodic reverse polarity timers for descaling
- Exceptional power factor (>0.95) mitigating industrial reactive charges
Technical Architecture: High-Frequency IGBT Switching vs Legacy SCR Systems
Discover why tier-1 test laboratories and manufacturing facilities in Poznań are phasing out bulky legacy thyristor rectifiers in favor of high-frequency digital PWM resonant switching topologies.
Optimizing Operational Costs & Thermal Density in Aging Facilities
Burn-in rooms are notorious for generating extreme heat loads. When dozens of electronic test power supplies run concurrently for 72 to 168 hours, inefficient power conversion compounds HVAC electricity costs. Legacy silicon-controlled rectifiers (SCR) generally operate at 70%–78% conversion efficiency with sluggish transient response times exceeding 100 milliseconds.
Fenvix aging test power supplies deploy advanced insulated-gate bipolar transistor (IGBT) full-bridge inverter technology switching at 20kHz to 50kHz. This design achieves active power factor correction (PFC > 0.95), typical system efficiencies between 90% and 94%, and dynamic transient recovery times under 2 milliseconds. The microsecond responsiveness prevents damaging voltage overshoots during sudden DUT (Device Under Test) open-circuit or short-circuit failures.
Furthermore, our integrated closed-loop deionized liquid cooling configurations allow high-power test cabinets (up to 300kW) to operate in completely sealed IP54 enclosures, shielding sensitive control boards from Poznań plant ambient dust, metallic particles, and humidity.

Comparative Selection Matrix for Electronic Aging Power Configurations
| Test Application | Voltage & Current Matrix | Key Engineering Requirements | Cooling Options | Recommended Model Class |
|---|---|---|---|---|
| EV Battery Module & BMS Burn-in | 0–120V / Up to 1,000A DC | Ultra-low ripple <0.1%, fast rise time, remote voltage sensing | Forced Air / Liquid | Fenvix BMS-Pro Series |
| Automotive On-Board Charger (OBC) Stress | 400V–800V / 20A–100A DC | Programmable dynamic ramp, over-voltage latch, Modbus-TCP | Intelligent Variable Fan | Fenvix HV-EV 800 Series |
| High-Power Inverters & SiC Module Aging | 0–1500V / 50A–200A DC | High peak isolation, arc detection, automated cyclic profiles | Dual Closed-Loop Water | Fenvix SiC-Master HV |
| High-Current Connectors & Busbar Endurance | 0–15V / 1,000A–15,000A DC | True continuous constant current (CC), continuous copper thermal sink | Water-Cooled Copper Heat Sink | Fenvix HC-Max Rectifiers |
| Capacitor & Insulation Breakdown Life Test | 0–3200V to 100kV DC | Constant current capacitor charging, rapid discharge quench circuit | Forced Air / Oil Insulation | Fenvix CapCharge 100kV |
| PCB Assembly / EMS Multi-DUT Benchtop | 0–60V / 0–100A (1.5kW–6kW) | 19-inch rack compatible, SCPI commands, high precision LCD | Quiet Low-Acoustic Air | Fenvix RackMate 2U/3U |
Key Sourcing Trends Influencing Poznań Test & Quality Engineers
Procurement decisions across Poland and the wider European Union are governed by tightening efficiency regulations, Industry 4.0 data traceability, and supply chain de-risking.
Grid Decarbonization & Eco-Design
Under the EU Green Deal and European Eco-Design Directives, test facilities in Poznań face stringent energy quotas. Fenvix integrates high-efficiency switching topologies and optional energy regeneration modules that feed braking and discharging energy back into the internal plant 400V grid, reducing net electrical draw by up to 88%.
Digital Traceability & SCADA Integration
Modern quality assurance mandates end-to-end data logging for every serialized unit undergoing burn-in. Fenvix units offer native RS485 (Modbus-RTU), Ethernet (Modbus-TCP), and analog control interfaces, enabling seamless plug-and-play communication with local LabVIEW, Python, and PLC automated test execution architectures.
Rapid Factory-Direct Customization
Catalog distributors often force Polish engineers into standard off-the-shelf voltage bands that do not match specialized DUT parameters. Fenvix engineers customize internal busbars, cabinet enclosures, front-panel controls, and firmware timing routines directly at our factory, shipping pre-calibrated prototypes with zero minimum order quantities (No MOQ).
Inside the Fenvix Production & Quality Verification Facility
Unlike sourcing brokers or re-branders, Guangdong Fenvix Technology Co., Ltd. controls the complete manufacturing chain in our 3,000 m² plant, from raw copper busbar fabrication to high-power load testing.
Full In-House Sheet Metal & CNC Machining Capability
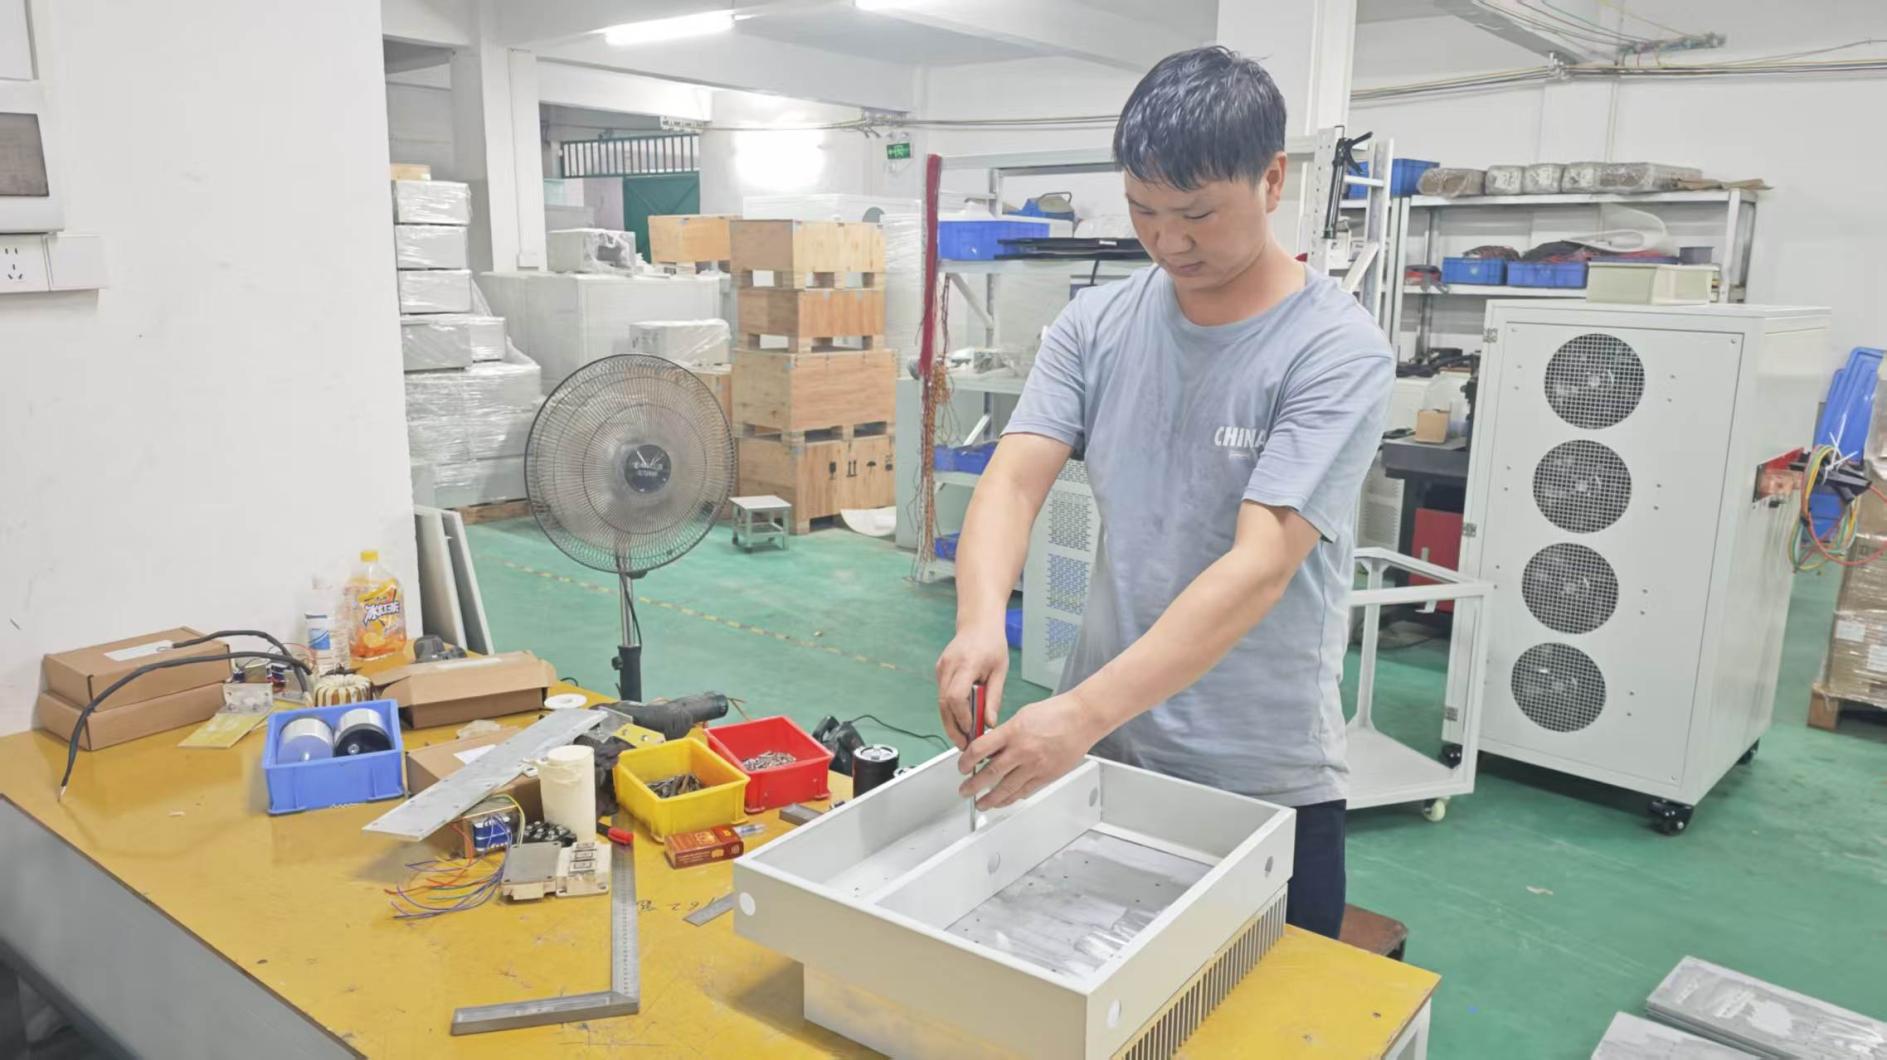
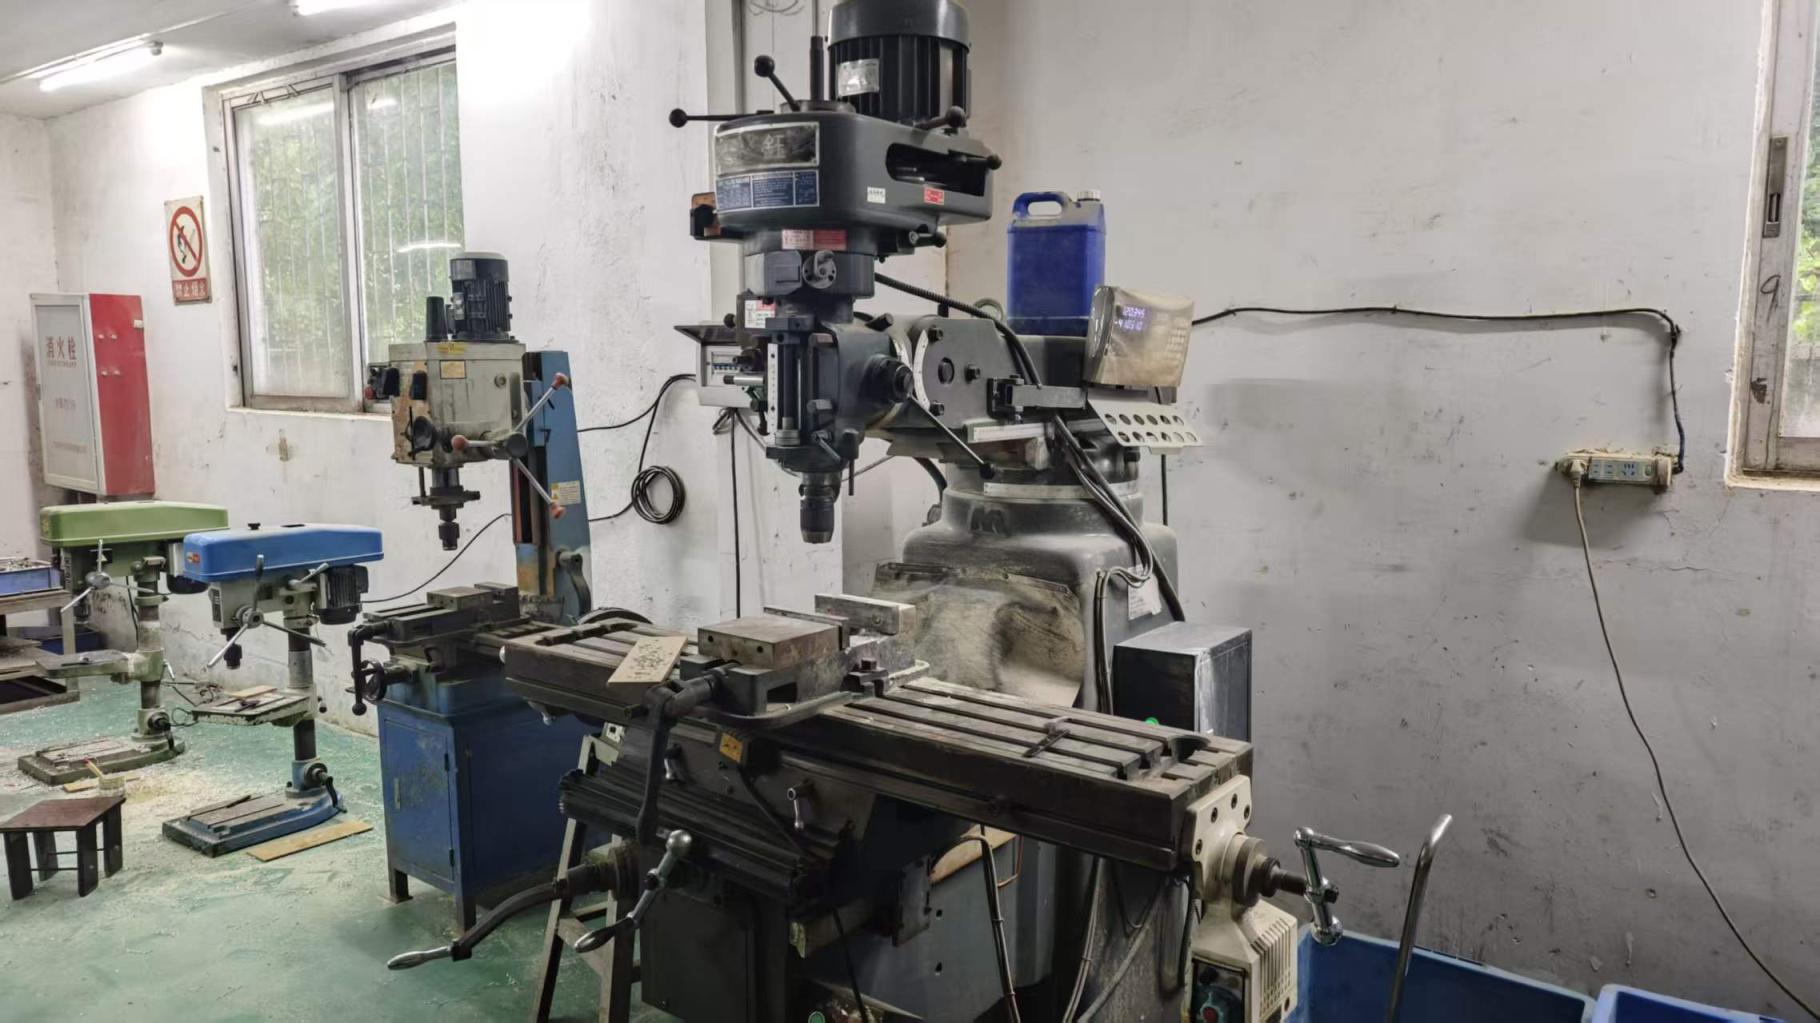
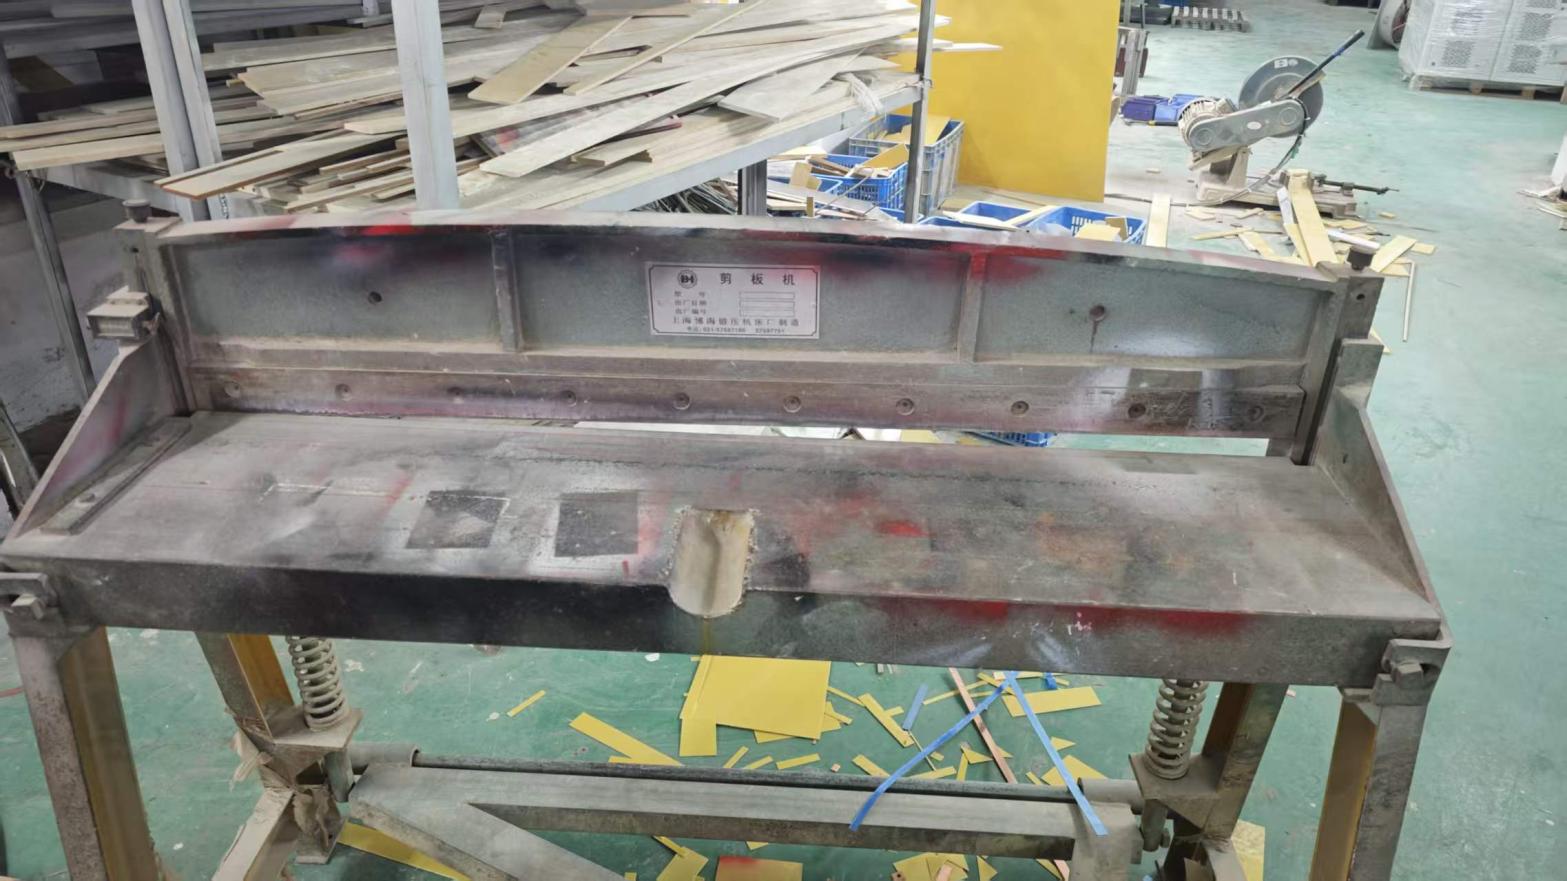
High-current, high-voltage power supplies require uncompromising structural integrity and thermal dissipation channels. At Fenvix, our facility in Guangdong is equipped with in-house plate shearing machines, punching presses, precision milling equipment, and automatic drilling and tapping machinery. We fabricate our own heavy-gauge cold-rolled steel enclosures and CNC-machine electrolytic copper busbars to exact tolerances.
By keeping metal fabrication under one roof, we eliminate third-party subcontractor delays, maintain stringent dimensional control, and can quickly adapt cabinet form factors to fit our Poznań clients' tight cleanroom footprints or 19-inch equipment racks.
Every single power unit undergoes a rigorous multi-stage quality protocol: incoming raw component verification, high-pot insulation breakdown testing, full-load burn-in under real resistive and inductive loads, and oscilloscope waveform analysis for ripple and transient stability before seaworthy or airworthy wooden crating.
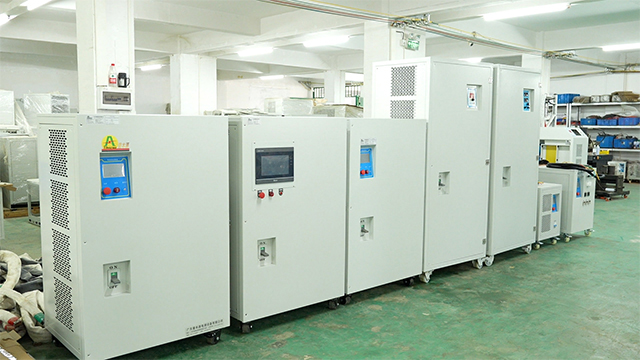
Precision Workshop Stages: From Component Fabrication to Load Test



Certified Rigor & International Compliance for Polish Importers
Fenvix operations conform to the highest global standards, ensuring seamless customs clearance, rapid CE integration, and trouble-free technical audits across the European Union.
ISO 9001:2015 Certified
Standardized quality management systems overseeing incoming materials, sub-assembly inspections, and pre-shipment documentation.
CE, LVD & EMC Compliance
Compliant with Low Voltage Directive (2014/35/EU) and Electromagnetic Compatibility Directive (2014/30/EU) for safe EU grid integration.
TÜV Rheinland Audited
Our production facilities, testing instruments, and manufacturing capacities have been independently audited on-site by TÜV Rheinland.
End-to-End DDP Logistics
Reliable freight channels serving Poland via Rail Freight (Małaszewicze terminal), Air Express, or Ocean shipping to Gdynia/Gdańsk.

Frequently Asked Questions by Poznań Sourcing & Test Engineering Teams
Get practical, transparent answers regarding grid compatibility, delivery timelines to Wielkopolska, custom firmware adaptations, and technical warranty support.
Are Fenvix power supplies directly compatible with Poland's 400V 50Hz three-phase grid?
What are the primary logistics corridors and typical delivery lead times to Poznań?
- Air Express / Air Freight (7–10 Business Days): Best suited for urgent benchtop units, control PCBs, or critical prototype validation models, landing at Poznań-Ławica (POZ) or Warsaw Chopin (WAW).
- China-Europe Railway Express (16–22 Days): High-capacity, cost-effective container rail transit arriving directly at the Małaszewicze dry port terminal in Poland, then trucked straight to your facility in Poznań.
- Maritime Ocean Freight (28–35 Days): Cost-optimized for heavy industrial rectifiers, 120kW+ cabinets, or multi-rack containerized testing systems via Gdynia or Gdańsk container ports.
Do you accommodate custom DC voltage, current ratings, and specialized control firmware?
When should a Poznań facility select water-cooled over air-cooled power supplies?
What CE documentation and test certificates are supplied with each export shipment?
How does Fenvix deliver post-sales technical support and warranty service in Poland?
Ready to Optimize Your Electronic Aging & Burn-In Infrastructure in Poznań?
Submit your voltage, current, duty cycle, and communication requirements today. Our experienced power electronics engineering team will deliver a comprehensive technical proposal, electrical schematics, and an official factory-direct quote within 24 hours.