Engineering-Grade Power Supplies for Ostrava Surface Finishers
Custom direct-drive switch mode converters, heavy-duty immersion electrolysis rectifiers, and high-frequency pulse modules engineered for demanding automotive, metallurgy, and heavy machinery plants.

12V/15V 5000A-6000A 75kW HF Plating Rectifier
- Output: 12V/15V, Up to 6000A
- Cooling: Deionized Water / Closed Loop
- Efficiency: ≥90% at Rated Load
- Control: CV/CC, RS485 Modbus

12V 150A High-Frequency Precision Bench Rectifier
- Output: 0–12V DC / 0–150A Continuous
- Ripple Factor: ≤1% RMS Ultra-Low Ripple
- Application: PCB Vias, Au/Ag Deposition
- Display: Digital 4-Digit Multi-Meter

12V 4000A 48kW Heavy Zinc/Nickel Electroplating Unit
- Input: 380V / 400V AC 3-Phase 50Hz
- Duty Cycle: 100% 24/7 Heavy Industrial
- Protection: Over-temp, Short, Phase loss
- Topology: Full-Bridge Soft-Switch IGBT

8000A 12V Water-Cooled Continuous Galvanizing Rectifier
- Output: 12V DC / 8000A Output Array
- Cooling: Liquid Cooled Sealed Enclosure
- Busbar: T2 Electrolytic Copper Interface
- Environment: Acid-Fog & Salt Mist Resilient

100A–3000A Step-Ramp Anodic Oxidation Rectifier
- Voltage: 12V, 24V, up to 100V Programmable
- Ramping: Multi-Step Current Density Slope
- Application: Alloy Extrusions & Hard Coat
- Integration: 0–10V / 4–20mA PLC Inputs

5000W Electrophoresis (E-Coat) Cataphoretic Power Supply
- Output: 0–300V DC Smooth Voltage Arc
- Protection: Instant Overcurrent Trip (Arcing)
- Application: Auto Sheet & Frame Priming
- Stability: Voltage Regulation <0.5%

48V 625A 30kW Auto-Polarity Reversing Descaling Supply
- Switching: IGBT H-Bridge Milli-sec Reverse
- Timer: 4-Segment Cyclic Forward/Reverse
- Application: Wastewater & Scale Electrolysis
- Enclosure: IP54 Corrosive Mist Sealed

300kW 20V 15,000A Heavy Metallurgy Electrolysis Rectifier
- Output: 20V DC / 15,000A Continuous DC
- Topology: Modular Parallel Current Sharing
- Cooling: Dual-Circuit Direct Liquid Thermal
- Field Service: Zero-Downtime Hot-Swappable Subracks
Strategic Electrochemistry Sourcing for Ostrava’s Heavy Industrial Base
A technological and supply chain roadmap bridging China’s premier power engineering manufacturing hub with Central Europe’s historic heart of metallurgy and automotive manufacturing.
The city of Ostrava, historically recognized as the steel backbone of the Czech Republic and Central Europe, has undergone an unprecedented transformation into an advanced engineering, automotive component fabrication, and modern metallurgical processing cluster. From heavy rail transport manufacturing and structural carbon-steel galvanizing to intricate zinc-nickel barrel plating for Tier-1 automotive supply networks (supplying assembly lines in nearby Nošovice and throughout the Žilina-Katowice industrial corridor), electroplating performance is directly dictated by DC power quality. In modern electrochemical deposition, the switch from obsolete, energy-intensive silicon-controlled rectifiers (SCR/thyristors) to high-frequency insulated-gate bipolar transistor (IGBT) switch-mode technology is no longer merely an upgrade; it is an economic and environmental imperative under escalating European energy pricing and strict corporate decarbonization standards.
Direct sourcing from specialized Chinese manufacturers like Guangdong Fenvix Technology Co., Ltd. provides Ostrava's galvanic operations, job-shop coaters, and equipment integrators with custom-engineered rectifiers that balance high-power efficiency, nanosecond-level pulse and reversing controls, and robust galvanic isolation against aggressive workshop chemicals. Because surface finishing quality—measured in layer uniformity, micro-crack densities, corrosion barrier hours (ASTM B117), and bath power efficiency—stems directly from instantaneous waveform control, understanding the synergies between Chinese power electronics manufacturing and Moravian-Silesian process lines is critical for regional production managers.
Automotive Zinc-Nickel & Hard Chrome Lines
Tier-1 automotive sub-suppliers positioned along Ostrava's key transit hubs require uniform thickness distribution on fasteners, brake calipers, and hydraulic piston rods. Low-ripple (<1% RMS) high-frequency rectifiers prevent the "dog-bone" over-deposition effect on sharp edges, saving precious nickel salt chemistry and meeting stringent OEM automotive salt-spray milestones exceeding 720 hours without red corrosion.
Continuous Heavy Strip Galvanizing & Pickling
Ostrava’s large-scale rolling mills, steel wire factories, and tube fabricators operate continuous strip and wire immersion lines requiring tens of thousands of continuous DC amperes. Fenvix water-cooled rectifiers operate 24/7 in non-stop automated dip baths, withstanding acidic fumes through completely sealed, NEMA 4X / IP54 liquid-chilled compartments that decouple sensitive electronics from the ambient plant air.
Precision Anodizing & Industrial Wastewater
From architectural aluminum profile hard-anodizing (Type III) that requires precise multi-phase current ramping to prevent burning, to electrolytic descaling and advanced electrochemical oxidation (EO) for industrial wastewater remediation, our automatic polarity-reversing DC power supplies eliminate electrode passivation and scale build-up without manual acid-cleaning shutdowns.
Local Technology Trends in Ostrava's Metal Treatment Sector
How automation, soaring energy prices, and EU environmental frameworks are shaping power conversion procurement in the Moravian-Silesian basin.
Procurement teams and galvanic plant supervisors in Ostrava and the wider Moravian-Silesian region are shifting criteria when selecting electrical conversion gear. First, the phase-out of legacy oil-immersed thyristor rectifiers is accelerating due to the Czech Republic’s high baseline industrial electricity tariffs and the European Green Deal. A modern high-frequency switch-mode power supply (SMPS) delivers system efficiencies above 90–93%, contrasted with 70–75% for older SCR units under variable tank loads. On a continuous 10,000A / 12V galvanizing line running 6,000 hours per year, this difference represents over 120,000 kWh in conserved electricity annually, recouping capital investment within 14 to 18 months solely on utility bills.
Second, the modernization of Ostrava’s manufacturing ecosystem relies heavily on automated SCADA and Industry 4.0 connectivity. Manual dial adjustment of tank voltages is completely obsolete. Modern plants require Modbus-RTU, Profibus, or analog 0–10V/4–20mA interfaces connected directly to Siemens or Allen-Bradley PLCs. Fenvix integrates industrial communication modules that transmit real-time current density, output ripple values, cumulative Ampere-hour (Ah) dosing data for brightener replenishment, and fault diagnostics directly to the control room, preventing catastrophic batch stripping due to human operator omission.
Third, physical factory space constraints in urbanized Ostrava production halls prioritize power density. Our high-frequency transformer cores, built with nano-crystalline magnetic alloys operating between 20kHz and 50kHz, occupy less than one-third of the footprint and weight of traditional 50Hz iron-core units. This enables galvanic workshops to expand line throughput or double anode busbar feeds without extending building foundations or constructing separate exterior substation rooms.
In-House Mechanical & Electrical Fabrication
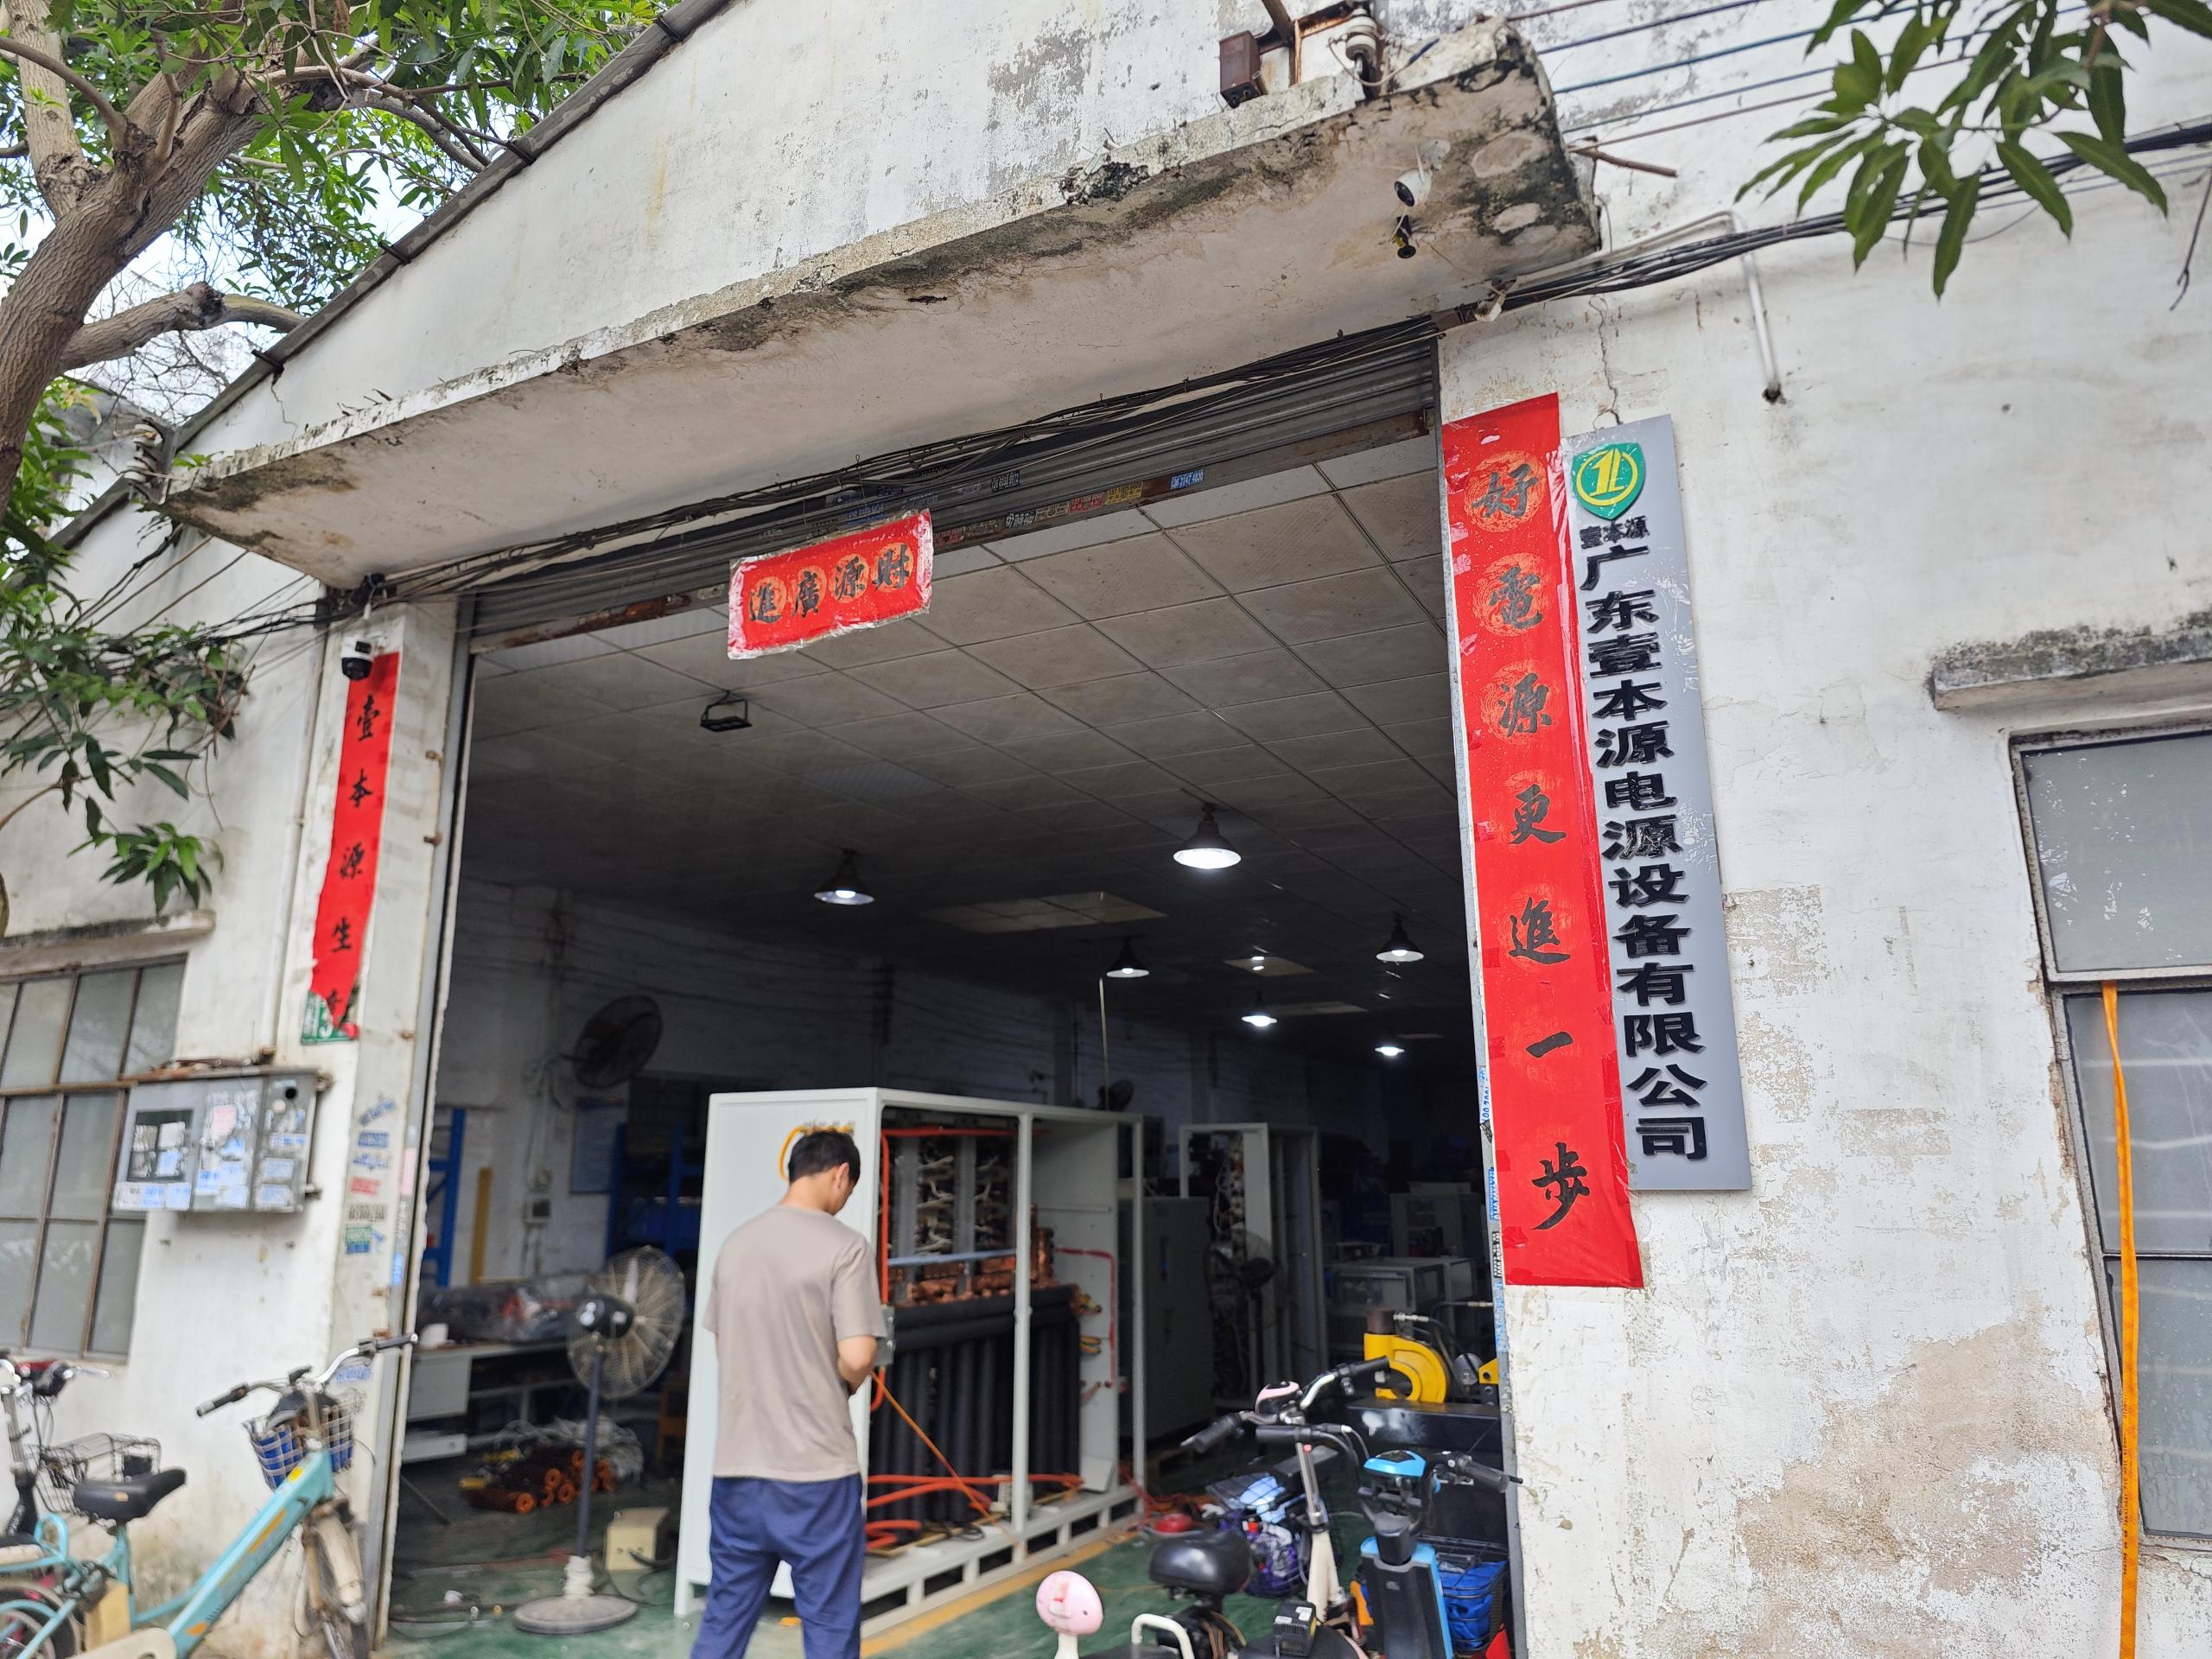
Unlike trading entities, Guangdong Fenvix controls every phase of production inside our 3,000m² facility. From CNC plate shearing, automated turret punching, and precision tapping of heavy electrolytic copper busbars to multi-layer PCB potting, vacuum impregnation, and closed-loop thermal testing, we ensure that power supplies shipped to European facilities endure the harshest chemical processing atmospheres.
Every plating rectifier undergoes a non-negotiable 48-hour burn-in under dynamic full-load cycles before crate departure, documented with individual oscilloscope waveforms, temperature probe logs, and dielectric withstand test reports.
Why Moravian-Silesian Engineers Partner with Fenvix
Combining direct Chinese factory pricing and agile engineering customization with European conformity and rigorous quality assurance.
ISO 9001 & CE Certified
Full CE LVD (EN 61010-1) and EMC (EN 61000-6-2/4) compliance, fully audited on-site by TÜV Rheinland for frictionless EU customs clearance.
Zero Minimum Order Quantity
No MOQ policy. We manufacture single-unit prototypes for pilot R&D lines as meticulously as 50-unit batches for factory expansions.
Tailored Non-Standard Ratings
Standard catalogues cannot solve unusual bath layouts. We construct custom voltages (6V–3200V) and currents up to 15,000A to your exact tank footprint.
DDP Delivery to Ostrava
Comprehensive logistical handling: maritime, rail freight via the New Silk Road, or expedited air cargo directly to your industrial gate with all duty cleared.
Frequently Asked Questions: Rectifier Sourcing in Ostrava
Practical answers to technical, logistical, and warranty considerations faced by Czech engineering and procurement professionals.
Can Fenvix rectifiers seamlessly replace legacy Czech-built or German thyristor rectifiers in Ostrava facilities?
How does water cooling compare against air cooling in Ostrava's typical workshop conditions?
What documentation and CE standards are provided for regional industrial safety inspections in the Czech Republic?
What is the typical shipping lead time and customs procedure from your Guangdong factory to Ostrava?
How is after-sales warranty and component replacement handled remotely for Czech buyers?
Upgrade Your Electrochemical Precision Today
Connect with our senior power electronics application team. We review your process bath calculations, input electrical constraints, and duty parameters to recommend the most cost-effective, high-efficiency configuration for your plant.
Get Catalog