High-Efficiency Oxidation & Finishing Power Units
Engineered with dual CC/CV modes, soft ramp starts, low ripple factor (<1%), and corrosive-proof cooling topology. Benchmarked for extreme duty cycles in continuous industrial processing.

12V-15V 5000A-6000A 75KW Water Cooled Rectifier
- Rated Power75 kW
- Output Range12-15V / 5000-6000A
- Cooling TypeDeionized Water Cooled
- Control ProtocolRS485 Modbus / 4-20mA

100A–3000A Anodic Oxidation DC Rectifier
- TopologyIGBT Inverter Circuit
- Voltage Options12V / 24V / 48V / 60V
- Control ModeConstant Current / Voltage
- ApplicationAluminum Hard Anodizing
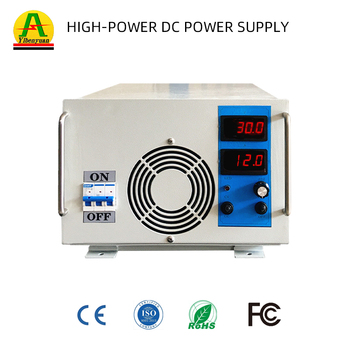
Titanium Alloy Micro-Arc Oxidation Supply
- Output Spec0-150V / 0-50A Steady
- RampingMulti-stage Slope Curves
- ProtectionOvervoltage, Short, Phase Loss
- ApplicationMedical & Aerospace Alloys

Customized 8000A 12V High-Output Rectifier
- Current Rating8000A Continuous
- ChassisSealed IP54 Anti-Corrosion
- Thermal MgmtPure Copper Water Block
- Efficiency≥ 91.5% at Full Load

48V 625A 30KW Polarity Reversing Rectifier
- Reversal ModeProgrammable Forward/Reverse
- Timer Control4-Stage Automated Sequence
- Peak Current625A Synchronous
- ApplicationDescaling & Anodic Stripping

800V 50A 20KW Programmable DC Source
- Output Range0-800V Adjustable
- Ripple & Noise≤ 0.2% RMS Full Scale
- InterfaceLAN, CANopen, RS485
- Use ScopeHV Aging, Dielectric Film Test

300kW 20V 15000A High-Capacity System
- Total Output300 kW Ultra-Heavy Load
- Max Current15,000A Continuous DC
- Parallel ConfigN+1 Modular Synchronization
- ApplicationMajor Automotive E-Coating

5kW Precision Electrophoresis DC Supply
- Voltage Stability±0.5% Load Regulation
- ProtectionSpark Quenching Circuit
- Input Line380VAC 3-Phase ±15%
- Use ScopeElectrophoretic Coating & Lacquering
Precision Oxidation Deployments in the Žilina Industrial Core
Aligning precision switch-mode direct-current topologies with the rigorous electro-finishing benchmarks demanded by northern Slovakia's advanced manufacturing and tier-supplier clusters.
Strategic Industrial Synergy with Žilina’s Engineering Hub
The Žilina Region represents one of Central Europe's most concentrated automotive, mechanical engineering, and metallurgical corridors. Home to global OEM vehicle assembly plants, tier-1 transmission builders, and specialized aluminum extrusion foundries, the demand for surface treatment consistency has moved far beyond legacy silicon controlled rectifiers (SCR). Modern anodizing operations—ranging from Type II architectural sulfur bath finishes to Type III severe-duty military hard-coating—require exact control of film formation dynamics. When local facilities treat structural chassis members, turbocharger impellers, or hydraulic manifold blocks, any ripple instability causes erratic cell pore geometry, inconsistent dielectric barrier layers, and catastrophic fatigue vulnerability.
By engineering China-manufactured, European-certified high-frequency switch-mode power supplies directly for Žilina's manufacturing ecosystem, Fenvix bridges the gap between capital efficiency and elite electro-finishing precision. Our IGBT high-frequency architecture operates at 20 kHz to 50 kHz switching frequencies, reducing ripple factor below 1% under harsh current spikes. This enables local electroplating and oxidation workshops around Žilina, Martin, and Čadca to eliminate the thermal burnt spots commonly caused by standard 50Hz SCR transformers, ensuring exact color uniformity, unyielding corrosion barrier formation, and total compliance with VDA 6.3 and ISO/TS automotive surface standards.
Automotive Aluminum Structural Components
Žilina's thriving automotive supply chain demands hard-coat anodizing on structural subframes, battery pack enclosures, and brake pistons. Fenvix units deliver programmable multi-step current ramps that mitigate thermal stress during initial oxide barrier formation, preventing microscopic crazing in EN AW-6060 and 6082 alloy matrices.
Precision Rail & Heavy Transport Metallurgy
Adjacent to the vital transport hubs connecting Slovakia, Czechia, and Poland, local plants specialize in heavy traction components. Our high-amperage (up to 15,000A) water-cooled rectifiers supply stable electro-cleaning, hard anodizing, and zinc-nickel plating capable of surviving severe road de-icing salts and mechanical friction.
Specialized Titanium Medical & Tooling Finishing
Serving precision CNC machinists and precision surgical tooling producers in northwestern Slovakia, Fenvix 150V micro-arc and color-anodizing rectifiers provide ultra-tight millivolt voltage regulation to produce sterile, biocompatible, and vibrant titanium oxide films with zero color variance across production batches.
| Oxidation Process Type | Local Metal Substrate | Power Parameter Profile | Key Process Advantage |
|---|---|---|---|
| Type II Sulfuric Acid Anodizing | EN AW-5052, 6063 Aluminum | 15V–24V DC, 1000A–5000A (CC Mode) | Uniform porous cell density; optimized for dye absorption and decorative automotive trims. |
| Type III Hard Anodizing | EN AW-2024, 7075 Extrusions | 40V–75V DC, Pulsed / Ramp Current Profile | Sub-zero bath stability; achieves 50–70 μm film thickness without surface burning or spalling. |
| Titanium Spark/Micro-Arc Oxidation | Grade 5 Ti-6Al-4V Medical/Aero | 100V–180V DC, Controlled Spark Discharge | Forms ceramic-like crystalline rutile/anatase coatings with extreme wear and corrosion resistance. |
| Cataphoretic E-Coating (KTL) | Stamped Galvanized Sheet Steel | 200V–400V DC, 50A–300A Digital Steps | High throw-power coating inside deep hollow sections of welded car bodies without run marks. |
Surface Finishing Technology Shifts in Slovakia
How the European Green Deal, surging industrial kilowatt costs, and Industry 4.0 integration are rewriting procurement criteria for electro-chemical power sources.
Thermal & Power Efficiency Rationalization
With Central European energy pricing under relentless scrutiny, surface treaters in the Váh River Basin cannot justify legacy oil-cooled or thyristor systems operating at 65% to 75% efficiency. Fenvix modern high-frequency IGBT architectures push overall electrical efficiency above 90%, slashing facility power consumption while cutting cooling chiller loads by over 30%.
Digital Twin & SCADA Network Integration
Manual dial-based power racks are obsolete in modern Žilina smart factories. Today’s plating plants require real-time bath resistance monitoring, automated recipe parameter downloads via Profinet or Modbus-RTU, and continuous timestamped logging of ampere-minutes for full batch traceability in compliance with automotive audits.
Sealed Cabinets & Harsh Acid Atmosphere Defense
In hot sulfuric acid and hard-coat electrolyte environments, standard cooling fans ingest corrosive fumes that rapidly destroy circuit boards. The local trend has shifted toward fully sealed IP54 chassis combined with isolated water-cooling jackets, safeguarding inner electronic components and multiplying MTBF lifespan.
Frequently Asked Questions by Žilina Buyers
Direct answers addressing technical configuration, European conformity, shipping logistics, and commissioning support for operations in Slovakia.
What exact parameters are required to calculate rectifier sizing for our anodizing tank? +
How do Fenvix power supplies ensure full compliance with EU and Slovak industrial standards? +
When should our plant choose water-cooled over forced air-cooled rectifiers? +
What are the lead times and delivery logistics from Guangdong to Žilina? +
Can Fenvix supply units without Minimum Order Quantity (MOQ) for pilot test runs? +
How do you handle commissioning and after-sales support for clients in Central Europe? +
Why Tier-1 Industrial Plants Partner with Fenvix
Combining complete vertical integration—from cabinet sheet metal punching to final burn-in oscilloscope load verification—with over 13 years of field-proven power innovation.
Full Vertical Production
We own and control every step: precision CNC laser cutting, busbar bending, tapping, module wiring, and final testing. In-house mechanical manufacturing protects design integrity and prevents third-party fabrication delays.
Strict Load & Burn-In Testing
Every single power supply undergoes full-load resistance bank testing for a minimum of 24–48 continuous hours. Waveform fidelity, switching thermals, and ripple factor are rigorously benchmarked before crating.
TÜV Rheinland Audited
Our 3,000m² manufacturing facility in Guangdong is physically inspected and verified by TÜV Rheinland. We maintain transparent production logs, strict ISO 9001:2015 tracking, and globally recognized business credit scores.
Bespoke OEM / ODM Agility
From custom DC voltage envelopes (up to 3,200V) to special pulsed waveforms, reversing circuits, and multi-channel remote PLC touch interfaces, our engineering department realizes tailored solutions rapidly.




Request a Custom Technical Sizing & Factory Quote
Connect with our senior electrical engineering group today. Whether upgrading an active anodizing tank in Žilina or architecting an automated turn-key electro-coating plant from scratch, we provide comprehensive thermal sizing, schematics, and factory-direct pricing within 24 hours.