Featured Model

Manufactured under strict ISO 9001 quality supervision, these factory-direct power supplies are configured to standard European industrial voltages (380V/400V 50Hz) and tested under full continuous load for heavy industrial electrodeposition.




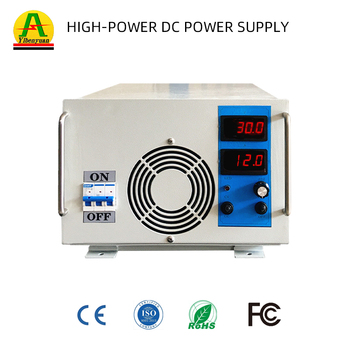


North Macedonia's transition into a primary tier-1 and tier-2 automotive component export hub across the Western Balkans demands modern surface protection technologies. Pulse electroplating rectifiers replace obsolete silicon controlled rectifiers (SCR) to meet strict European Union corrosion resistance benchmarks.
Technological Industrial Development Zones (TIRZ) house multinational manufacturers delivering electronic wiring harnesses, catalytic converters, and precision machined stampings for German and Central European automotive OEMs. Periodic reverse pulse power supplies drastically improve throw power in deep blind micro-vias and tight mechanical recesses, eliminating uneven edge buildup in high-density components.
The industrial corridor spanning Bitola, Ohrid, and Prilep focuses heavily on metal forming, heavy agricultural machinery, industrial fittings, and specialized die manufacturing. Our water-cooled pulse rectifiers provide continuous cathodic polarization while minimizing hydrogen embrittlement in high-tensile fasteners, hardened gear profiles, and hydraulic valves undergoing heavy hard-chromium plating.
Regional architectural aluminium extrusion and zinc galvanizing plants demand tight energy efficiency due to Western Balkan grid tariffs. Fenvix high-frequency IGBT units operate at a power factor exceeding 0.95, slashing reactive power charges and optimizing chemical bath consumption through consistent, ultra-low ripple voltage delivery.
A quantified metallurgical and electrical comparison showing why Macedonian electroplating lines are replacing legacy thyristor systems with programmable pulse power supplies.
| Performance Parameter | Legacy Thyristor / SCR Rectifier | High-Frequency DC IGBT System | Fenvix Dual-Pulse & Periodic Reverse System |
|---|---|---|---|
| Current Density Limit | Low (Burn risks at edges: 2-4 A/dm²) | Moderate (Stable CC mode: 4-6 A/dm²) | Very High (Up to 15-25 A/dm² Peak) |
| Microstructure & Grain Size | Coarse, columnar crystal growth | Fine crystalline morphology | Ultra-dense equiaxed nanograins (< 50nm) |
| Hydrogen Embrittlement Risk | High (Continuous proton reduction) | Moderate (Linear potential gradient) | Minimized (Hydrogen desorbs during t-off/reverse cycle) |
| Precious Metal Bath Efficiency | Standard over-consumption (15-25% waste) | Improved distribution uniformity | Saves 18-35% in Gold (Au), Silver (Ag), and Nickel (Ni) |
| Grid Electrical Efficiency | 68% - 76% (High phase distortion) | 88% - 91% (High-frequency conversion) | 90% - 93% (Cos φ ≥ 0.95 low harmonic distortion) |
| Throwing Power in Blind Holes | Poor (Substantial dog-bone effect) | Standard European tolerance | Near 1:1 plating ratio in deep high-aspect trenches |
In standard DC electroplating, a continuous cathodic diffusion layer builds rapidly at the substrate boundary. This depleted zone starves metal ion concentrations, forcing operational amperages down to prevent burning, pitting, and dendritic growth.
Fenvix pulse electroplating power supplies introduce programmable pulse-on ($T_{on}$) and pulse-off ($T_{off}$) microsecond intervals. During $T_{on}$, an intense capacitive burst deposits metal ions under high overpotential, instigating massive crystal nucleation. During $T_{off}$, current drops to zero or reverses into an anodic pulse, replenishing the local ion concentration while selectively dissolving microscopic nodules and discharging trapped molecular hydrogen gas.

Operating from our 3,000m² specialized power equipment manufacturing facility in Guangdong, China, Fenvix supplies demanding metallurgical, chemical, and aviation enterprises across five continents. Verified on-site by TÜV Rheinland.
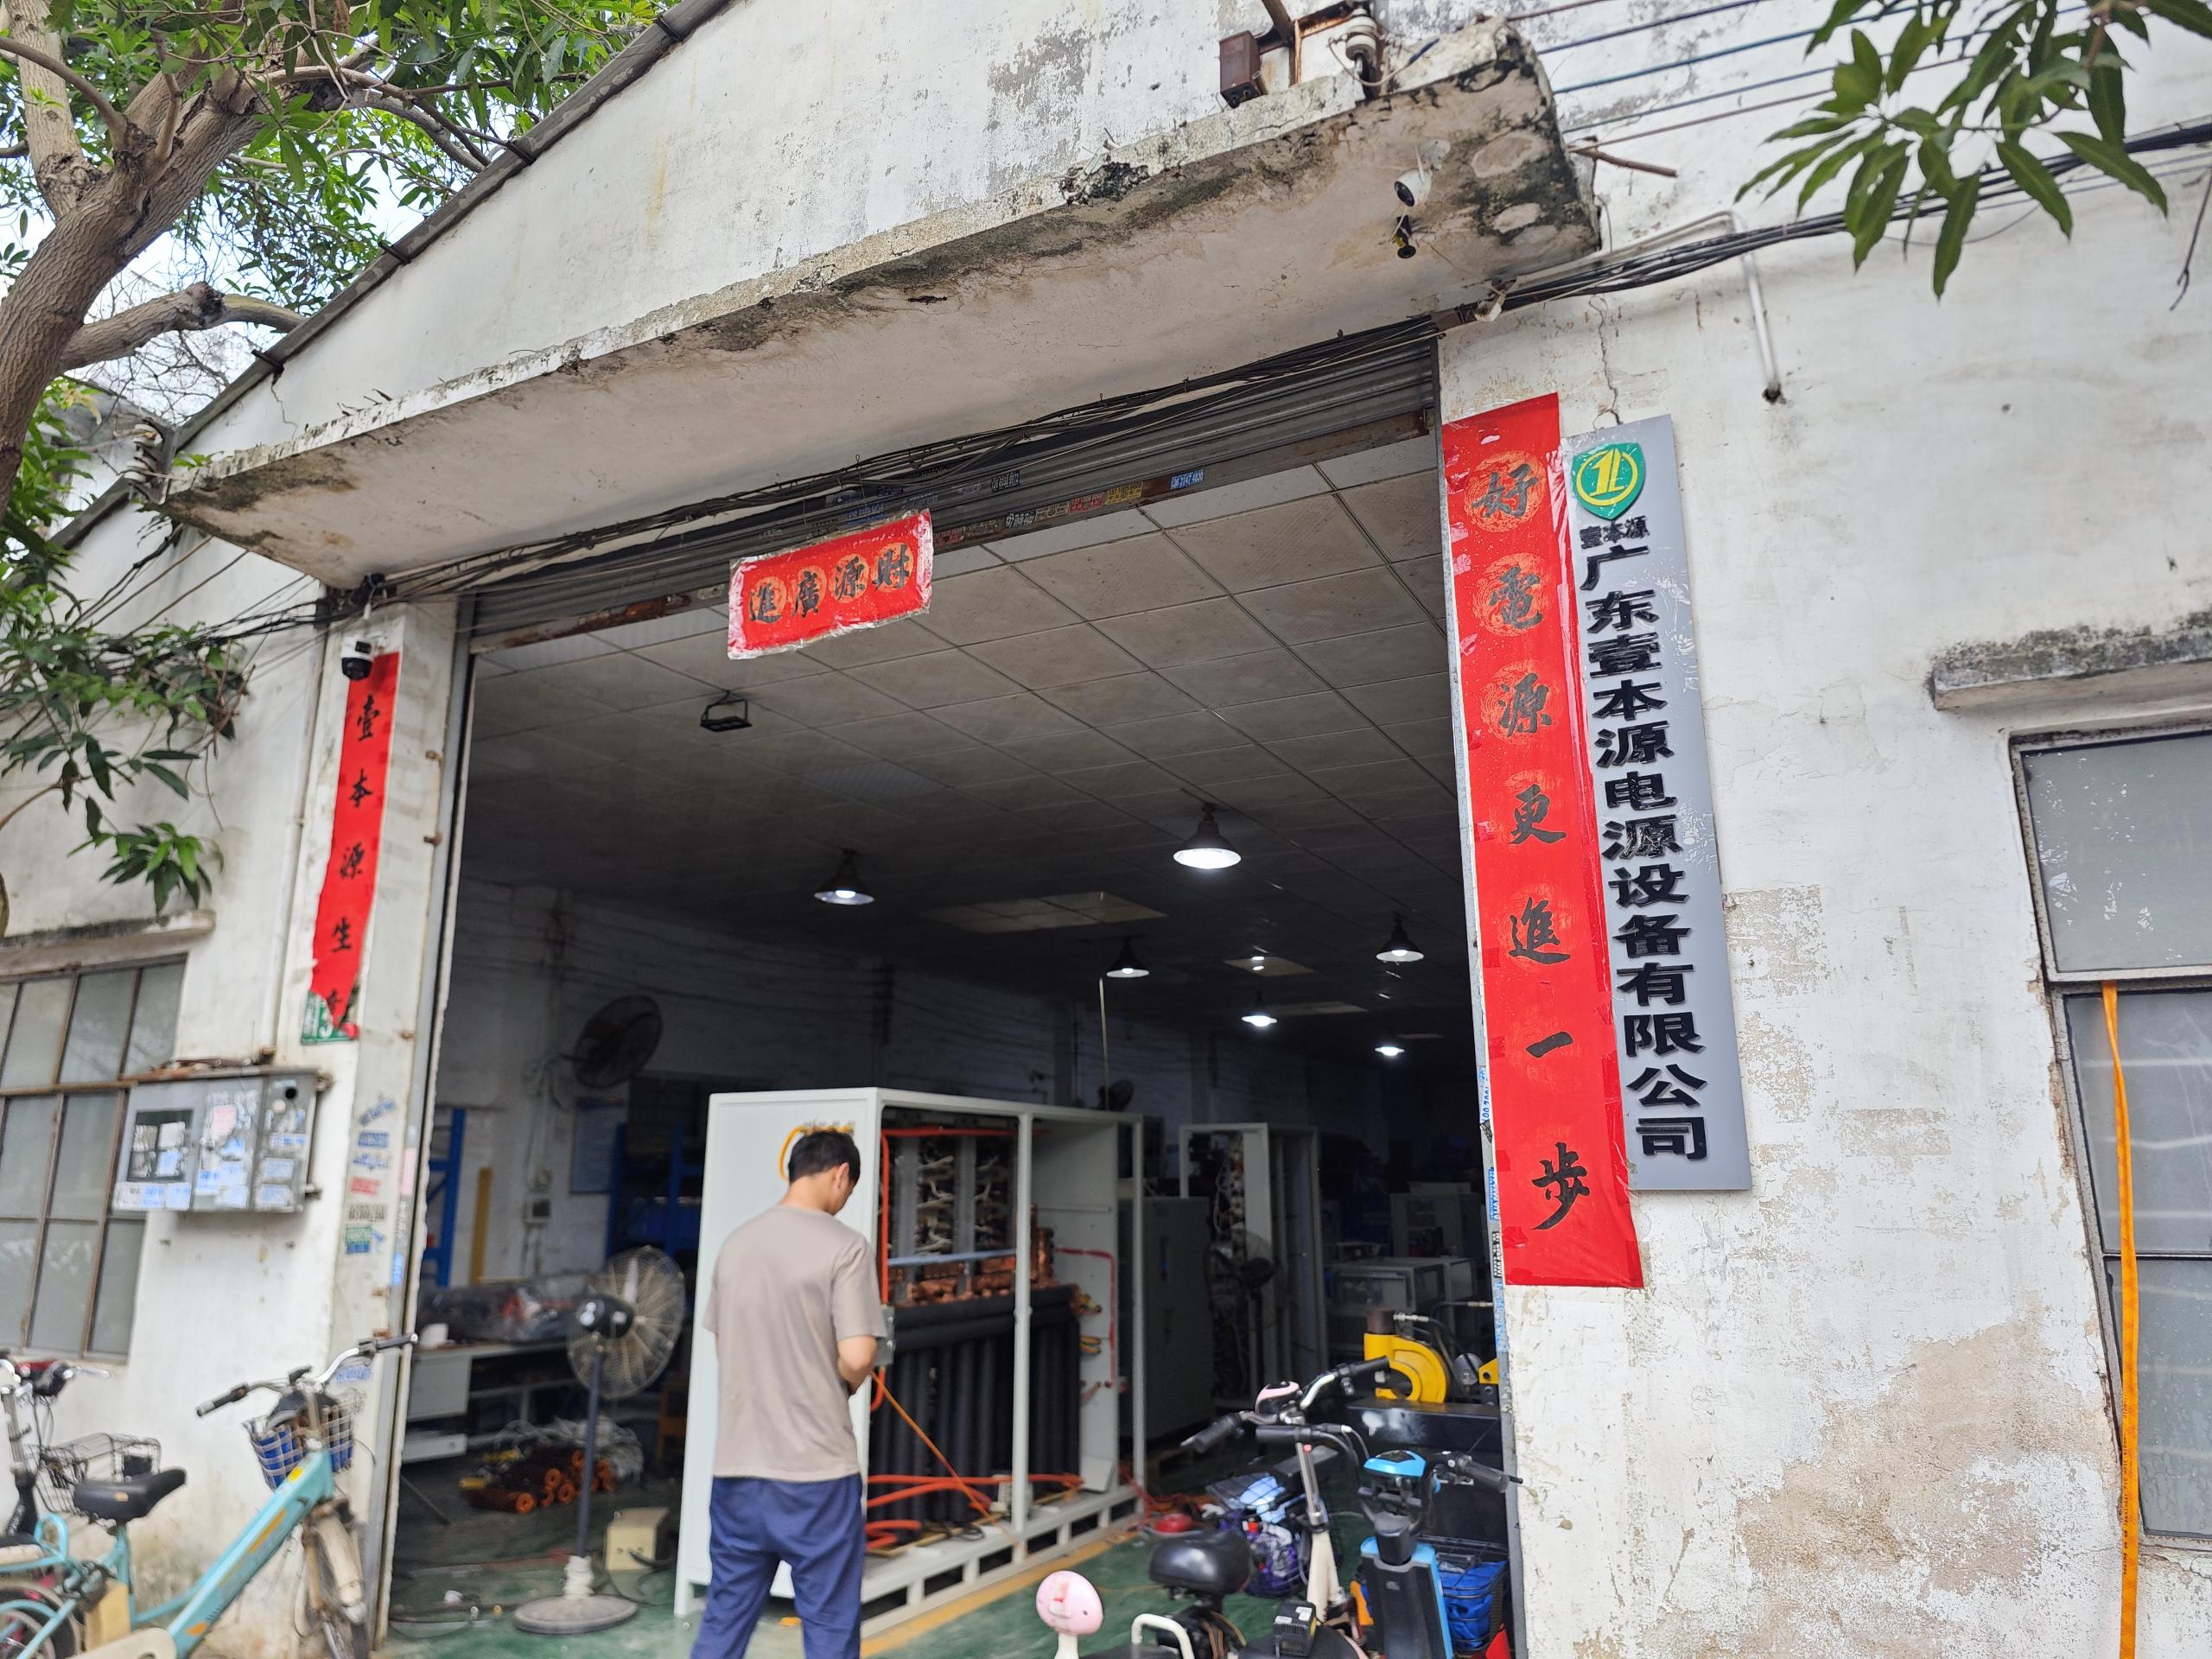
Unlike export traders or assembly assemblers who outsource sheet metal and magnetic winding, Fenvix maintains complete vertical control over heavy mechanical fabrication, CNC busbar milling, CNC drilling, transformer winding, and cabinet coating.
Every single power unit earmarked for North Macedonia and the European customs corridor undergoes mandatory 100% full-current burn-in testing under real resistive dummy loads, followed by detailed digital oscilloscope validation for pulse rise time, peak ripple, and thermal balance.
Documented traceability from incoming cold-rolled silicon sheets and Infineon IGBT modules to finished seaworthy crate sealing.
Native RS485 Modbus, Profibus, CANopen, and isolated 0-10V/4-20mA analog interfaces allow seamless SCADA and PLC synchronization.
Flexible DDP (Delivered Duty Paid), CIF Thessaloniki/Durrës, FOB, and EXW agreements, transacting conveniently in EUR and USD.
Direct communication with certified power electronic engineers for custom waveform profiling and tank busbar dimensioning.
Addressing engineering specifications, logistical routes, grid compliance, and operational best practices for electroplating equipment procurement.
Send your electrolyte tank dimensions, desired peak current, voltage range, and waveform requirements. Our application engineering team will provide a tailored technical proposal within 24 business hours.