Water Cooled

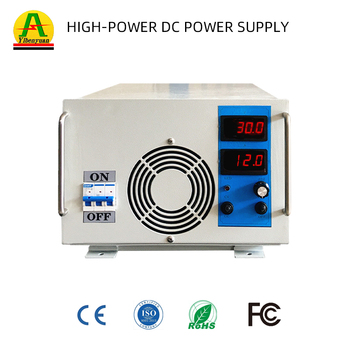
12V/15V 5000A–6000A 75kW Water-Cooled DC Rectifier
- TopologyHigh-Frequency IGBT
- Output12V–15V / 5000A–6000A
- ModeCV / CC Digital Display
- CoolingDeionized / Chilled Water
Engineered to deliver exceptional current density control, high dynamic response, and sub-1% ripple for critical surface treatment operations.






A technical evaluation of high-frequency switch-mode rectifiers versus legacy thyristor equipment in Swedish manufacturing ecosystems.
In the advanced manufacturing corridors stretching from Greater Stockholm through Södertälje, Västerås, and Linköping, aluminum surface treatment is shifting away from bulk commercial finishing toward high-precision functional coatings. Industrial sectors such as automotive electrification, marine hardware, medical robotics, and defense aerospace demand extreme coating homogeneity, narrow micron-tolerance film thicknesses, and verifiable metallurgical performance. Achieving these criteria while complying with rigorous environmental frameworks and elevated electrical utility costs requires a fundamental upgrade in rectification technology.
Traditional silicon-controlled rectifiers (SCR or thyristor systems) utilize line-frequency 50Hz transformation. When operating at partial load during voltage-ramp phases in hard anodizing, SCR units exhibit high current ripple (often exceeding 5% to 8%) and a poor power factor dropping below 0.70. High ripple directly introduces excessive Joule heating into the aluminum workpiece and acidic electrolyte, triggering localized dissolution of the anodic oxide barrier layer and causing "burning" or micro-cracking. In contrast, modern switch-mode IGBT (Insulated-Gate Bipolar Transistor) DC power supplies switch at frequencies between 20kHz and 50kHz. This delivers a virtually pure, ripple-free direct current with dynamic adjustment speeds under 10 milliseconds, enabling absolute barrier layer stabilization, denser cellular pore architecture, and up to 25% lower electrolyte cooling energy overhead.
| Performance Characteristic | Legacy SCR / Thyristor Rectifier | Fenvix High-Frequency IGBT Solution | Operational Impact in Stockholm Operations |
|---|---|---|---|
| Conversion Efficiency | 72% – 82% (Significant heat waste) | 90% – 94% Across 30–100% Load | Reduces factory power bills and heat emissions in closed facilities. |
| DC Current Ripple (RMS) | 4.0% – 8.0% (Higher at low voltages) | ≤ 1.0% Across Entire Operating Range | Eliminates burning, optimizes film hardness, and reduces acid chilling loads. |
| Power Factor (cos φ) | 0.65 – 0.78 (Generates reactive penalties) | ≥ 0.95 (Active correction available) | Complies with Vattenfall & Ellevio power quality standards without capacitor banks. |
| Dynamic Ramp Control | Slow analog response (100–300 ms) | Microsecond digital response (<10 ms) | Essential for precision titanium coloration and micro-arc oxidation routines. |
| Chassis Footprint & Mass | Heavy oil-filled or bulky cabinets | 1/3 Volume, 1/4 Weight, Modular Rack | Saves valuable floor space in high-rent urban and industrial zones. |
Tailored rectification profiles engineered for specific Scandinavian industrial requirements, environmental criteria, and automated processing lines.
Heavy-duty aluminum heat sinks and battery tray casings fabricated around Södertälje and Gothenburg require dense, dielectric-insulating Type III hard anodized layers. Our 5000A–15000A water-cooled rectifiers maintain exact current density across complex profiles, eliminating dielectric breakdown under continuous high voltages.
Precision medical device clusters in Solna and Uppsala rely on high-voltage DC power modules for color-coding and passivation of titanium orthopedic screws and surgical tools. Our 150V/50A digitally programmable units allow precise voltage-step regulation within 0.1V, achieving repeatable oxide interference colors.
In Kista, advanced microwave radar housings, optical transceiver shells, and 5G chassis demand chemical nickel-gold plating and high-precision copper electrodeposition. Fenvix compact bench and rack-mount rectifiers deliver sub-millivolt stability for micro-via metallization with negligible electromagnetic interference.
Naval components and Baltic marine structural parts are subject to harsh brackish water corrosion. Hard coat anodizing according to MIL-A-8625 Type III requires cold-electrolyte processing at sub-zero temperatures. Our pulse-reverse and current-ramping power units generate abrasion-resistant oxide depths exceeding 50 microns without surface overheating.
Municipal wastewater and industrial cooling circuits in the Mälardalen region employ electro-coagulation and electrolytic descaling to curb chemical usage. Fenvix automated polarity-reversing 48V/625A power units clean fouled electrodes automatically through timed inversion, eliminating chemical descaling down-time.
Understanding shifting technical, environmental, and digital mandates governing high-power electrical equipment investments.
With Sweden's commitment to climate neutrality and volatile grid tariffs, surface finishers are eliminating air-cooled rectifiers that exhaust hot air inside conditioned workshops. Water-cooled rectifiers direct thermal losses into closed glycol loops that feed plant floor heating or municipal heat exchange circuits, reducing overall operational carbon footprint.
Swedish OEMs require complete recipe-driven automation. Modern power supplies must abandon basic analog dials in favor of industrial fieldbus interfaces like Modbus-RTU, Profinet, and Ethernet/IP. Every anodizing run requires timestamped ampere-minute tracking, voltage-ramp verification, and alarm telemetry exported directly to plant MES databases.
Scandinavian utility companies impose strict Total Harmonic Distortion (THDi) caps on major manufacturing consumers. Fenvix units feature optimized multi-phase front-ends and active power factor correction, maintaining THDi below regulatory limits and protecting neighboring robotics and sensitive laboratory instruments from grid pollution.
From internal sheet-metal fabrication to automated 100% full-load burn-in, we eliminate intermediaries to deliver cost-effective engineering certainty.
We own and operate precision shearing, CNC punching, milling, drilling, and copper busbar tapping lines. Chassis design, heat sink geometry, and cabinet IP ratings are fully controlled under one roof.
Certified under rigorous ISO 9001 management protocols. Our production facility and trade qualifications are verified on-site by TÜV Rheinland, with CE, RoHS, LVD, and EMC documentation available.
We actively support R&D institutions, university prototypes, and pilot facilities with single-unit custom builds, alongside high-volume scheduled delivery for Tier-1 production lines.
Consult directly with our electrical design team on voltage headroom, cable drop compensation, chiller pipe diameters, and control system pinouts before final purchase orders are issued.
 Assembly Bay
 Finished Units
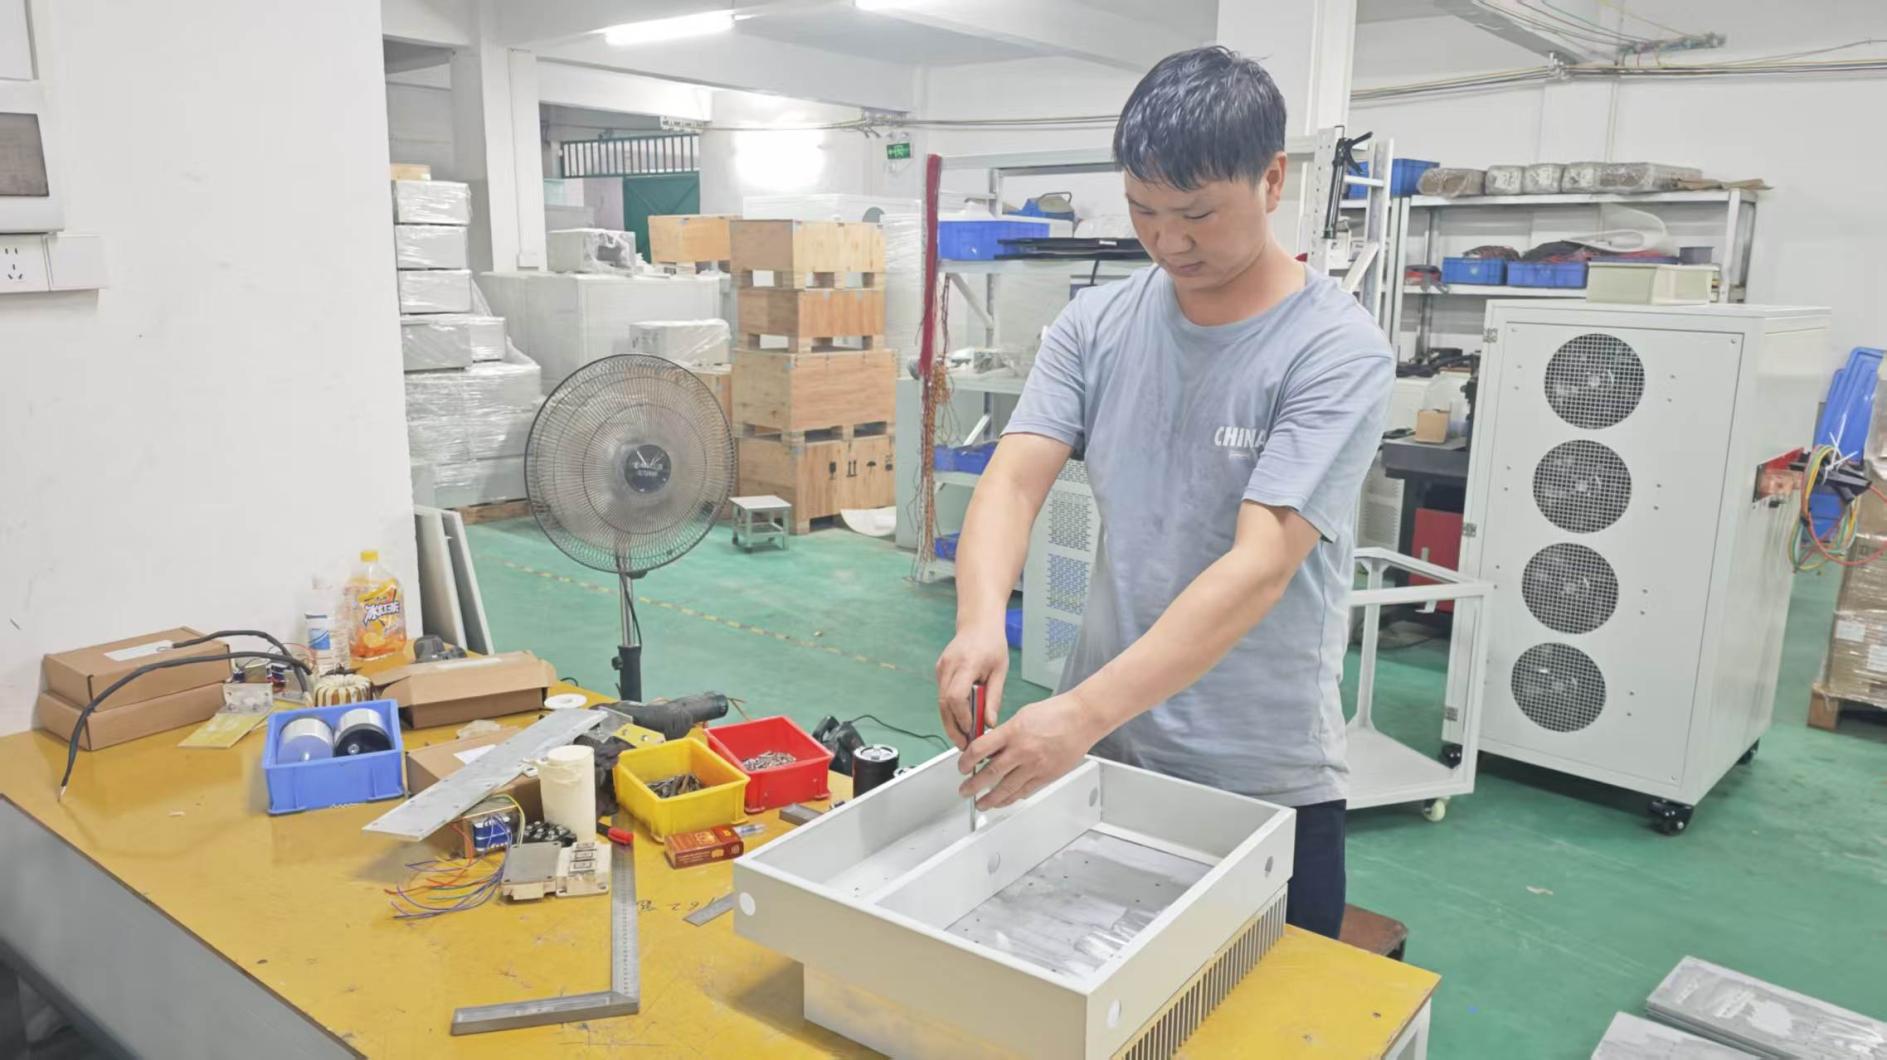 Wiring Integration
 Load Commissioning
 Waveform Validation
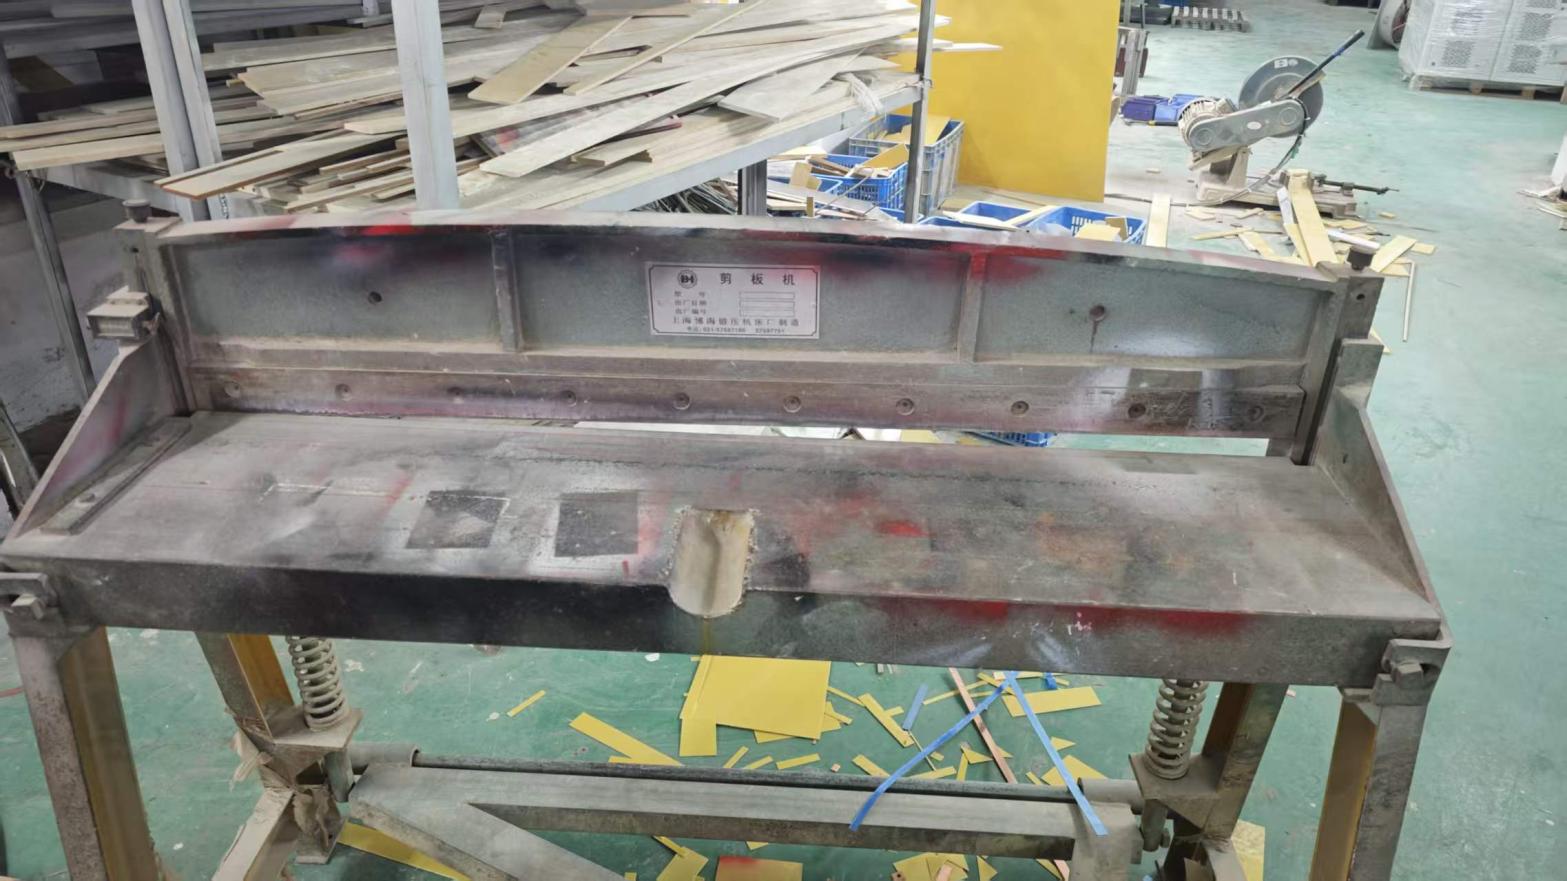 CNC Sheet Metal
Key technical, electrical, logistical, and warranty considerations addressed for buyers in Sweden.