Water Cooled

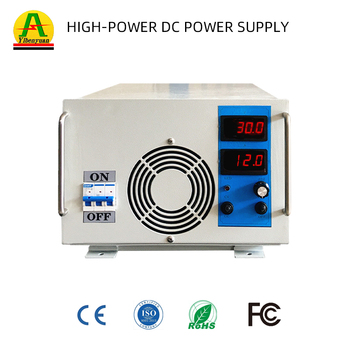
12V/15V 5000A–6000A 75kW Rectifier
- TopologyHigh Frequency IGBT
- RegulationCV / CC Digital Display
- CoolingDeionized Liquid Circuit
Field-proven topologies built with high-speed IGBT semiconductors, programmable logic controls, and closed-loop liquid thermal management to satisfy rigorous European metallurgical surface finishing standards.






The city of Prešov, alongside the broader Prešov and Košice regional manufacturing basins in Eastern Slovakia, represents a vital hub for precision machinery, automotive component stamping, heavy engineering, and specialized electrical equipment manufacturing. Local electroplating plants, contract job shops, and in-house tier-supply finishing lines operate under rigorous requirements dictated by European automotive primes, industrial machinery OEMs, and structural equipment suppliers. The surface engineering infrastructure across eastern Slovakia has progressively transitioned toward higher-tolerance anti-corrosion barrier coatings, hard-chrome alternatives, micro-crack chrome plating, passivated zinc-nickel alloys, and decorative or hard anodizing for extruded aluminum components.
In this operating theater, legacy thyristor (SCR-based) transformers increasingly fall short of modern process specifications. Silicon-controlled rectifiers exhibit slow dynamic step responses, low electrical conversion efficiencies (often below 75% at lower utilization ranges), high input reactive power penalties, and substantial current ripple at modulated loads. When electroplating intricate geometries or high-stress automotive shafts, high ripple currents generate micro-porosities, unequal crystalline growth, and thickness variations across the cathode boundary layer. Modern switch-mode power supplies (SMPS) operating with insulated-gate bipolar transistors (IGBTs) solve these systemic bottlenecks by operating at switching frequencies between 20 kHz and 50 kHz. This high switching speed suppresses RMS ripple to less than 2% across 10% to 100% of the rated load curve, ensuring uniform throwing power, accelerated deposition kinetics, and significantly reduced chemical additive consumption for electroplaters in the Prešov region.
Deploying heavy-duty DC power supplies in Slovakian finishing facilities requires meticulous attention to operational environments, chemical exposure risks, and grid compliance. Plant managers in industrial corridors such as Prešov-Juh, Kežmarok, and nearby Poprad must balance continuous multi-shift production schedules with volatile chemical atmospheres characterized by acidic mists, high ambient humidity, and thermal variations. Fenvix metal finishing power systems address these localized environmental vectors through differentiated architectural designs.
Our heavy-duty liquid-cooled power architectures decouple internal power semiconductors, gate drivers, and high-frequency planar transformers from corrosive ambient air. By passing cooling media through sealed deionized-compatible aluminum cold plates or nickel-brazed copper heat sinks, the internal electronics cabinet achieves true IP54/IP65 environmental isolation. Plating facilities handling zinc-nickel, copper acid tanks, and chromium trioxide baths eliminate the vulnerability of forced-air ducting drawing airborne acid droplets across sensitive circuitry. In contrast, for lighter auxiliary plating lines and testing rooms, our forced-air cabinets utilize tropicalized conformal coatings, internal channel separation, and rear-exhaust air conduits to prolong component longevity without complex chiller plumbing.
Delivers stable constant current (CC) control with sub-2% ripple, ensuring defect-free deposition of alkaline zinc-nickel coatings on chassis fasteners, hydraulic tubing, and powertrain brackets matching OEM specifications.
Configured with multi-step voltage ramping profiles and high-voltage compliance up to 150V DC for sulfuric acid and hard-coat anodizing of precision-machined aluminum profiles and titanium sub-assemblies.
Supplies stable, pulse-free DC voltage across large dip tanks, establishing uniform film build on intricate pressed steel assemblies without pinholes, orange peel, or dielectric edge breakdown.
Automated polarity-reversal rectifiers clear cathode scaling during electrocoagulation and heavy metal precipitative recovery from rinse waters, eliminating manual acid-washing downtime.
High-speed loop response ensures absolute synchronization with line velocity variations, maintaining constant current density per surface area on high-speed copper, nickel, or tin plating strips.
The manufacturing sector in Eastern Slovakia is confronting two interrelated pressures: aggressive industrial decarbonization mandates backed by rising European energy spot prices, and strict compliance with EU environmental directives (including REACH restrictions on hazardous chromate formulations). Electrical efficiency in the plating room has evolved from an accounting afterthought to an existential competitive parameter.
Conventional thyristor rectifiers convert input AC to output DC with total system efficiencies rarely exceeding 70% to 78% when throttled down to typical operational voltages (e.g., 6V to 9V on an 18V rated machine). The remaining 22% to 30% of energy converts directly into waste heat, imposing secondary utility costs through high air conditioning and chiller plant loads. In contrast, Fenvix switch-mode rectifiers maintain a near-flat efficiency curve between 89% and 93% across their active output bandwidth, operating with an input power factor of ≥ 0.94. This reduces total grid kVA demand and prevents power harmonic pollution on facility transformers without requiring costly harmonic filter banks.
Furthermore, Industry 4.0 modernization across regional tier plants requires seamless communication between DC power sources and central SCADA or PLC networks. Fenvix units integrate standard RS485 Modbus-RTU, Profibus-DP, or Profinet protocols alongside isolated 0–10V / 4–20mA analog interfaces. Operating technicians can remotely set multi-stage amp-hour counters, trigger automated polarity-reversal routines, program soft-start voltage ramps, and log continuous thermal and load data directly into quality assurance records.
| Performance Specification | Legacy SCR / Thyristor Units | Fenvix High-Frequency IGBT SMPS | Operational Impact in Plating Shop |
|---|---|---|---|
| Conversion Efficiency | 70% – 78% at partial loads | 89% – 93% continuous | Cuts plant electrical utility consumption by 15–25% |
| Output DC Ripple | 5% – 15% RMS at dialed-down currents | ≤ 2% RMS full output scale | Eliminates micro-cracking; improves coating grain uniformity |
| Power Factor (λ) | 0.65 – 0.78 (variable with phase angle) | ≥ 0.94 fixed across operating band | Eliminates reactive energy utility surcharges |
| Physical Footprint & Mass | Heavy oil/air transformers (approx. 1200kg) | Compact modular design (approx. 280kg) | Saves 60% floor space; allows tank-side mounting |
| Process Control Dynamic | Slow response (100–200 ms) | Ultra-fast transient (≤ 10 ms) | Prevents burning during ramp-up and rack entry |
Every industrial power supply is fabricated, assembled, and load-tested in-house at our ISO 9001 certified facility, ensuring structural integrity, thermal safety, and exact electrical performance.
 Main Assembly Workshop
 Finished Rectifier Cabinets
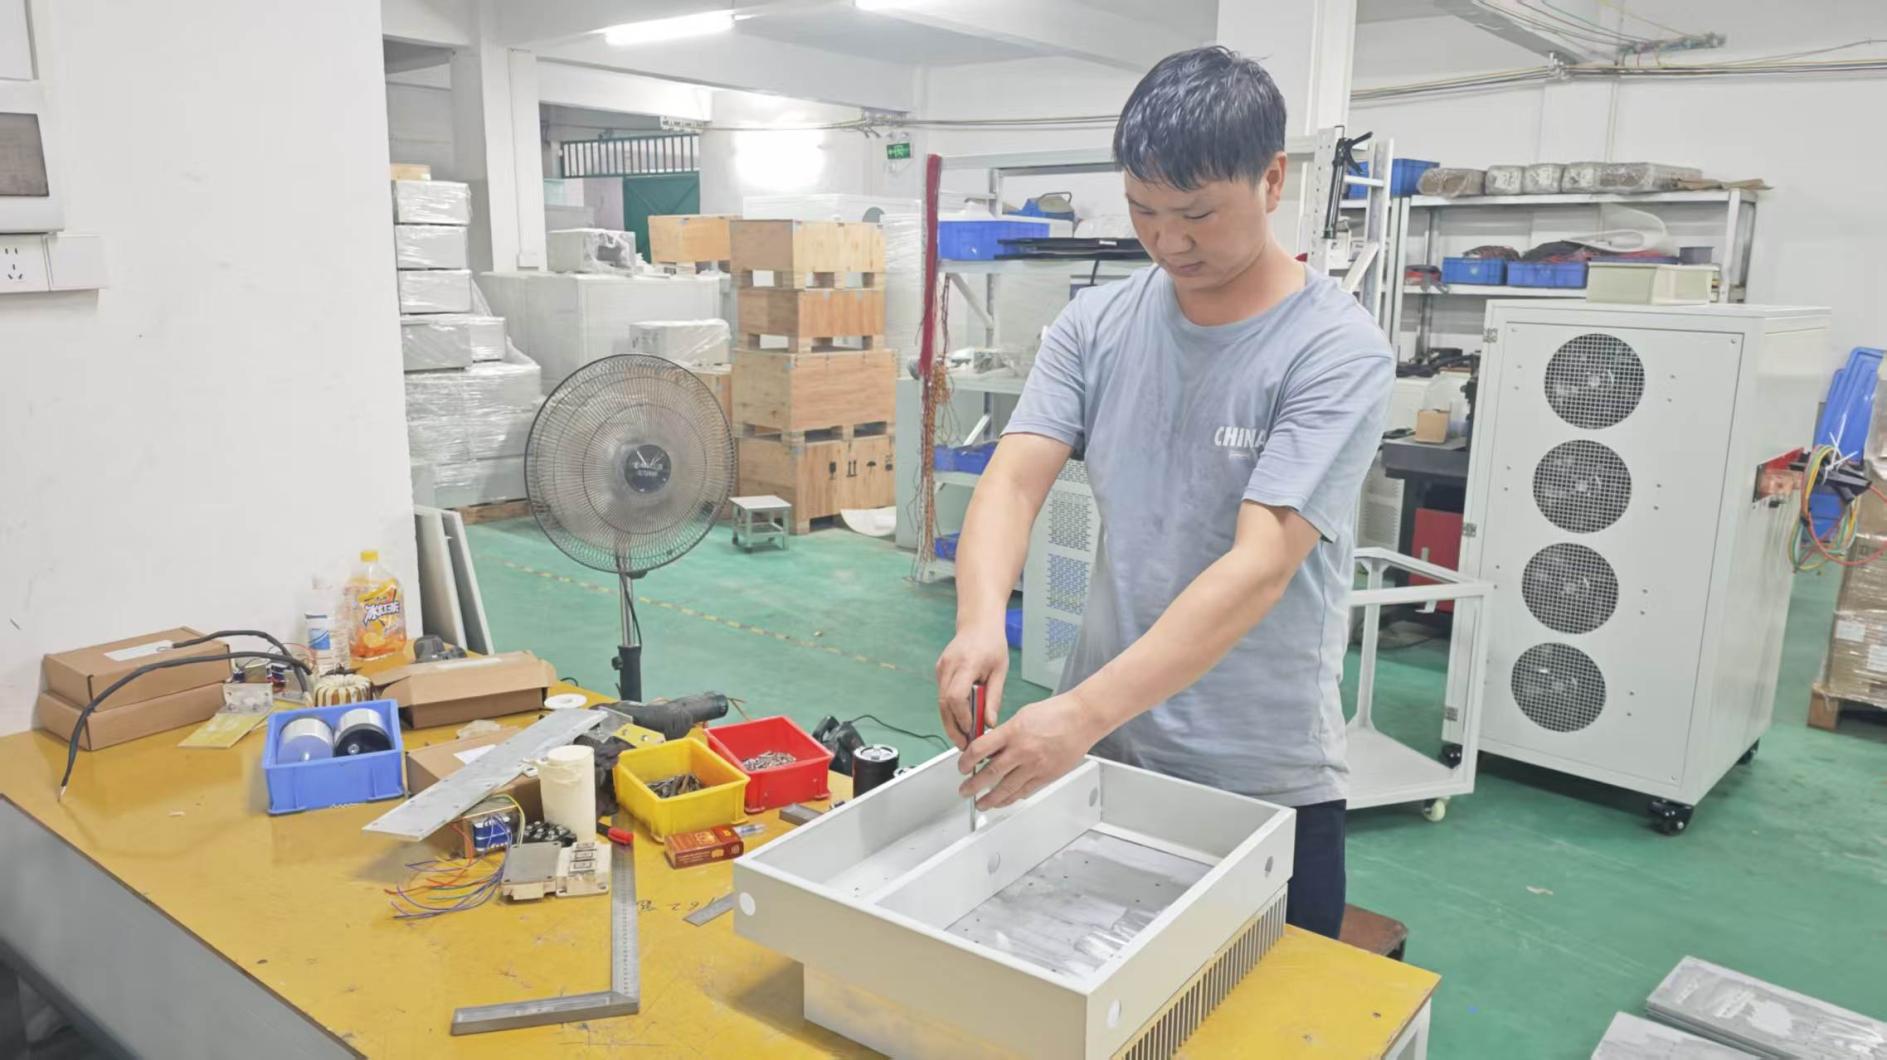 Module Assembly & Wiring
 Full Load Commissioning
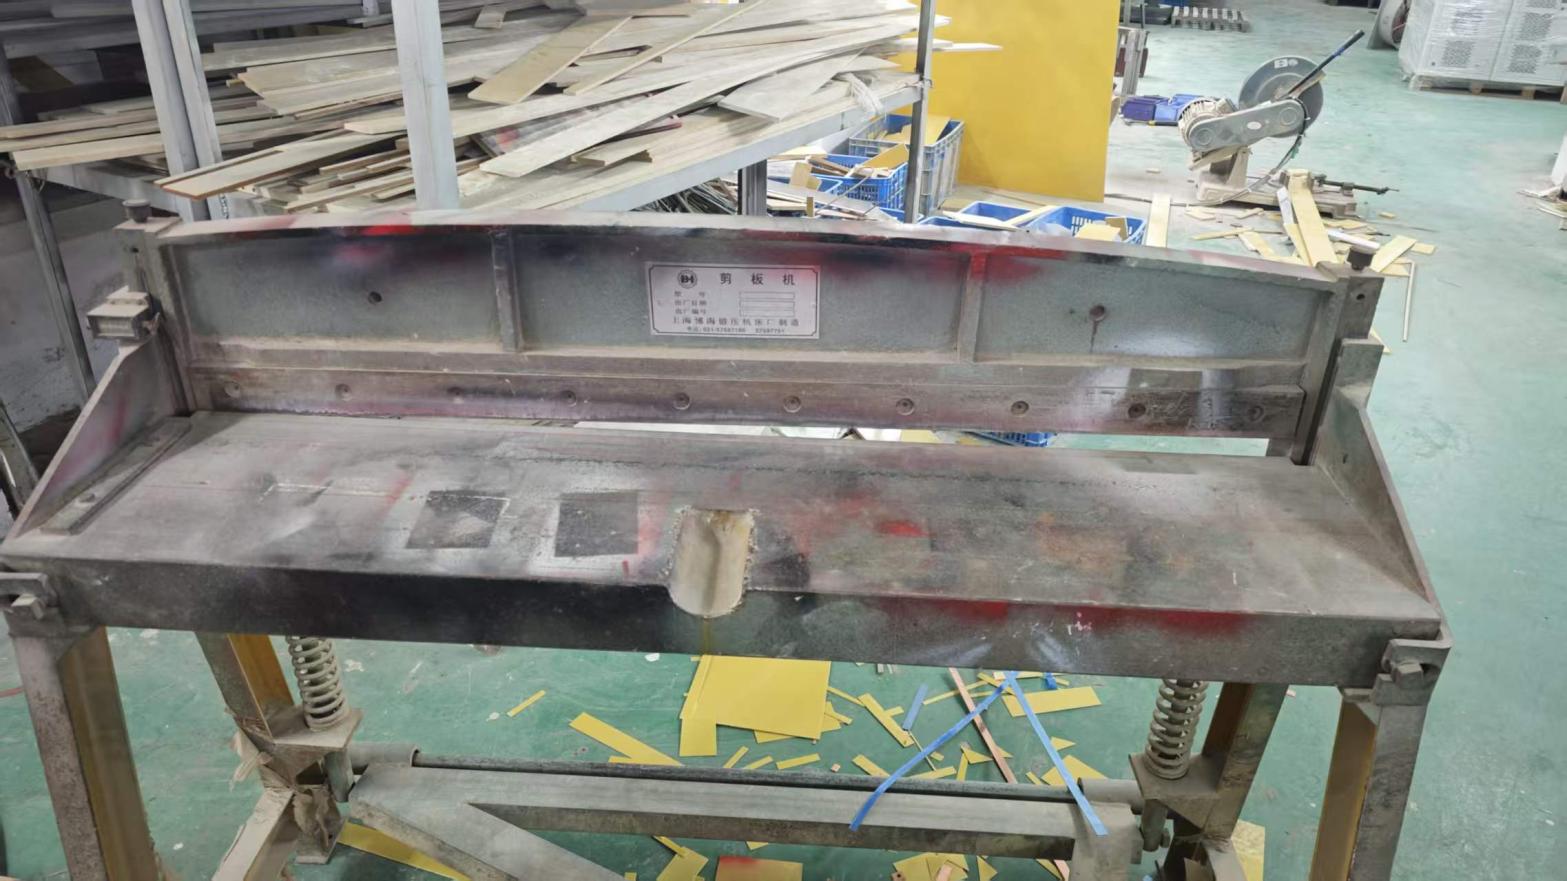 In-House Sheet Metal Shearing
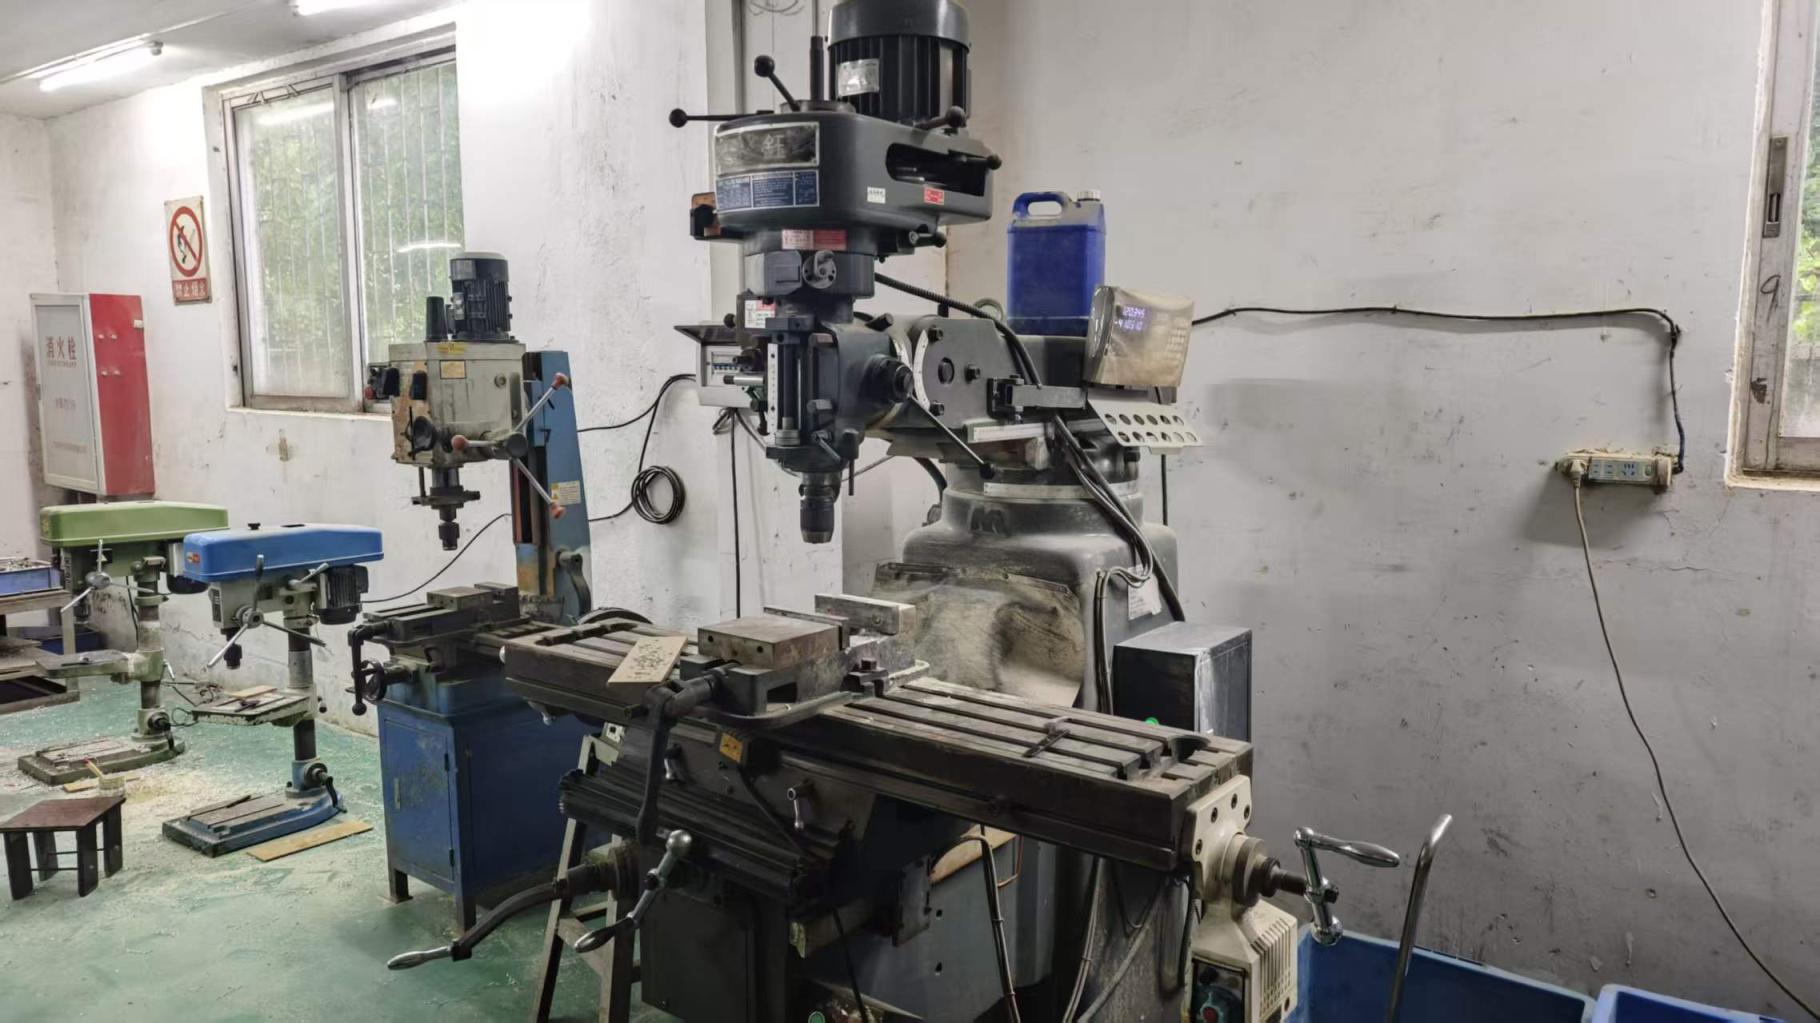 Heavy Copper Busbar Milling
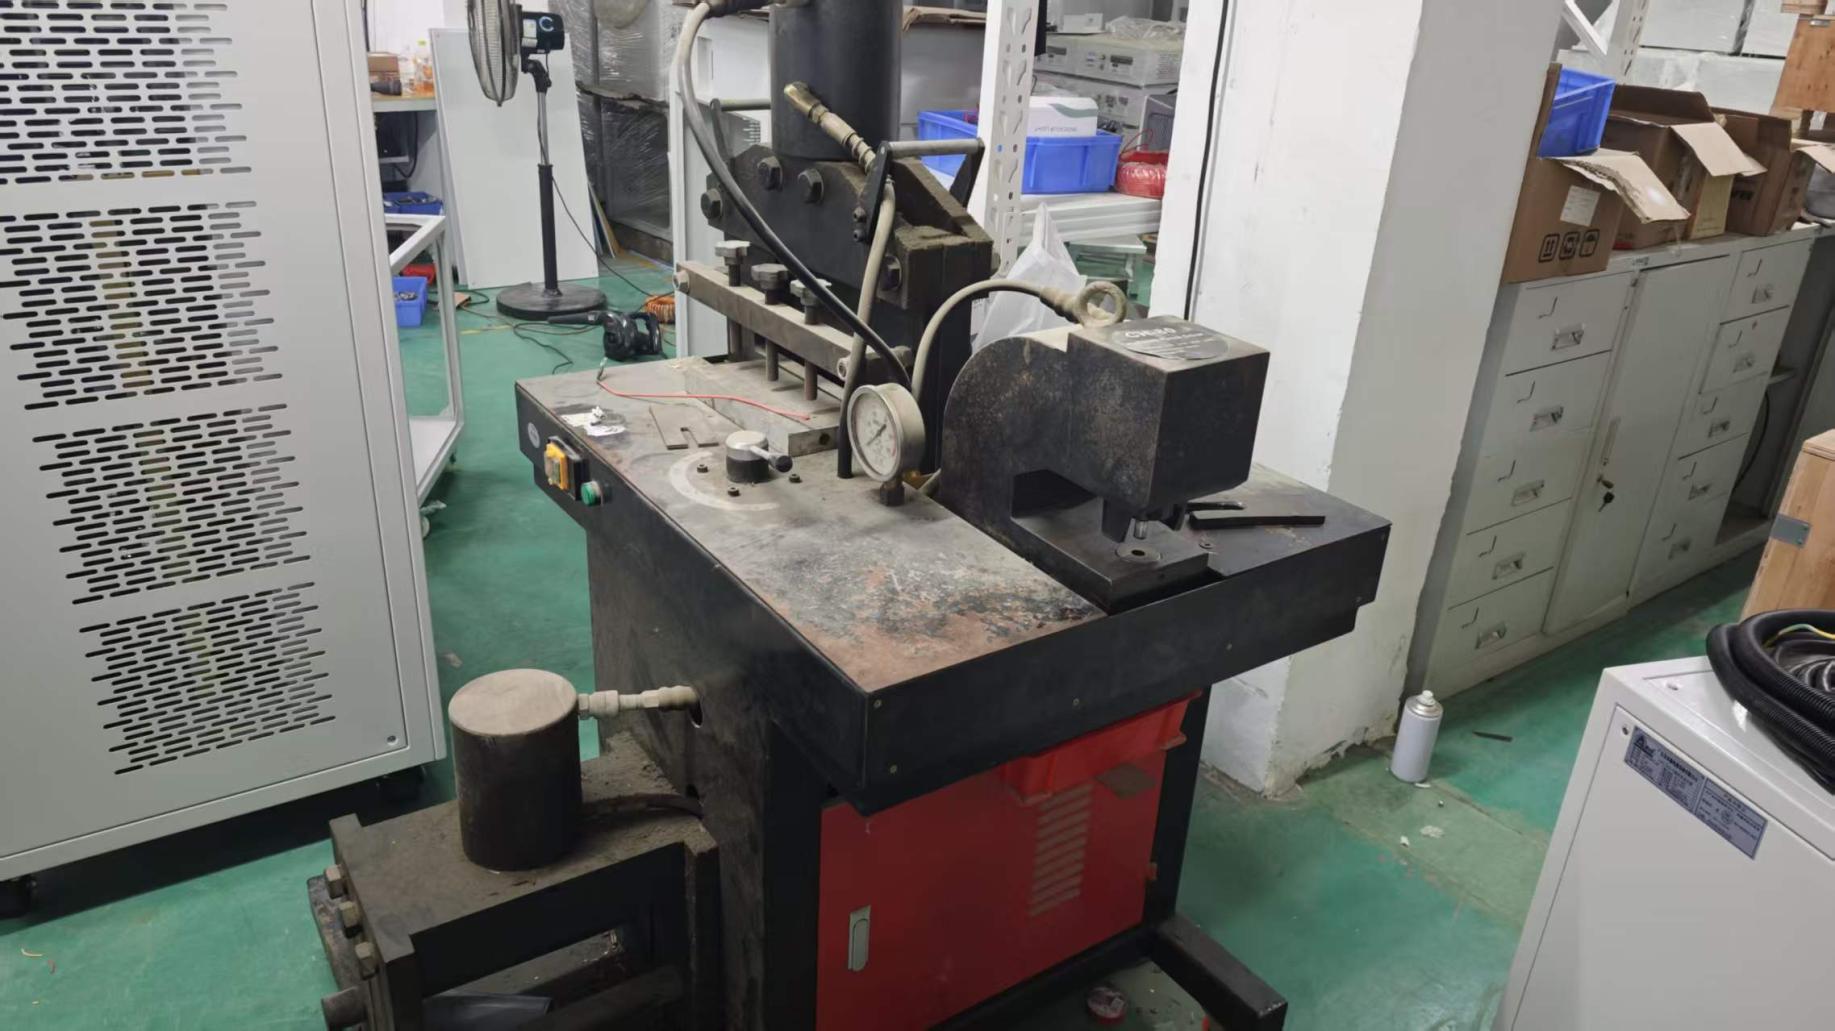 Precision CNC Punching
 Oscilloscope Waveform Verification
Founded in 2013, Guangdong Fenvix Technology Co., Ltd. operates a specialized 3,000 m² engineering and manufacturing facility in Guangdong, China. Unlike trading entities, Fenvix maintains complete control over mechanical chassis fabrication, heavy copper busbar preparation, magnetic component winding, SMD control electronics assembly, and high-power thermal burn-in protocols. Our on-site manufacturing infrastructure includes plate shearing machines, CNC punching stations, milling, drilling, and tapping equipment, ensuring that all structural cabinets and busbar assemblies meet rigorous geometric and thermal conductivity tolerances.
Certified under the ISO 9001 Quality Management System and verified on-site by TÜV Rheinland, our processes enforce strict quality gates from raw semiconductor inspection to finished-cabinet full-load testing. Our units hold CE conformity, adhering strictly to EU Low Voltage Directive (LVD) and Electromagnetic Compatibility (EMC) regulations. We partner with plant engineers, electrochemical process specialists, and system integrators across Eastern Europe, offering zero-MOQ flexibility for single-unit replacement retrofits, full plant line designs, and high-volume OEM/ODM cabinet branding.
Direct answers to engineering parameters, electrical compliance, integration protocols, and logistics for industrial procurement teams in Slovakia.
Consult with our senior power electronics engineering team. Receive comprehensive sizing recommendations, technical schematics, and competitive factory-direct quotations within 24 business hours.