Recommended Metal Finishing Power Supply Systems
Engineered for high-duty continuous operation across Romanian manufacturing hubs—from Mioveni automotive lines to Brașov aerospace facilities. High electrical efficiency, ultra-low ripple, and full SCADA automation.

12V/15V 5000A–6000A 75kW Water-Cooled Plating Rectifier
- Output: 0–15V / 0–6000A DC
- Cooling: Deionized Liquid Cooling
- Control: CC / CV Digital Display
- Efficiency: ≥ 90% (IGBT Inverter)

12V 4000A 48kW High-Frequency Switch-Mode Rectifier
- Output: 12V DC / 4000A Continuous
- Ripple: ≤ 2% RMS (Full Load)
- Topology: Full-Bridge Phase Shift
- Target: Zinc, Nickel, Copper Lines

8000A 12V Water-Cooled Galvanizing & Chrome Rectifier
- Capacity: 96kW High-Current Module
- Enclosure: Sealed IP54 Anti-Acid
- Protection: Thermal, Phase-Loss, Short
- Use: Structural Steel Galvanizing

100A–3000A Anodic Oxidation Pulse & DC Power Unit
- Range: 12V–24V / 100A–3000A
- Ramping: Multi-Step Programmable
- Interface: RS485 / Modbus RTU
- Application: Hard Coat & Architectural
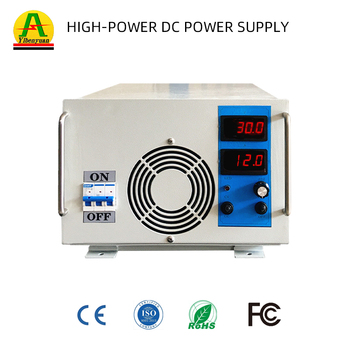
Titanium Alloy Anodizing Power Supply 150V 50A
- Output: 0–150V DC / 0–50A
- Mode: Ultra-Precise Constant Current
- Standard: AMS 2469 / MIL-A-8625
- Application: Aviation Fasteners & Medical

5000W Precision Electrophoresis (E-Coat) DC Unit
- Output: 0–250V / 0–20A Stable DC
- Stability: ≤ 0.5% Voltage Drift
- Soft Start: 0–600s Linear Ramping
- Industry: Automotive Cathodic Primer

48V 625A 30kW Polarity-Reversing DC Power System
- Switching: Integrated H-Bridge Inverter
- Timing: Multi-Segment Period Setting
- Cycle: Millisecond Polarity Flip
- Application: Electro-Etching, Descaling

300kW 20V 15,000A Heavy-Duty Electrolysis Rectifier
- Power: 300kW Constant Operating
- Busbar: T2 High-Purity Solid Copper
- Cooling: Internal Water-Water Heat Ex
- Use: Smelting, Strip Plating, Cladding
Localized Applications in Romania's Manufacturing Landscape
Romania represents Eastern Europe’s most dynamic manufacturing hub. Our industrial metal finishing power supplies are engineered specifically to overcome regional grid fluctuations and satisfy demanding OEM supply chains.
Surface finishing in Romania has moved decisively beyond conventional manual electroplating. Today, Tier-1 automotive integrators, aerospace subcontractors, and metal fabricators operating in regions like Argeș, Dolj, Brașov, Timiș, and Prahova require digitalized, closed-loop electro-chemical control. A variable DC rectifier is no longer merely a basic transformer; it is the fundamental determinant of coating thickness uniformity, corrosion resistance, molecular micro-hardness, and energy expenditure.
Automotive Corridor (Pitești – Craiova – Timișoara)
Driven by Automobile Dacia (Renault Group) in Mioveni and Ford Otosan in Craiova, local component coaters require multi-stage programmable rectifiers for Zinc-Nickel (Zn-Ni) alloy electroplating and cathodic electrophoretic deposition (KTL/E-Coat). Our units provide ripple under 2%, preventing pinholes and ensuring 720+ hours of neutral salt spray (NSS) corrosion resistance.
Aerospace & Defense Hub (Brașov & Bacău)
Subcontractors serving major commercial airframes around Ghimbav and Bacău operate strictly under AS9100 and NADCAP standards. Fenvix constant-current anodizing rectifiers provide specialized ramp-voltage control for Tartaric-Sulfuric Acid (TSA), Chromic Acid (CAA), and Titanium Alloy Hard Anodizing without heat shock or structural embrittlement.
Electronics & Precision PCB (Cluj & Arad)
Continuous reel-to-reel plating lines and high-density interconnect (HDI) PCB manufacturing across Transylvania require high-frequency pulse rectifiers for selective gold (Au), palladium (Pd), and micro-hole copper filling. Fenvix units offer microsecond response times that virtually eliminate edge over-plating.
Continuous Strip Galvanizing (Galați & Hunedoara)
Heavy metallurgy plants along the Danube and Western industrial clusters demand ultra-high amperage (up to 15,000A) continuous DC units. Heavy busbar engineering, double-inverter redundancy, and internal deionized closed-loop water cooling safeguard the power stages against corrosive chemical vapors.
Eco-Friendly Wastewater Treatment (Industrial Parks)
Romanian environmental enforcement (Garda Națională de Mediu) requires galvanic plants to clean process effluent. Our automated polarity-reversing DC power supplies support electro-coagulation and electro-dialysis without anode passivation, dropping heavy metal sludge volumes drastically.
Industrial Trends Shaping Romanian Metal Finishing
Strategic modernization across the Romanian finishing industry is driven by stringent EU green directives, rising industrial energy costs, and the mandate for end-to-end traceablity.
Electroplaters across Romania face structural transformation. Traditional thyristor (SCR) rectifiers, which have served workshops for decades, are being phased out rapidly under European Union climate mandates and market competition. As Romanian factories modernize their plating shops, four dominant market and technological drivers have emerged:
1. The Phase-Out of SCR/Thyristors: Shift to High-Frequency Switch Mode (SMPS)
Legacy Silicon-Controlled Rectifiers (SCR) operating at line frequencies (50Hz) are notoriously inefficient. Operating at 65% to 75% system efficiency with lagging power factors (0.65–0.78), they generate immense reactive power penalties from Romanian grid operators such as Electrica, Enel, or Transelectrica. Fenvix IGBT-based high-frequency rectifiers switch at frequencies between 20kHz and 50kHz, delivering overall conversion efficiencies exceeding 92% and a near-unity power factor (>0.95). In high-current installations running 24/7 (such as continuous galvanizing or hard chrome plating), this efficiency leap reduces electric utility bills by 18% to 26%, providing full capital expenditure (CapEx) amortisation within 14 months.
2. EU REACH Annex XIV Compliance: Cr(VI) to Cr(III) Transition
The stringent mandate to eliminate toxic hexavalent chromium (Cr6+) in favor of trivalent chromium (Cr3+) represents the most pressing chemistry changeover in Romanian automotive finishing lines. However, trivalent chromium electroplating processes present a much narrower electrochemical window; they are vulnerable to current disruptions and harmonic ripple. Traditional ripple rates of 5%–10% acceptable in Cr6+ produce hazy deposits, burning, and micro-cracking in Cr3+ electrolytes. Fenvix metal finishing rectifiers integrate advanced LC-filtering and phase-staggered PWM topologies to guarantee a strict root-mean-square (RMS) current ripple of ≤ 1% to 2% across the entire 10%–100% load spectrum.
3. Industry 4.0 Integration & Complete Batch Traceability
As multinational Tier-1 manufacturers expand operations in Romania, manual log sheets are being banned from galvanic floors. Finishing lines require real-time transmission of ampere-hours (Ah), dynamic voltage, bath temperatures, and operational alarm data directly into supervisory SCADA or manufacturing execution systems (MES). Our power supplies feature standard galvanically isolated RS485 (Modbus RTU), Siemens Profibus-DP, Profinet, and analog 0–10V / 4–20mA interfaces, facilitating autonomous recipe execution without operator variance.
| Performance Metric | Legacy Thyristor / SCR Rectifier | Standard Commercial SMPS | Fenvix High-Frequency IGBT System |
|---|---|---|---|
| Electrical Efficiency | 68% – 76% (High Thermal Waste) | 84% – 88% | 92% – 95% (Optimized Low-Loss) |
| Output DC Ripple (RMS) | 5% – 12% (Requires Bulky Chokes) | 3% – 5% | ≤ 1% – 2% (Ultra-Smooth Waveform) |
| Power Factor (cos φ) | 0.65 – 0.75 (Reactive Tariffs) | 0.88 – 0.90 | ≥ 0.95 (Eliminates Grid Surcharges) |
| Cabinet Footprint & Weight | Extremely Heavy / Large Volume | Compact Modular | 60% Smaller vs SCR; Crane Not Required |
| Dynamic Response Time | Slow (100–300 ms) | Moderate (10–20 ms) | Sub-Millisecond (< 2 ms Fast Loop) |
| Corrosive Acid Resistance | Open Air Ventilation / Prone to Rot | Standard Varnishing | Sealed Water-Cooled IP54 / Nano-Coated |
Engineering Authority: Fenvix Guangdong Factory
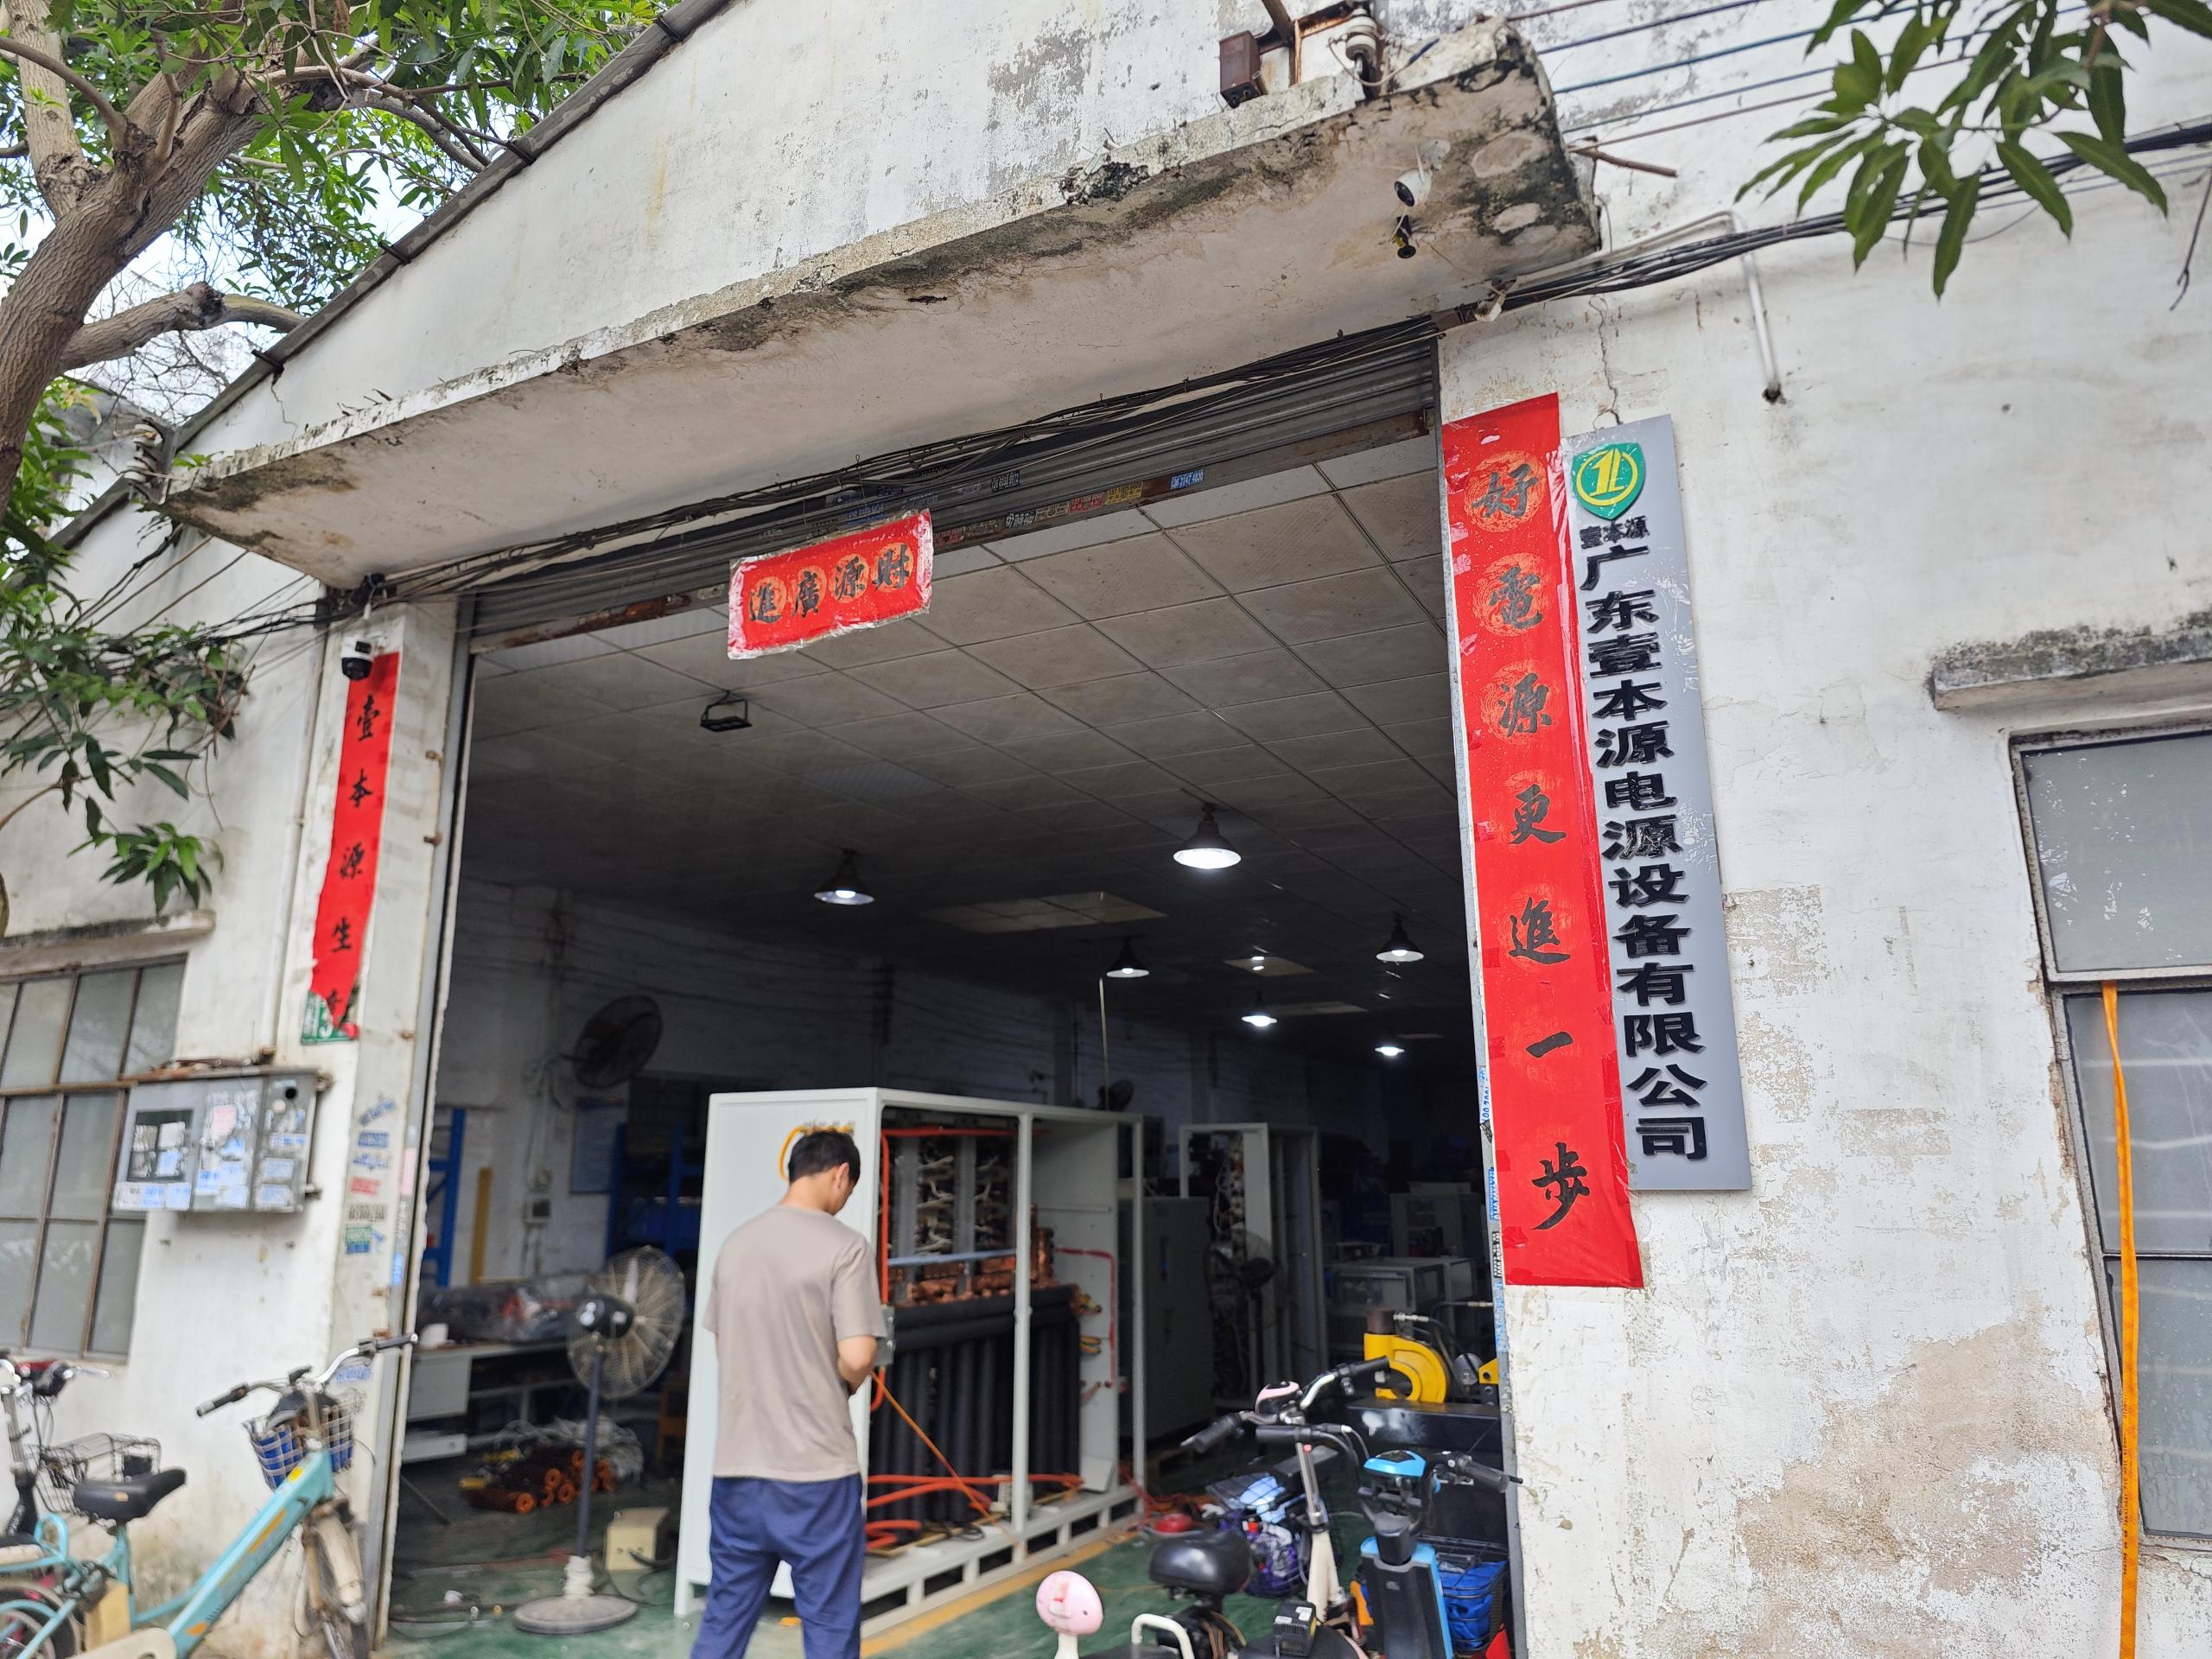
Established in 2013, Guangdong Fenvix Technology Co., Ltd. provides direct manufacturing capability, eliminating broker markups and ensuring customized power architectures delivered directly to Romania.
Complete In-House Mechanical & Electrical Fabrication
Unlike trading companies that outsource chassis assembly and power engineering to external contractors, Fenvix controls every manufacturing phase inside our 3,000m² facility in Guangzhou. From CNC laser plate shearing, automated turret punching, and milling to copper busbar silver-plating, transformer winding, and high-frequency ferrite core assembly, in-house control guarantees mechanical precision and thermal stability.
Rigorous 100% Full-Load Burn-In & Oscilloscope Calibration
Every single power supply destined for Romanian customers undergoes a minimum of 48 hours continuous burn-in testing under simulated full-load conditions inside temperature-controlled chambers. Our test engineers inspect switching waveforms via digital storage oscilloscopes, verifying zero voltage switching (ZVS) performance, peak diode recovery spikes, and thermal equilibrium across cooling channels before packing in fumigated seaworthy wooden cases.
Certified Quality & Global Delivery Safeguards
Our operational management, documentation, and international logistics are engineered to reduce commercial and operational risks for Romanian procurement teams.
ISO 9001:2015
Certified design, manufacturing, and QA processes across our entire plant.
CE & EU Compliance
Complies fully with EN 60146, Low Voltage Directive (LVD) & EMC standards.
TÜV Verified
On-site assessment and capability verification by TÜV Rheinland auditors.
DDP Delivery
Door-to-door customs cleared delivery to Bucharest, Constanța, Cluj, or Timișoara.
No Minimum Order
1-set pilot prototypes and high-volume multi-tank batch production supported.
Frequently Asked Questions for Romanian Procurement Teams
Detailed technical, electrical, and commercial answers compiled by our application engineers specifically for Romanian plant managers and system engineers.