High-Performance Power Rectifiers for Industrial Electrolysis
Engineered for high current density, low residual voltage ripple (≤1%), and non-stop 24/7 reliability in demanding galvanic, metallurgical, chemical, and water-treatment installations.

12V 15V 5000A–6000A 75kW Water-Cooled DC Rectifier
- Output Range:12–15V | 0–6000A
- Cooling Topology:Deionized Water Cooled
- Topology:IGBT Switch-Mode PWM
- Ripple & Cos φ:≤ 1% RMS | PF > 0.94

12V 4000A 48kW CV/CC Industrial Plating Rectifier
- Output Range:0–12V | 0–4000A
- Operation Modes:Constant Voltage / Current
- Cooling:Forced Air / Isolated Duct
- Digital Comms:RS485 Modbus-RTU / PLC

8000A 12V High-Amperage Water-Cooled Rectifier
- Current Output:8000A Continuous
- Busbar Linkage:Direct Silver-Plated Copper
- Protection:Phase Loss, Overheat, Short
- Compliance:CE, EMC, LVD Directive

300kW 20V 15,000A Megawatt Electrolysis Power Unit
- Peak Output:20V DC | 15,000A
- Efficiency:≥ 92.5% at Full Load
- Input Voltage:380V/400V 3-Phase 50Hz
- Cabinet Design:IP54 Sealed Thermal Chamber

48V 625A 30kW Auto-Polarity Reversing Descaling Supply
- Voltage / Current:0–48V | 0–625A
- Polarity Cycle:Programmable 1s–999h
- Applications:Wastewater & Scale Removal
- Interface:4–20mA, 0–10V, RS-485

100A–3000A Variable Anodic Oxidation Power Source
- Voltages:12V / 24V / 60V / 100V
- Ramp Profiles:Stepwise Voltage/Current Ramp
- Target Metals:Aluminum & Titanium Alloys
- Control Stability:< 0.5% Drift across 24h
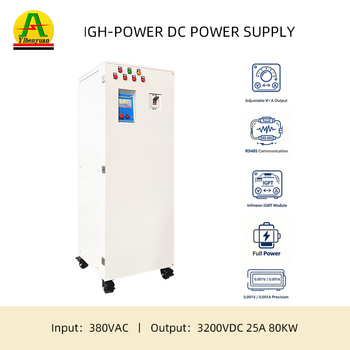
80kW 1000V–3200V High-Precision Programmable HV Source
- Voltage Rating:Up to 3200V DC Regulated
- Regulation Speed:< 5ms Dynamic Response
- Target Fields:Capacitor Bank / Insulation Test
- Display:7-inch Industrial HMI Touch
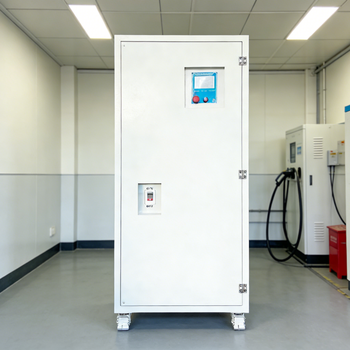
160kW 2500A High-Current Heavy Electrolysis Rectifier
- Rated Power:160kW Continuous Output
- Current Setting:0–2500A Infinitely Adjustable
- Thermal Protection:Direct Heat-Sink Sensor Trip
- Cooling Options:Forced Water / Air Intercool
High-Frequency Switch-Mode (IGBT) vs. Legacy SCR Rectifiers
Why modern industrial electrolysis facilities in Europe are retiring line-commutated silicon-controlled rectifiers (SCR) in favor of high-frequency pulse-width modulated (PWM) IGBT architectures.
The Thermodynamic and Electrochemical Imperative
Electrolytic processes—including continuous chlor-alkali splitting, copper electrowinning, industrial hard-chrome deposition, and water electrolysis for green hydrogen—are intensely energy-demanding. In an electro-chemical cell, power dissipated through parasitic ac-ripple does zero productive work: it generates unwanted Joule heating, accelerates cathode degradation, damages protective catalyst coatings, and increases consumption of electrolyte additives.
Traditional thyristor (SCR) rectifiers operate at fundamental grid frequencies (50Hz in Bulgaria). To smooth output current, massive multi-ton inductive choke filters are required. Even with filtration, residual ripple typically hovers between 5% and 12%, resulting in uneven deposition thickness and excessive heat accumulation in electrolyte baths.
Fenvix High-Frequency Advantage: By switching at 20 kHz to 50 kHz using high-voltage insulated gate bipolar transistors (IGBT), our rectifiers reduce current ripple below 1% RMS while cutting cabinet footprint by 60% and improving overall conversion efficiency up to 94%.
In addition, the high input displacement power factor (cos φ > 0.94) eliminates penalties from transmission system operators (such as ESO Bulgaria) for reactive power absorption, directly cutting overall facility operational expenditures (OPEX).
| Performance Metric | Fenvix IGBT Switch-Mode | Conventional Thyristor (SCR) |
|---|---|---|
| Electrical Conversion Efficiency | 91% – 95% | 78% – 84% |
| Current Output Ripple (RMS) | ≤ 1.0% Across Range | 5.0% – 12.0% |
| Input Power Factor (cos φ) | ≥ 0.94 without capacitors | 0.65 – 0.82 (Varies with phase angle) |
| Step-Response Speed | < 5 ms (Millisecond level) | 200 – 500 ms |
| Equipment Weight & Volume | Compact modular (1/3 volume) | Extremely heavy oil/air transformer |
| Electrode Longevity | Prolonged (minimal micro-arcing) | Shortened by low-frequency pulses |
Electrochemical Applications Across Ruse’s Industrial Infrastructure
As Bulgaria's primary inland port on the Danube river, Ruse serves as a strategic crossroads of chemical processing, metallurgy, mechanical engineering, and waterborne freight.
Chemical Clusters & Chlor-Alkali Operations
The chemical manufacturing belt along the Danube in Northern Bulgaria relies on continuous electrolysis for chlorine, caustic soda, and hypochlorite synthesis. Our modular water-cooled DC rectifiers provide isolated, non-stop constant-current supplies that endure aggressive corrosive atmospheres, ensuring process uptime in Free Zone Ruse and East Industrial Park installations.
Danube Shipyards & Vessel Maintenance
Shipbuilding, barge repair facilities, and marine engineering workshops on the Ruse waterfront require robust galvanic rectifiers for sacrificial zinc anode testing, hull hard-chrome restoration, and shaft electropolishing. Fenvix units offer heavy-duty IP54 enclosed chassis resistant to riverside humidity and condensation.
Automotive Components & Surface Treatment
Ruse’s precision machine parts and automotive tier-suppliers operate automated electro-galvanizing, nickel-plating, and hard anodizing lines. Constant-current stability within ±0.5% guarantees absolute coating uniformity, strict micrometric tolerance adherence, and zero burn marks on complex geometries.
Electrolytic Water Treatment & Descaling
With high carbonate hardness in regional Danube groundwater and stringent EU industrial discharge regulations, closed-loop treatment plants utilize Fenvix 48V auto-polarity-reversing DC power supplies. Automated polarity cycle timers eliminate manual cathode descaling downtime and minimize chemical additive usage.
Green Hydrogen Electrolyzer Pilots
As Northern Bulgaria accelerates clean energy initiatives linked with cross-border Romania-Bulgaria logistics, pilot PEM and alkaline water electrolyzers require low-harmonic, dynamic-response DC sources capable of tracking fluctuating solar and wind renewable inputs without inducing thermal degradation in catalyst membranes.
Emerging Procurement Trends in Ruse’s Electrochemical Sector
A roadmap of technology shifts shaping procurement priorities for Northern Bulgarian engineers and plant directors.
EU Green Deal & Energy Auditing
Surging European electricity prices place conversion efficiency at the center of procurement. Transitioning from 80% SCR rectifiers to 94% Fenvix IGBT units yields a complete capital payback within 14–18 months in continuous 24/7 electrolysis operations.
SCADA Integration via Profibus / Modbus
Modern automated factories in Ruse eliminate manual dial adjustments. Fenvix systems come standard with galvanically isolated RS-485 interfaces supporting Modbus-RTU, Profibus-DP, and 4–20 mA remote feedback to integrate seamlessly with Siemens and Schneider plant SCADA systems.
Harsh Environment Water-Cooled Enclosures
Open-air fan cooling draws airborne acid mist, humidity, and conductive particulates into cabinet electronics. Ruse electroplating workshops increasingly mandate completely sealed water-cooled IP54 cabinets that isolate high-voltage power components from contaminated shop atmospheres.
Modular Redundancy & Rapid Field Repair
Unplanned downtime in continuous plating or chemical extraction halts entire supply chains. Fenvix power stages utilize parallel slide-in IGBT power blocks. If one block requires service, the unit continues operating at derated capacity without complete shutdown.
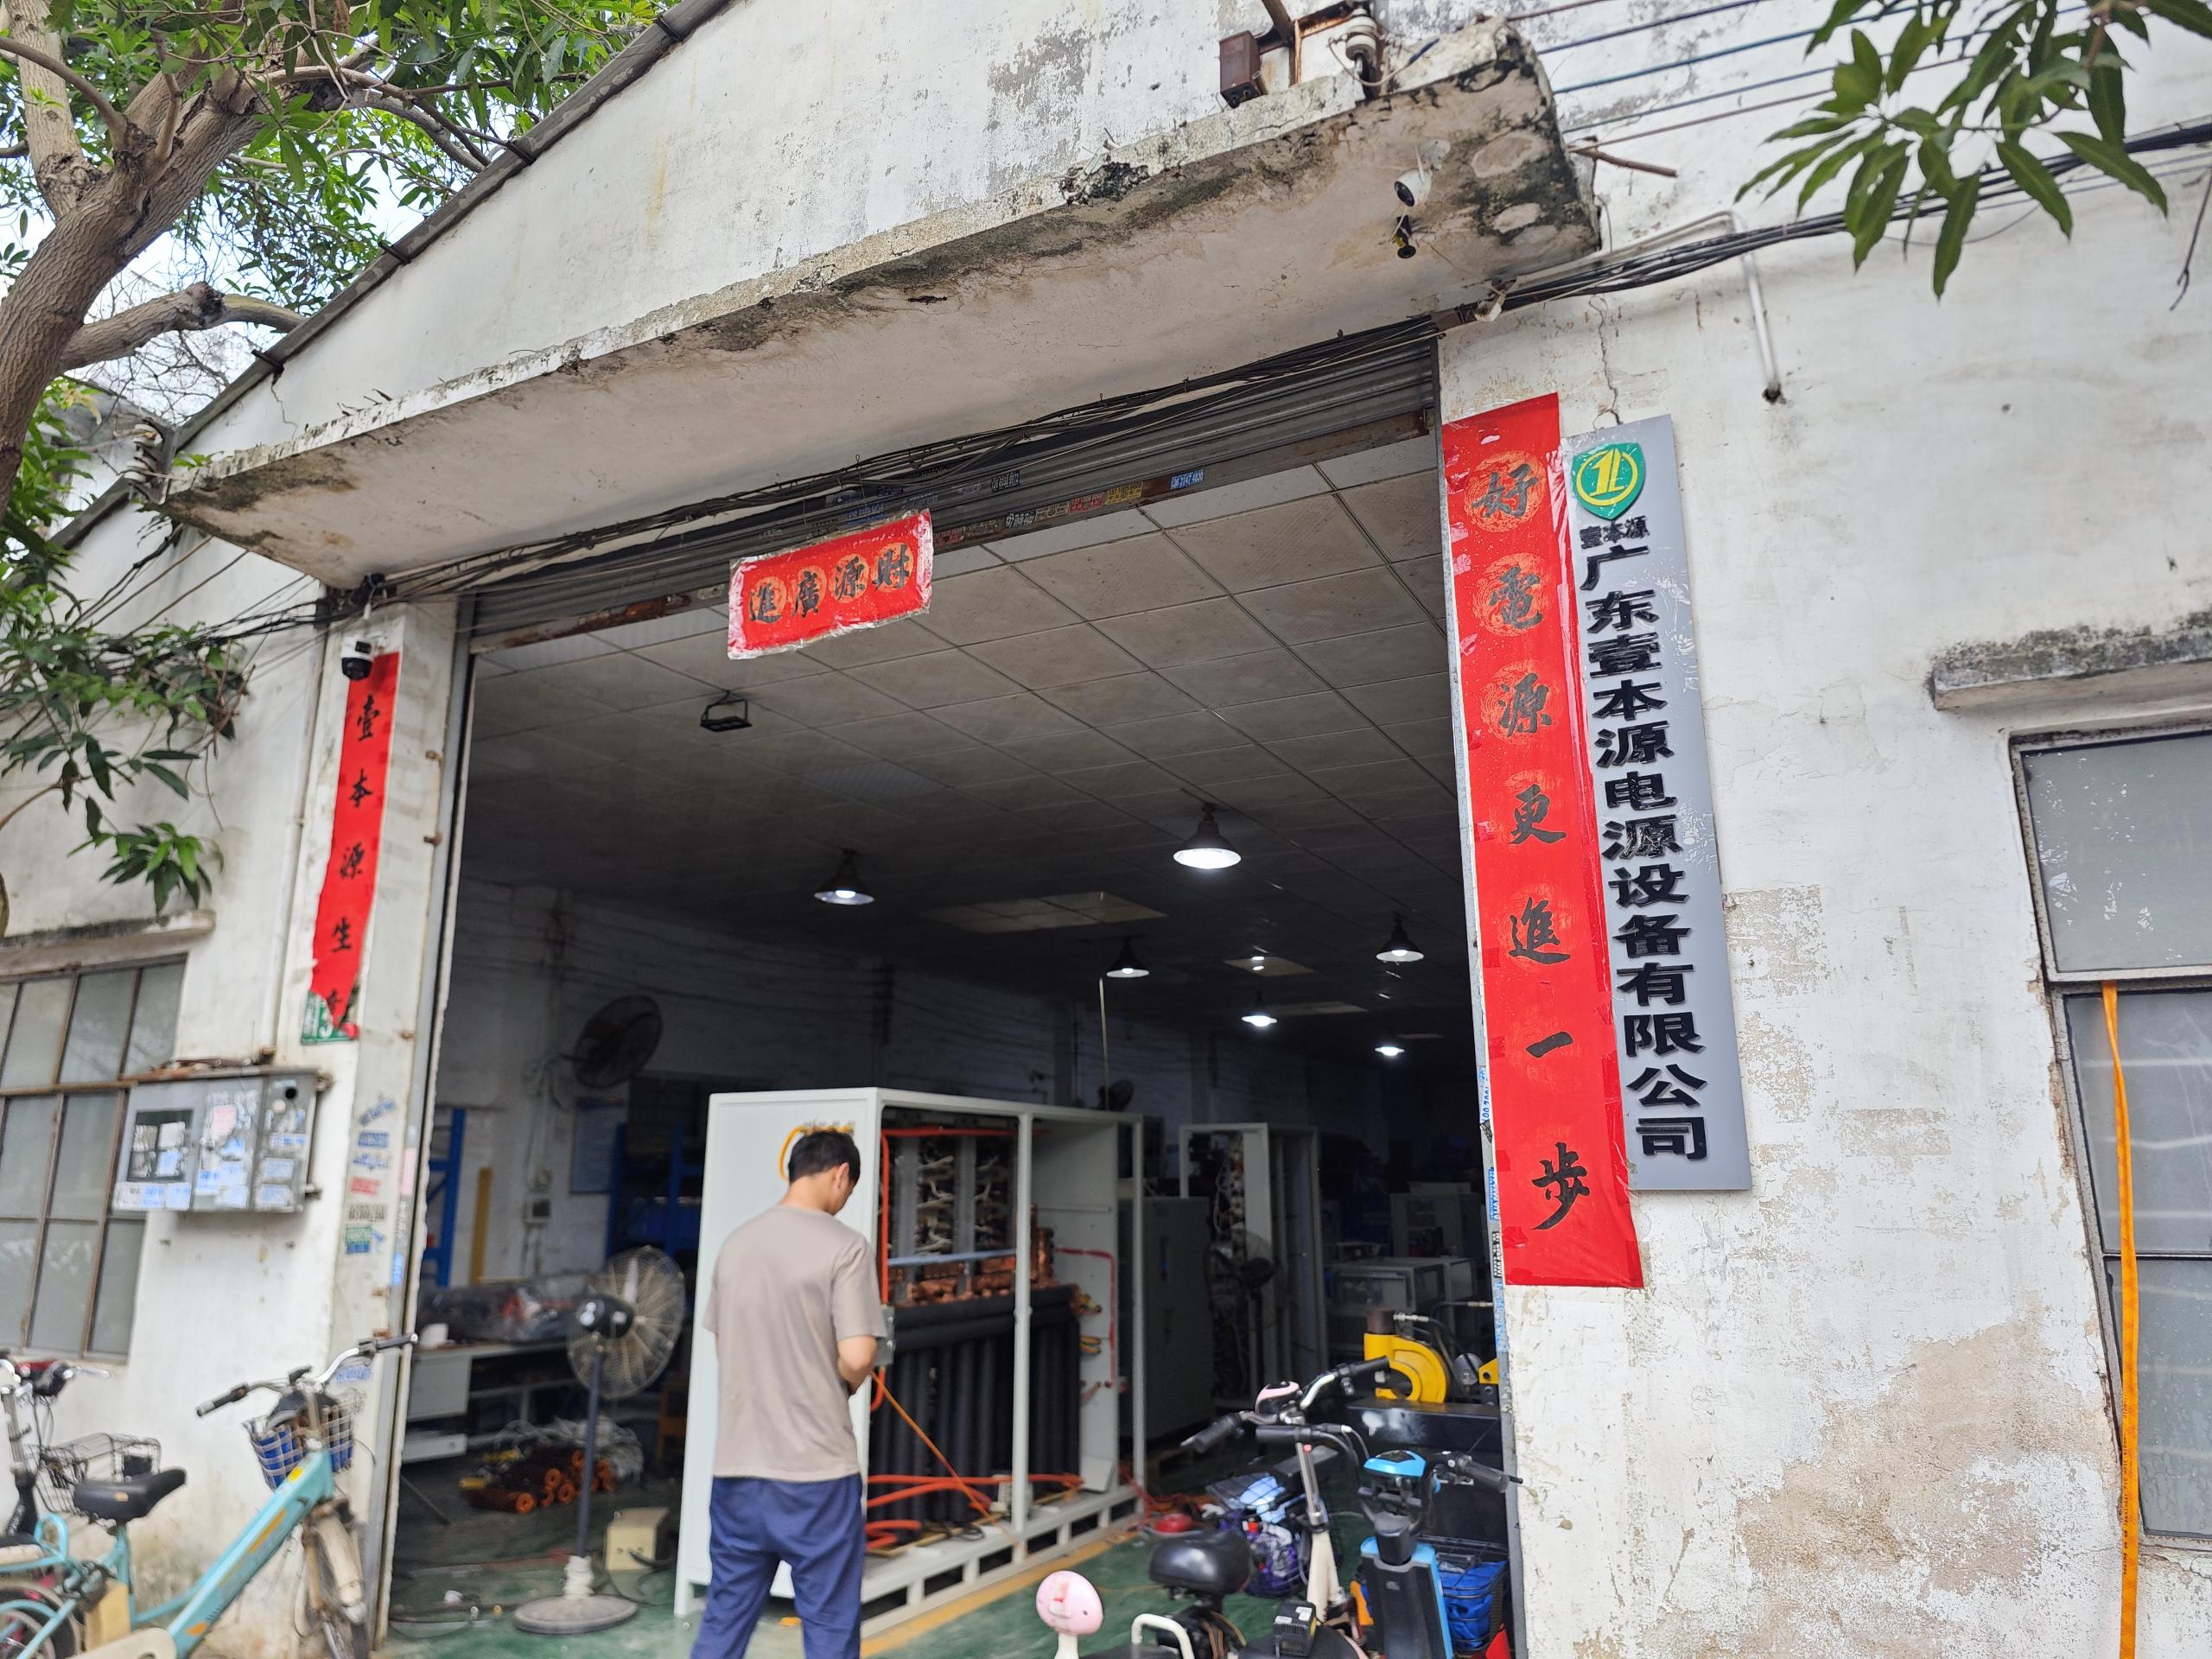
Direct Manufacturing Strength: Guangdong Fenvix Technology
Operating a dedicated 3,000m² facility since 2013, Fenvix controls every phase of design, laser plate shearing, busbar machining, winding, assembly, and full-load burn-in testing.



No Trading Middlemen: Direct Factory OEM/ODM Execution
For industrial buyers in Ruse, dealing directly with an authentic manufacturer ensures that custom mechanical busbar offsets, specialized tank voltage requirements (e.g., non-standard 15V, 28V, or 64V outputs), and specific cooling water connections (BSP, NPT, or flanged) are incorporated directly at the drafting table.
Every single power unit undergoes a rigorous 24-hour full-load thermal burn-in before release. Oscilloscope testing validates residual ac-ripple, step-response timing, and soft-start ramp precision, verified under ISO 9001 quality management procedures and on-site audit verification by TÜV Rheinland.
International Compliance & European Standards
All Fenvix electrolysis and plating power supplies shipped to Bulgaria and the European Union adhere strictly to the European Low Voltage Directive (LVD 2014/35/EU), Electromagnetic Compatibility Directive (EMC 2014/30/EU), and RoHS hazardous materials directives. Test reports and Declarations of Conformity accompany all export orders.
Whether for single-unit pilot lines or plant-wide expansions with multiple 15,000A cells, Fenvix offers transparent EXW, FOB, CIF (via Port of Varna or Constanța), and DDP delivery terms directly to the Ruse destination.
Frequently Asked Questions for Ruse & Bulgarian Industrial Buyers
Comprehensive answers covering grid compatibility, thermal cooling, logistics routes, and technical interfacing.
Are Fenvix power supplies directly compatible with Bulgaria’s 400V 50Hz grid?
How does the Danube valley climate impact water cooling vs. air cooling selection?
What are the optimal shipping routes and transit times to Ruse, Bulgaria?
Can our engineering team integrate the rectifier with an existing Siemens S7 PLC?
What is the minimum order quantity (MOQ) and warranty support policy?
How do Fenvix units comply with EU harmonic emissions standards (EN 61000)?
Modernize Your Electrochemical Cells in Ruse Today
Consult with Fenvix power engineers to size your custom electrolysis rectifier. Receive a detailed electrical calculation sheet, custom cabinet CAD footprint, and transparent CIF/DDP delivery quotation within one business day.