Water Cooled

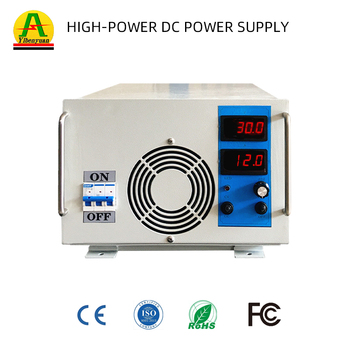
12V 15V 5000A 6000A 75KW Rectifier
- Rated Power: 75 kW Module
- Output Range: 12V–15V / 6000A
- Control Modes: CV / CC Digital
- Cooling System: Closed-Loop Water
From continuous barrel zinc plating in local hardware manufacturing to heavy-duty hard chrome and electro-copper deposition, explore our verified switched-mode power supplies engineered with high-frequency IGBT modules and hermetic cooling architecture.






Technical adaptation parameters addressing grid stabilization, corrosion resistance, and specific manufacturing verticals across Kumanovo's evolving metalworking ecosystems.
The municipality of Kumanovo, representing the economic epicenter of North Macedonia's Northeastern Statistical Region, retains a prominent legacy in structural metallurgy, welded pipe fabrication, automotive mechanical components, and hardware construction. In recent industrial modernizations across areas such as the Noviny Industrial Zone and surrounding manufacturing estates along the Corridor X highway, operators have faced mounting performance bottlenecks rooted in obsolete silicon-controlled rectifier (SCR) and legacy thyristor equipment.
Operating legacy oil-cooled or bulky transformer-based rectifiers in contemporary Kumanovo plating lines incurs prohibitive electrical draw, high harmonic distortion back into the regional utility grid (EVN Macedonia), and high current ripple factor (often exceeding 5% to 8%). For advanced zinc passivation, decorative copper-nickel-chrome finishes, or technical hard anodizing on automotive cast components, excessive current ripple induces severe macroscopic defects: including micro-pitting, uneven crystal nucleation, coarse grain boundary deposits, and erratic plate thicknesses. Our high-frequency switch-mode power supplies (SMPS) deployed in Kumanovo resolve these limitations by converting the 400V 50Hz three-phase supply through rapid IGBT switching networks operating at 20 kHz to 40 kHz, suppressing output ripple to below 2% across the full dynamic load envelope.
Kumanovo's proximity to Skopje and cross-border transport nodes positions local tier-2 and tier-3 component finishers to supply automotive sub-assemblies. Our rectifiers provide high-precision constant current (CC) control vital for zinc-nickel alloy plating, ensuring strict salt-spray corrosion resistance (>720 hours to white rust) required by European OEMs.
Suburban industrial zones around Kumanovo frequently experience localized voltage sags during peak industrial periods. Fenvix units incorporate wide AC input tolerances (400V ± 15%) coupled with integrated active power factor correction (PFC ≥ 0.95), safeguarding delicate control electronics from power drops without tripping line breakers.
Plating workshops dealing with hydrochloric pickling, cyanide baths, or high-temperature sulfuric acid anodizing produce highly corrosive aerosols. Fenvix integrates conformal three-coat PCB varnishing, isolated air channels, and optional water-cooled IP54 stainless-steel cabinets that eliminate external air intake entirely.
Assessing the strategic transition from legacy transformer infrastructure toward energy-efficient, closed-loop automated electrodeposition in North Macedonia.
The manufacturing sector across North Macedonia is currently navigating critical economic alignments driven by the EU Carbon Border Adjustment Mechanism (CBAM) and regional clean-air mandates. As surface treatment operations in Kumanovo prepare for integration with European supply chains, plant managers are phasing out inefficient electrical hardware that inflates operating costs.
A conventional 5000A thyristor (SCR) rectifier operating in a continuous galvanizing plant averages 70% to 75% efficiency under typical bath voltages, converting substantial energy directly into waste heat that places additional demands on workshop chillers. By contrast, Fenvix high-frequency switched-mode DC power supplies utilize advanced zero-voltage switching (ZVS) topologies achieving electrical efficiency greater than 90% across broad operational load envelopes.
Furthermore, local plating enterprises are shifting away from manual control knobs toward smart automated lines. Standardized industrial bus integration—specifically isolated RS485 Modbus, Profibus, and 4–20mA/0–10V analog interfacing—allows plating shops in Kumanovo to synchronize real-time current density profiles directly with SCADA systems, hoist arms, and dosing pumps.
| Evaluation Parameter | Legacy SCR / Thyristor Rectifier | Fenvix Switched-Mode (SMPS) IGBT | Direct Strategic Impact for Kumanovo Plants |
|---|---|---|---|
| Operating Efficiency | 68% – 76% (High thermal loss) | 90% – 93% Typical | Reduces monthly utility costs by 18% to 25% under 24/7 continuous operation. |
| Current Ripple Factor | 5% to >8% at partial load settings | ≤ 2% Full Dynamic Range | Eliminates micro-cracking and burning; accelerates electrodeposition rate by 15%. |
| Physical Footprint & Weight | Large, heavy footprint (>800 kg per 5kA unit) | Ultra-compact cabinet (<200 kg modular) | Allows mounting directly adjacent to plating tanks, shortening expensive copper busbar runs. |
| Automation Protocol | Manual potentiometers; crude 0–10V analog | Isolated RS485 / Modbus RTU / PLC Digital | Enables complete automation, remote amp-hour chemical replenishment, and datalogging. |
| Cooling Flexibility | Corrosive ambient air pull or heavy oil bath | Hermetic closed water circuit or isolated air tunnel | Protects semiconductor power stages against corrosive chemical mist and ambient factory dust. |
Direct factory production, rigorous QA standards, and proven engineering capabilities behind our international supply operations.
Guangdong Fenvix operates a strictly monitored ISO 9001 certified manufacturing facility in Guangzhou, China. Our facilities, workforce, and trade operations have been independently audited on-site by TÜV Rheinland.
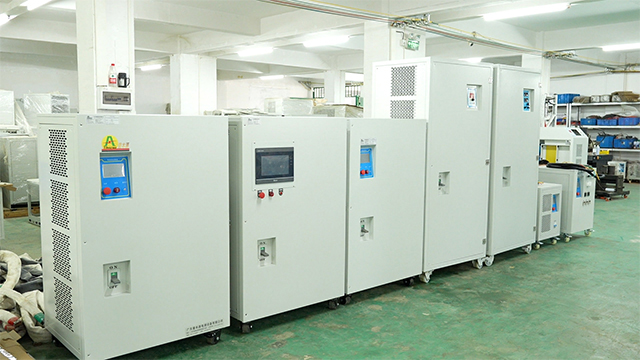
Unlike assemblers relying on third-party subcontractors, our 3,000m² manufacturing plant performs in-house plate shearing, punching, milling, drilling, and high-purity T2 copper busbar forming to ensure structural and thermal integrity.
We support specialty prototype lines, custom pilot tanks, and educational laboratory benches with a strict 1-unit MOQ policy, scaling directly to complete multi-megawatt electroplating rectifying lines without penalty.
Every power supply undergoes thorough full-load burn-in testing, oscilloscope waveform checks, insulation resistance verification, and high-voltage breakdown evaluations prior to export packaging.
We support versatile export documentation and delivery modes for European buyers, accommodating EXW, FOB, CIF (Thessaloniki or Durrës ports), and multimodal inland container transit to Kumanovo.
Our specialized power electronics engineering group provides detailed schematics, busbar cross-section sizing recommendations, cooling circuit flow calculations, and remote digital commissioning support.
Detailed answers regarding technical specifications, local utility compatibility, customs procedures, and operation in North Macedonia.