ISO 9001:2015 & TÜV Rheinland Verified Manufacturing
Electrophoretic Coating Power Supply Manufacturer & Exporters in the Tiraspol Market
Engineered High-Frequency Switch Mode DC Power Units, High-Precision Cathodic/Anodic Electrocoat Rectifiers, and Heavy-Duty Industrial Conversion Solutions for Moldovan & Transnistrian Surface Engineering Plants.
Precision Industrial Rectification
Specialized E-Coat, Anodizing & Electroplating Power Assemblies
Continuous-duty Constant Current / Constant Voltage (CC/CV) power supplies designed for superior throw-power, sub-1% voltage ripple, and ultra-high chemical immersion durability.
High-Efficiency Electrophoretic Coating Power Architectures in Tiraspol
A technical overview of modern switch-mode IGBT power conversion vs legacy SCR systems within regional heavy-equipment, agricultural machinery, and automotive part manufacturing facilities.
Electrophoretic deposition (EPD)—widely identified across industrial manufacturing as cathodic electrodeposition (CED) or electrophoretic painting (e-coat)—demands unparalleled precision in direct current regulation. In the regional manufacturing hub of Tiraspol and the wider Transnistrian and Moldovan industrial basins, modern manufacturing infrastructure is actively undergoing mechanical equipment retrofits. Historically powered by heavy, oil-immersed silicon-controlled rectifiers (SCR/Thyristors) of the late Soviet and early Eastern European industrial era, regional electrocoating facilities frequently face power inefficiency, excessive harmonic pollution, and high rejection rates stemming from voltage ripple anomalies.
As international supply chains impose stringent automotive and agricultural quality standards (including 1,000-hour neutral salt spray corrosion thresholds under ISO 9227 and ASTM B117), the role of the electrophoretic coating power supply becomes decisive. Guangdong Fenvix Technology Co., Ltd. supplies high-efficiency, solid-state IGBT switch-mode DC power units engineered precisely to resolve these challenges, providing smooth soft-ramp energization, robust throwing power into concealed metal cavities, and high operational resilience under fluctuating input grid parameters.
Engineering Core: Unlike standard DC bench sources, an authentic electrophoretic painting rectifier must combine a sub-1% voltage ripple coefficient with programmable multi-segment soft-start capabilities. This prevents high inrush currents upon workpiece immersion, suppressing paint "orange peel," pinholes, electrical rupture marks, and edge burning on complex structural steel fabrications.
Localized Industrial Application Scenarios in the Tiraspol Basin
Surface finishing infrastructure across Tiraspol, Bender, and neighboring processing zones serves a distinct collection of demanding industries requiring dependable DC power systems:
Agricultural Machinery & Implements
Continuous priming of tillage tools, chassis frames, and seed drills requiring resilient cathodic epoxy primers that withstand corrosive chemical fertilizers, mud, and mechanical abrasion.
Automotive Components & Fasteners
High-throw-power barrel and rack e-coating lines for steering linkages, stamped brackets, and spring clips needing micro-level paint uniformities without mechanical thread jamming.
Electrical Enclosures & Switchgear
Complete surface passivation and primer insulation coating for sheet metal cabinets, distribution boards, and industrial housings requiring flawless edges and strict dielectric properties.
Cast Iron Pump & Motor Casings
Heavy submersible hydraulic casings and motor stator frames processed through deep immersion tanks where water-cooled rectifiers operate 24/7 under dense airborne chemical vapors.
Technological Evolutionary Trends in Regional Coating Facilities
Plant operators across the Dniester River industrial corridor are navigating rapid shifts in operational economics and international energy benchmarks. Three noticeable engineering trends define recent equipment procurement:
1. Replacement of SCR Systems with High-Frequency IGBT Topologies: Traditional thyristor rectifiers exhibit an efficiency ceiling around 70% to 75% at variable output loads, with a poor power factor that incurs power supply penalties from regional electrical utilities. Fenvix high-frequency switch-mode power supplies operate near 90% typical electrical efficiency, maintaining a power factor greater than 0.95 across 30% to 100% current settings. Over a multi-tank production line operating 16 hours daily, this reduction in active kWh draw delivers full system payback within 14–18 months.
2. SCADA and Automated Line Integration via Fieldbus Networks: Outdated manually tuned potentiometer dials are rapidly being decommissioned. Modern surface finishing plants in Tiraspol rely on centralized PLC automation. Fenvix integrates isolated RS485 (Modbus-RTU) interfaces and 0–10V/4–20mA analog terminals standard across our e-coat rectifiers. System engineers can dynamically orchestrate multi-step voltage ramping profiles synchronized with conveyor hoist arrival, track amp-hour totalization for paint replenishment, and instantly capture tank fault telemetry.
3. Severe Environment Sealed Cabinet Engineering: Coating and galvanizing shopfloors are characterized by acidic vapors, elevated moisture, and airborne particulates. Conventional air-cooled power supplies that draw ambient workshop air directly over sensitive control printed circuit boards (PCBs) suffer from trace electrolytic corrosion and untimely bridge failure. Fenvix answers this challenge through internally sealed water-cooled enclosures (IP54/NEMA 4 equivalent) and double-layer polyurethane conformal coatings across all drive logic circuitry.
Performance Characteristic
Legacy SCR / Thyristor Rectifier
Fenvix High-Frequency IGBT Rectifier
Direct Process Impact
DC Output Ripple Factor
5% to 15% (Higher at lower load)
≤ 1% to 2% RMS Flat
Eliminates pinholes; achieves smoother, denser film layers.
Electrical Energy Efficiency
70% – 76% Average
90% – 93% High Efficiency
Lowers plant electricity consumption by up to 20%–25%.
Physical Volume & Weight
100% (Bulky, heavy footprint)
~30% – 35% Compact Modular
Frees up floor space; simplifies mezzanine or gantry mounting.
Response Time to Load Shock
Slow (100–200 ms dynamic delay)
Ultra-Fast (≤ 10 ms transient)
Prevents over-current trips upon workpiece tank immersion.
Power Factor (Cos φ)
0.65 – 0.80 (Varies with phase angle)
≥ 0.95 Natural High PF
Avoids reactive power penalty charges from utility grids.
Guangdong Fenvix Technology Co., Ltd. does not trade or re-badge; we engineer, stamp, assemble, and validate every power supply under ISO 9001 certified protocols since 2013.
Main Assembly Workshop
Finished Industrial Cabinets
Waveform & Ripple Inspection
In-House CNC Fabrication
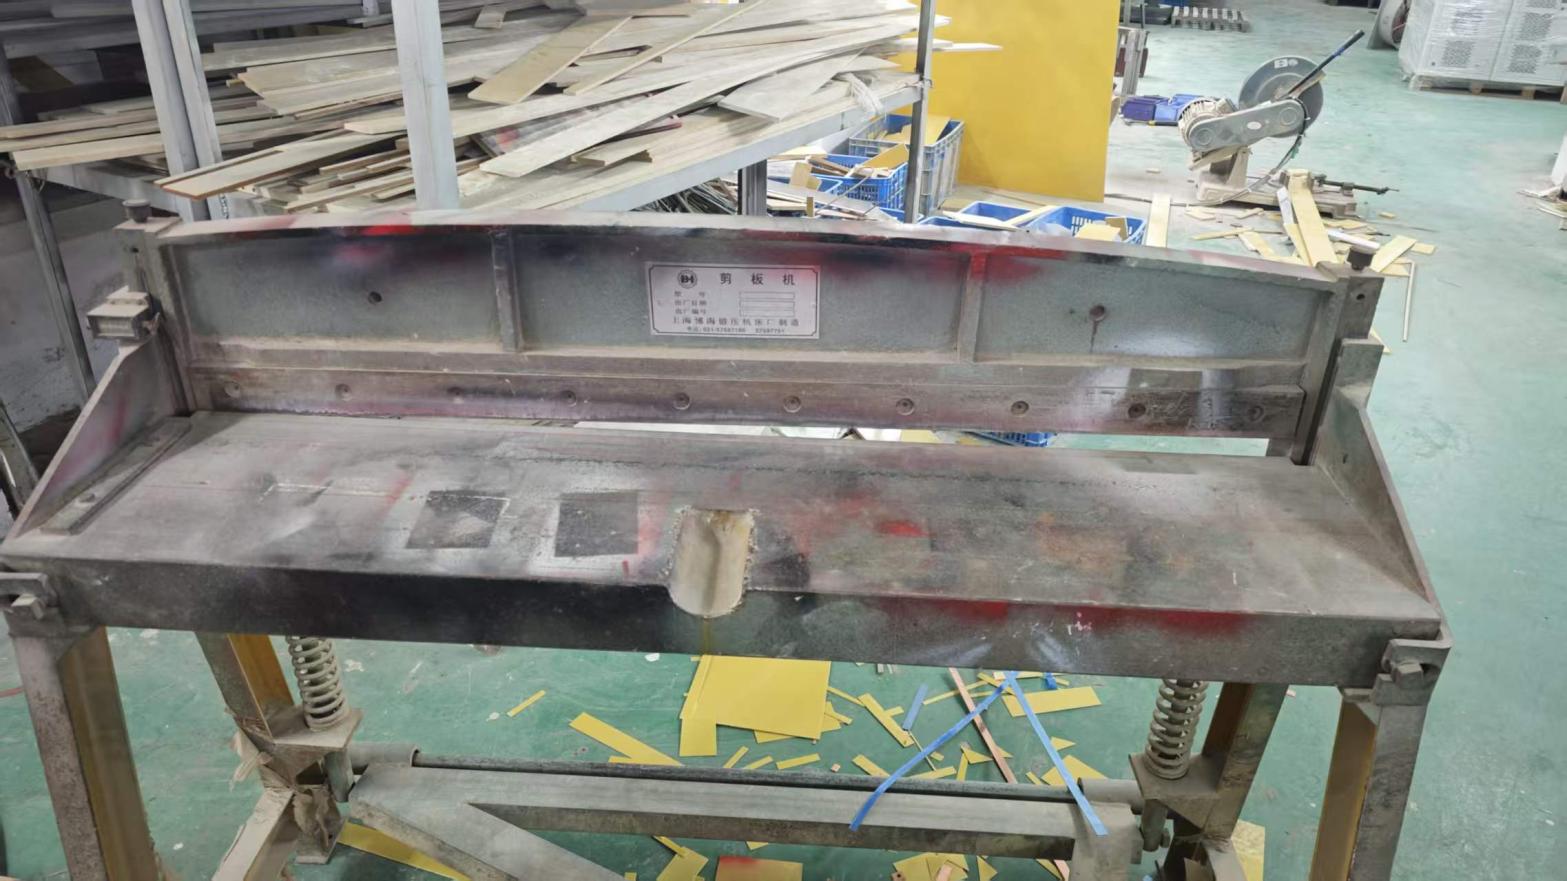
With an operational floor span encompassing over 3,000 square meters and an engineering cohort boasting more than a decade of specialized high-power DC design expertise, Fenvix eliminates production bottlenecks. Enclosures, chassis frames, and high-purity T2 red copper busbars are fabricated internally using precision plate shearing, drilling, tapping, and milling machinery. This guarantees precise busbar surface flatness, lowering interface contact resistance and mitigating heat concentration at extreme current thresholds up to 15,000A.
Each electrophoretic and plating rectifier undergoes a structured 5-stage qualification regimen before being dispatched to our clients across Europe, Asia, and the Americas: incoming raw material quality assessment, printed circuit board automated testing, sub-assembly wiring verification, full-load dynamic oscilloscope ripple analysis, and uninterrupted high-temperature load burn-in. Third-party verified on site by TÜV Rheinland, our operations adhere strictly to international Low Voltage (LVD) and Electromagnetic Compatibility (EMC) standards.
Local Procurement Clarity
Frequently Asked Questions by Industrial Buyers in Tiraspol
Direct answers addressing voltage compatibility, logistics, duty cycles, and custom technical adaptations for the regional European and Eurasian trade routes.
What parameters are required to accurately size an electrophoretic coating power supply?
To properly size the unit, provide: (1) Total active immersion surface area per rack/flight-bar (in m²), (2) Target current density recommended by your paint supplier (typically 20–40 A/m² for cathodic epoxy electrocoat), (3) Desired bath operating voltage (typically 150V to 350V DC), (4) Paint conductivity and throwing power parameters, and (5) Ambient workshop cooling availability. Our engineering desk uses these figures to configure the optimum transformer turns ratio, output filtering inductors, and soft-ramp timing logic.
Can Fenvix rectifiers accommodate voltage irregularities in Eastern European utility grids?
Yes. Industrial mains in older factory districts can experience grid instability ranging between ±10% to ±15%. Fenvix rectifiers feature a wide AC input voltage tolerance window (standard 380V/400V 3-phase ±15%, 50Hz/60Hz) paired with ultra-fast DSP closed-loop feedback circuitry. The system stabilizes DC output voltage variations within ≤ ±0.5% despite severe incoming AC voltage drops or surges.
Is there a Minimum Order Quantity (MOQ) for custom-engineered power supplies?
We maintain a strict No Minimum Order Quantity (MOQ: 1 Set) policy. Whether you require a single 20A experimental benchtop e-coat rectifier for metallurgical research, a replacement unit for an existing line, or a multi-unit 8000A installation for an automated chassis turnkey plant, we provide full engineering support, customized busbar layouts, and dedicated project management.
What are the international shipping terms, transit methods, and documentation for Tiraspol delivery?
We routinely deliver via multiple Incoterms including EXW, FOB (Guangzhou/Shenzhen), CIF (Constanța or regional European distribution hubs), CIP, and DDP by multimodal air cargo and sea-rail networks. All export shipments are packed inside fumigated, moisture-sealed ISPM-15 wooden crates and accompanied by full Certificates of Origin, ISO 9001 factory test inspection sheets, CE declarations, and technical wiring schematics in English.
How does Fenvix support overseas commissioning and warranty servicing?
Fenvix supplies all rectifiers with comprehensive modular plug-in sub-assemblies. In addition to clear wiring schematics and pre-commissioning video calls with our senior electrical engineers, we stock complete replacement drive boards, IGBT modules, and sensor assemblies. Should a fault occur, remote diagnostics identify the issue rapidly, and verified on-site third-party technical support protocols are established to ensure zero sustained plant downtime.
Optimize Your Coating Quality & Energy Efficiency
Consult directly with Fenvix power system application engineers. Receive custom dimensional drawings, electrical schematics, and an engineering quotation tailored to your production bath specs within 24 hours.