Industrial Electroforming & Electrochemical Systems
Engineered for exacting electroforming, micro-molding, and thick-layer metal replication. Continuous CV/CC operation, ultra-low ripple coefficient (<1%), and modular IGBT architecture.

12V 15V 5000A 6000A 75KW Water Cooled High Frequency Rectifier
- Output: 0–15V / 0–6000A
- Power: 75kW Heavy Duty
- Cooling: Pure Water Cooled
- Control: Digital Display CV/CC

12V 4000A 48kW High Frequency Electroplating Rectifier
- Output: 0–12V / 0–4000A
- Efficiency: ≥ 90% IGBT Stage
- Control: RS485 Modbus RTU
- Ripple: < 2% RMS Low Noise

8000A 12V Water-Cooled Galvanizing & Electroforming Rectifier
- Output: 12V / 8000A Continuous
- Enclosure: IP54 Sealed Cabinet
- Protection: Thermal, Overcurrent
- Duty: 24/7 Continuous Load

12V 150A Precision Electroforming & Au/Ag Plating Unit
- Output: 0–12V / 0–150A Step-less
- Accuracy: ±0.5% Setpoint Reg.
- Application: Optical & Micro-forms
- Norms: CE, LVD, EMC Compliant

48V 625A Auto Polarity Reversing Electrochemical Power Supply
- Output: 0–48V / 0–625A
- Reversal: Programmable Timer
- Bus: PLC Automated Interface
- Use: Stress Relief & Etching

300kW 20V 15,000A Heavy-Duty Electrolysis Rectifier
- Current: Up to 15,000A DC
- Structure: Independent Water Circuit
- Busbar: T2 Oxygen-Free Copper
- Rating: Industrial Grade 100%

100–3000A Multi-Range Adjustable Anodizing & Forming Source
- Voltage: 12V / 24V / 60V Options
- Ramp Mode: Multi-Step Current Slope
- Display: Touchscreen HMI Unit
- Reliability: Dual Over-Temp Cutoff
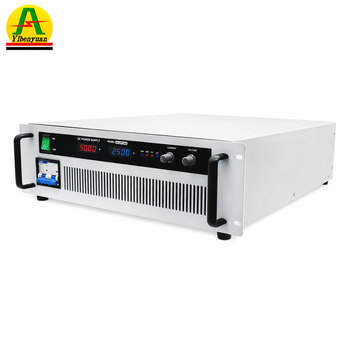
1.5kW–5kW Programmable Electroforming Lab DC Source
- Precision: 1mV / 1mA Resolution
- Interface: USB / RS232 / RS485
- Waveforms: DC, Pulse, Stepped Ramp
- Standard: EMC Class A Industrial
Engineering Whitepaper: Advanced Electroforming Power Supplies for Narva Industrial Hubs
Electroforming represents one of the most demanding sub-disciplines in advanced electrometallurgy. Unlike traditional decorative or sacrificial electroplating, where thin coatings (typically 5 to 25 microns) are deposited on a permanent substrate, electroforming involves atomic deposition of metals onto a sacrificial or reusable mandrel until structural thicknesses ranging from 100 microns to several millimeters are achieved. In Narva and the surrounding Ida-Viru county of Estonia, where precision engineering, energy-intensive manufacturing, metal recycling, and high-tech instrument production intersect, modernizing electroforming processes with switch-mode IGBT power supplies is vital to ensuring low mechanical stress, consistent grain morphology, and maximum electrical efficiency.
Technical Distinction: The micro-structural integrity of electroformed components—such as nickel rotary screens, optical molds, waveguide assemblies, and micro-fluidic nozzles—relies primarily on the suppression of root-mean-square (RMS) current ripple. A ripple coefficient exceeding 2% in the cathode film boundary promotes chaotic grain crystallization, internal lattice dislocations, and destructive macro-stress that results in structural warping upon separation from the mandrel.
Why Narva Manufacturers Transition from Thyristor (SCR) to High-Frequency IGBT Inverters
Historically, heavy industrial zones throughout the Baltic corridor relied on legacy 50Hz thyristor (SCR) rectifiers. While these units provide robust brute-force DC current, their technological limitations create severe bottlenecks in modern European precision manufacturing environments:
- Low Electrical Conversion Efficiency: SCR units operate with typical thermodynamic efficiencies of only 70% to 78%, dissipating valuable electrical power as waste heat into production facilities. Guangdong Fenvix high-frequency switch-mode rectifiers operate at efficiencies of 90% to 94%, significantly lowering plant overhead under prevailing Baltic power tariffs.
- Harmonic Pollution and Power Factor Degradation: Line-commutated SCR rectifiers create severe line distortion and display a poor power factor (often below 0.75 when throttled down). In contrast, Fenvix IGBT units integrate active power conditioning that maintains a power factor >0.93 across varying load profiles, protecting Narva power grids from harmonic penalties.
- Ripple Dynamics and Nucleation Density: SCR rectifiers inherently output high 300Hz line-frequency ripple unless huge, failure-prone LC smoothing chokes are installed. Our switch-mode rectifiers operate at inversion frequencies of 20kHz to 50kHz, delivering exceptionally smooth DC with a current ripple under 1%, vital for atomic micro-crystallization.
Technical Matrix: Electroforming vs. Standard Electroplating Specifications
| Electrical Parameter | Standard Surface Plating | Fenvix High-Precision Electroforming | Engineering Value to Narva Buyers |
|---|---|---|---|
| Current Ripple (RMS) | < 5% to 8% | < 1% to 1.5% | Eliminates internal grain lattice shear stress |
| Voltage Stability | ± 2.0% | ± 0.5% (High Accuracy) | Absolute repeatability across 72+ hour runs |
| Operating Inversion | Line 50Hz / SCR | 20kHz – 50kHz IGBT PWM | Substantial cabinet footprint & weight reduction |
| Current Density Control | Manual / Analog Dial | 0.01 A/dm² Programmable Steps | Prevents burning of micro-fine structural corners |
| Cooling Configurations | Standard Ambient Air | Isolated Water-Cooled or Sealed Chilled | Zero acid fume ingestion; IP54 internal electronics |
Localized Applications Across Narva & the Baltic Industrial Corridor
Targeted power electronics engineered to meet the manufacturing, material processing, and industrial R&D demands of Ida-Virumaa.
Micro-Screens & Filter Tubes
Continuous nickel electroforming of micro-perforated filtration screens utilized in chemicals, biotechnology, and agricultural centrifuges across regional processing facilities.
Precision Tooling & Mold Inserts
Manufacturing optical discs, lens matrixes, and textured injection molding cavities by depositing stress-free nickel-cobalt alloys over microscopic master mandrels.
Aerospace & Waveguide Channels
Seamless copper electroforming of complex microwave horns, millimeter-wave conduits, and RF shielding components requiring internal mirror surface finishes below 0.05 μm Ra.
Renewable Energy & Battery Foils
Ultra-thin copper and nickel foil deposition for modern lithium battery anodes and specialized electrolyzer components powering Baltic decarbonization initiatives.
Ida-Virumaa's Industrial Transition & High-Efficiency Power Trends
As northeastern Estonia transitions from legacy energy extraction toward high-value, green technological manufacturing, the demands placed on manufacturing equipment have evolved dramatically. European decarbonization frameworks, coupled with stringent environmental accountability, require manufacturing plants in Narva Industrial Parks to prioritize three specific technological trends:
1. Industry 4.0 Digital Integration: Standalone analog rectifiers are no longer viable for modern quality compliance. Baltic exporters need power supplies with native Profinet, Modbus-TCP, and RS485 digital interfaces that feed cycle logs directly to central SCADA engines, ensuring lot-by-lot metallurgical traceability for precision clients across Germany, the Nordics, and broader Europe.
2. Thermal Stability via Dedicated Chilled Water Circuits: Plating facilities handling chemical nickel sulfamate or acid copper electrolytes suffer high corrosive airborne degradation. Modern installations throughout Ida-Virumaa demand water-cooled power stages housed in sealed IP54 to NEMA 4X enclosures, isolating critical IGBT bridges from chemical vapors and reducing internal plant HVAC burdens.
3. Dynamic Forward & Reverse Pulse Modulation: The integration of automated reverse pulse electroforming allows fabricators to systematically dissolve micro-protrusions during crystal lattice formation. By cycling between forward deposition and high-frequency reverse stripping, Narva producers eliminate macroscopic nodular dendrites, generating thicker, flawless wall geometries with uniform tensile strength.
Guangdong Fenvix Factory Capabilities & Engineering Assurance
ISO 9001 certified manufacturing facility in Guangzhou, China. Direct engineering support, in-house fabrication, zero middleman overhead, and global logistics capability.
Since 2013
13+ Years of Continuous R&D Specialization
3,000 m²
Integrated Assembly & Metal Fabrication Facility
ISO 9001
Certified Quality System Verified by TÜV Rheinland
CE Conformity
Full EMC & LVD Compliance for European Imports
No MOQ
Custom Single Prototypes to Multi-Cabinet Lines
Direct Factory
In-House Copper Busbar & Sheet Metal Production
Procurement FAQ for Narva & Estonian Engineering Teams
Clear, direct answers regarding custom electrical sizing, European grid compliance, logistics, and technical commissioning support.