DC Regulated Power Supply Manufacturer & Supplier in Chicago
Industrial-Grade High-Frequency Rectifiers, Programmable High-Voltage DC Sources & Aircraft Ground Power Units Engineered for Greater Chicago & Midwest Heavy Manufacturing
Precision Engineered Units
Featured Industrial DC Power Supplies & Rectifiers
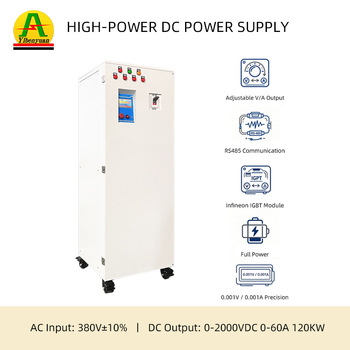
Direct-from-manufacturer high-power DC switching architectures configured specifically for continuous duty in Chicago's metal finishing, automotive tier testing, aerospace maintenance, and scientific research labs.
75kW Water-Cooled
12V/15V 5000A–6000A 75KW Water Cooled Plating Rectifier
Engineered for Chicago's Advanced Manufacturing Corridors
From the dense metal finishing plants along the Chicago Sanitary and Ship Canal to precision toolmakers in Elk Grove Village and energy test bays in DuPage County, regulated direct current power supplies are mission-critical. Here is how Fenvix systems solve harsh local operating challenges.
Metal Finishing & Electroplating
Greater Chicago remains one of North America's dense concentrations of job-shop platers and surface finishing facilities. In hard chrome, decorative nickel, and zinc barrel lines, low output ripple (under 1% RMS) directly determines crystal grain structure, throw power in blind recesses, and corrosion resistance under ASTM B117 salt spray standards.
Recommended: 12V/15V 3000A–8000A Water-Cooled IGBT Units with sealed electronics cabinets protecting against acid mist corrosion.
EV Powertrain & Battery Testing
As the Midwest automotive corridor accelerates battery module production and high-voltage motor assembly, Chicago R&D centers require stable DC sources simulating 400V and 800V architecture battery dynamics. Our programmable switching units feature sub-millisecond dynamic response to suppress inductive kickback during full-throttle acceleration profiles.
Recommended: 800V–1200V 50A–100A High Voltage DC Programmable Supplies with isolated RS485/CAN interfaces for automated test rack integration.
Aviation GSE & Hangar Maintenance
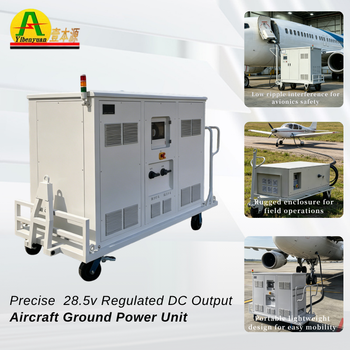
Serving Chicago O'Hare International (ORD) and Chicago Midway (MDW), airline maintenance hubs demand pure, surge-free 28.5V DC ground power units. Units must support cold-weather cranking currents up to 2000A for regional turboprops while maintaining clean, regulated voltage to prevent damage to sensitive avionics glass cockpits.
Recommended: Portable & Skid-Mounted 28.5V DC Ground Power Units featuring weather-sealed NEMA 3R outdoor enclosures and phase fail-safe protection.
Electrolytic Water Treatment & Descaling
Cooling towers, food processing facilities, and chemical processors in Cook and Will counties require chemical-free electrolytic scale control. Fenvix auto-polarity reversing supplies periodically invert electrode polarity, breaking down calcium and magnesium carbonate buildup without manual hydrochloric acid flushes.
Proximate to premier scientific institutions such as Argonne National Laboratory and Fermilab, advanced research programs in particle acceleration, pulsed plasma physics, and electron beam generation demand ultra-high voltage precision with minimal stored energy upon discharge.
Recommended: 0–100kV Capacitor Charging & High Voltage Sources featuring ≤ 0.05% line/load regulation and rapid quenching arc protection circuits.
Electrophoretic Paint (E-Coat) Systems
High-throughput agricultural equipment and automotive component manufacturers require defect-free cathodic electrodeposition. Fenvix E-coat power supplies execute programmable multi-zone voltage ramps, preventing pinholes and orange-peel defects across complex welded geometries.
Recommended: 200V–400V 50A–300A High Voltage E-Coat Systems with soft-start ramp profiling and ripple attenuation below 1.5%.
Technical Whitepaper: Choosing Modern IGBT Switching vs. Legacy SCR Rectifiers in Midwest Manufacturing
Throughout industrial Chicago, Gary, Rockford, and Milwaukee, numerous surface finishing and metal fabrication facilities continue to operate legacy silicon-controlled rectifier (SCR/thyristor) transformer units installed decades ago. While robust, 12-pulse and 6-pulse SCR rectifiers exhibit major engineering shortcomings under contemporary operating pressures: typical electrical conversion efficiency hovers between 68% and 78%, harmonic distortion on plant feeder lines often violates IEEE 519 thresholds, and low-frequency ripple causes non-uniform metallurgical deposition in modern micro-plating.
Fenvix industrial power architectures transition your plant to high-frequency insulated-gate bipolar transistor (IGBT) pulse-width modulation (PWM) topologies switching at 20 kHz to 40 kHz. The engineering advantages directly impact operational profitability:
Engineering Parameter
Traditional SCR / Thyristor Rectifier
Fenvix High-Frequency IGBT Technology
Chicago Plant Economic Advantage
Electrical Conversion Efficiency
68% – 78% (load dependent)
90% – 93% across 30%–100% load
Lowers annual ComEd kilowatt-hour bill by $8,500–$24,000 per 50kW line
Output Ripple Factor
4% – 8% RMS at reduced voltage
≤ 1.0% RMS across full envelope
Prevents microscopic lamination voids; cuts noble metal consumption by 8-14%
Input Power Factor (PF)
0.65 – 0.78 (degrades at partial loads)
≥ 0.94 (integrated active/passive PFC)
Eliminates utility reactive power penalty surcharges on industrial bills
Physical Footprint & Mass
Heavy line-frequency transformer; > 1200 kg
Compact high-frequency core; ~ 320 kg
Allows overhead mezzanine placement; saves precious floor space in urban shops
Response Time to Load Step
Slow phase control: 50 ms – 100 ms
Ultra-fast PWM loop: ≤ 2 ms – 5 ms
Prevents voltage sag during barrel rotation and rack immersion spikes
Cooling Enclosure Sealing
Open air intake; corrosive shop air ingress
Isolated water-cooling or IP54 ducting
Copper and electronics isolated from hydrochloric and sulfuric acid mist
Thermal Management Strategy: Air Cooling vs. Closed-Loop Deionized Water Cooling
Midwest facilities experience severe environmental extremes—sub-zero ambient temperatures during winter months alternating with intense summer heat and humidity. When specifying high-current DC rectifiers (≥ 3,000 Amperes), the choice of cooling system defines mean time between failures (MTBF).
For operations exceeding 40kW total output operating continuous 3-shift schedules, Fenvix strongly advises water-cooled architectures. Our water-cooled configurations utilize heavy-gauge copper heat exchangers with nickel plating. Power semiconductors and magnetic components are completely hermetically sealed from ambient atmospheric fumes. Heat is rejected directly to external chilled water or closed-loop cooling towers, preventing premature degradation of PCB solder joints caused by acidic airborne particulates prevalent in electroplating and anodizing rooms.
Macro Dynamics
Industrial & Energy Trends Driving DC Power Demand in the Midwest
Key infrastructure, sustainability, and technological shifts shaping capital equipment upgrades across Illinois and Great Lakes manufacturing.
Grid Modernization & Peak Load Tariffs
Commonwealth Edison (ComEd) and regional Midwest ISO (MISO) utilities enforce demanding power factor requirements and peak load demand penalties. Upgrading from archaic transformer rectifiers to high-efficiency IGBT supplies with power factor ratings of 0.94+ allows plants to operate high-current electrolysis without incurring penalty tiers.
Industry 4.0 SCADA Integration
Modern machining centers and plating automated hoists demand continuous parameter telemetry. Manual dials are obsolete. Chicago facility managers specify RS485 Modbus, Profibus, or isolated 4–20mA interfaces to log Ampere-hours, tank bath voltage drops, and thermal metrics to centralized manufacturing execution systems (MES).
Defense & Aerospace Mil-Spec Conformance
Subcontractors supporting naval systems around the Great Lakes Naval Station and defense aviation hubs require rigorous compliance with MIL-STD-704 and MIL-STD-810. Power units must demonstrate strict voltage ripple stability, phase margin resilience, and thermal endurance during cold-start operations.
Direct Manufacturer Advantage
Why Chicago Engineers Partner with Guangdong Fenvix Technology
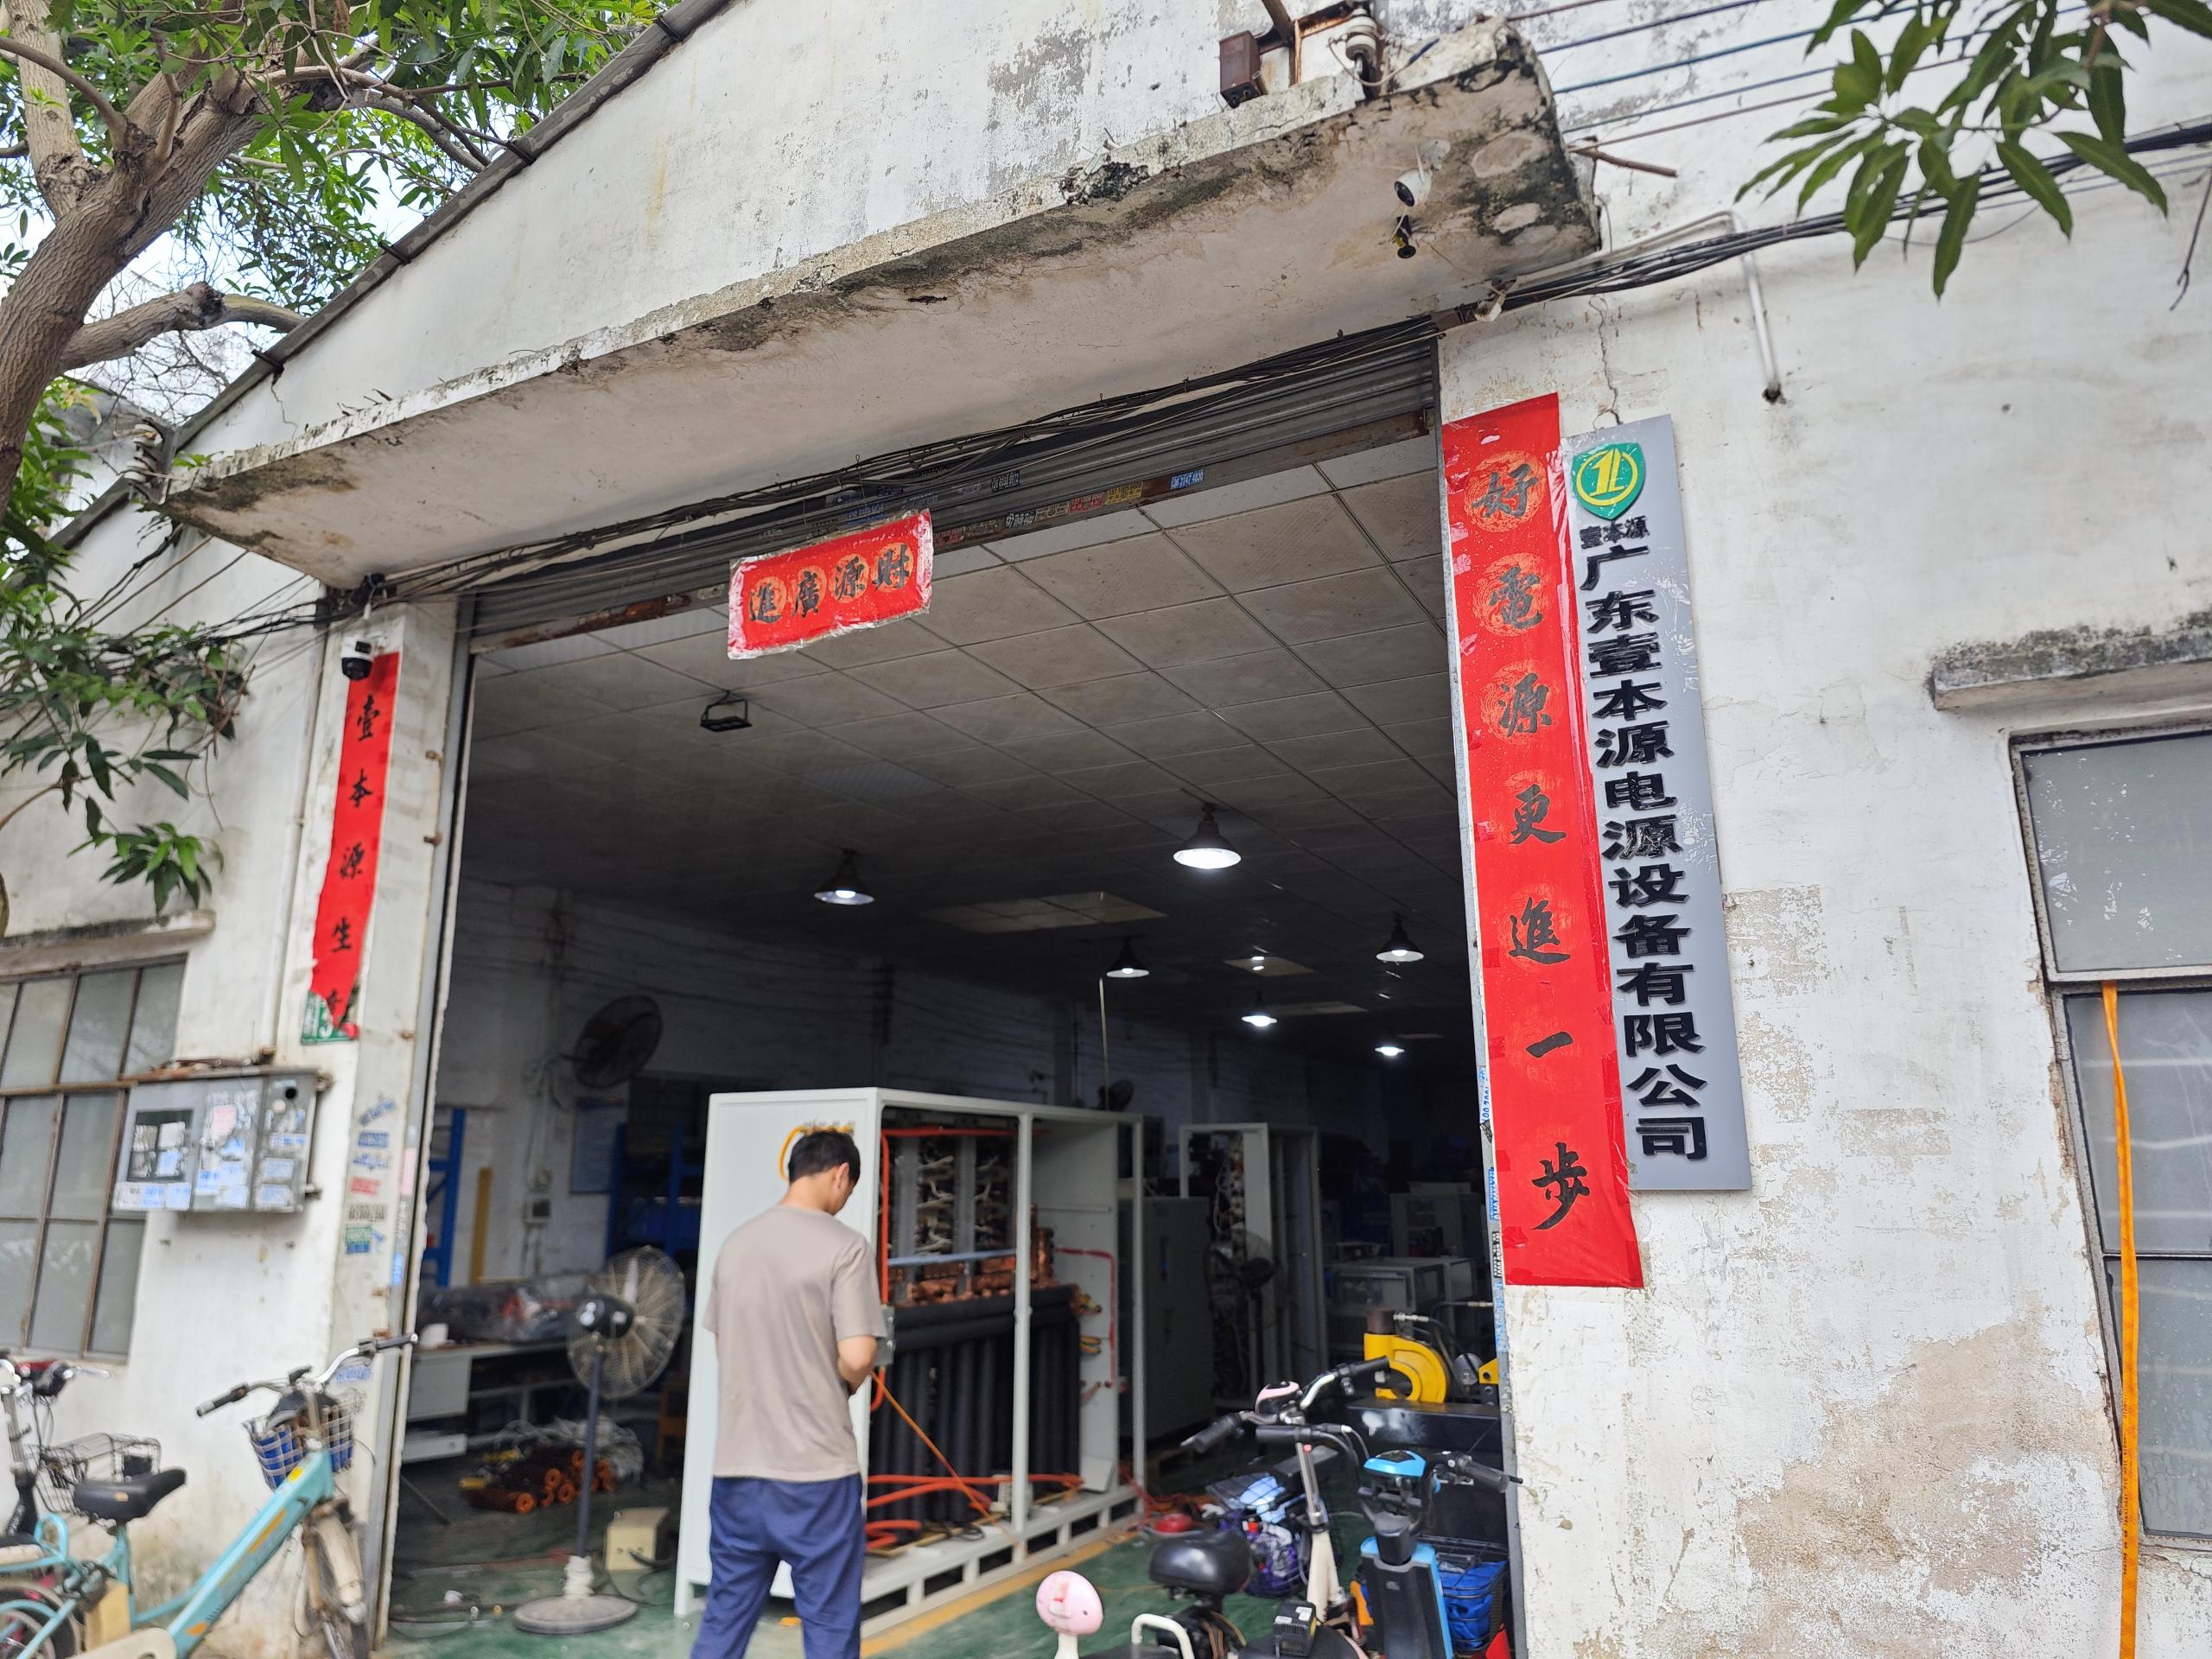
Operating our own specialized 3,000m² manufacturing facility in Guangdong since 2013, Fenvix eliminates trading middleman markups while providing full engineering customization, ISO 9001 quality rigor, and seamless DDP delivery directly to your facility dock.
In-House Sheet Metal, Busbar & Magnetic Assembly
Unlike catalog distributors who re-label outsourced assemblies, Fenvix controls the complete mechanical and electrical fabrication lifecycle under our ISO 9001 certified quality management system. From heavy plate shearing, CNC punching, precision copper busbar milling, and drilling to robotic transformer winding, every element is engineered under direct oversight.
Zero Minimum Order Quantity (No MOQ): Single-unit prototypes and custom R&D designs receive the same rigorous engineering attention as 50-unit production runs.
TÜV Rheinland On-Site Verified: Independent international third-party audit verifies physical production floor capability, trade safety, and engineering equipment.
100% Load-Bank Burn-In: Every single power supply undergoes full-voltage, full-current burn-in testing under dynamic oscilloscope monitoring before export dispatch.
US Grid Compatibility Engineered: Built native for 480V 3-Phase 60Hz or 208V/240V 60Hz delta/wye systems with American industrial safety interlocks.
ISO 9001 : 2015 Certified Factory
Production Workshop Floor
Finished High-Current Cabinets
Oscilloscope Precision Calibration
Full-Load Commissioning Testing
Buyer Knowledge Base
Frequently Asked Questions by Chicago & Midwest Buyers
Comprehensive engineering, logistics, and compliance answers for plant engineers, procurement directors, and maintenance leads.
Can Fenvix power supplies accommodate standard US three-phase 480V 60Hz industrial inputs?
Yes, absolutely. While default European architectures utilize 380V/400V 50Hz, all Fenvix industrial power supplies built for the US market are engineered with native 480VAC ± 10% 3-phase 60Hz or 208V/240V 60Hz input configurations. We size the internal input line reactors, primary rectifier diodes, and high-frequency filtering to match American National Standards Institute (ANSI) C84.1 voltage tolerances without requiring auxiliary external step-down transformers.
What documentation and technical data are required to order a fully customized DC source?
To ensure optimal engineering sizing, we ask Chicago clients to provide: (1) Primary AC line voltage, phase count, and frequency; (2) Target DC voltage and current adjustment range; (3) Operating mode requirement (Constant Voltage, Constant Current, Constant Power, or Auto-Polarity Reversal); (4) Maximum permissible output ripple factor; (5) Daily duty cycle (e.g., 24/7 continuous vs. intermittent test profile); (6) Thermal cooling preference (forced air, closed-loop DI water, or air-to-water heat exchanger); and (7) Remote communication protocol (RS485 Modbus, 0-10V/4-20mA analog, or Ethernet LAN). Our engineering department returns a formal general arrangement drawing and electrical schematic within 24 business hours.
How does Fenvix handle transatlantic logistics, customs clearance, and DDP delivery into Chicago?
We provide full Delivered Duty Paid (DDP) logistics directly to your facility address in Cook, DuPage, Lake, or Kane County. For urgent laboratory or ATE line needs, air freight via Chicago O'Hare (ORD) delivers in 5 to 7 business days. For heavy industrial water-cooled rectifiers, ocean intermodal freight enters through West Coast ports or directly via Great Lakes rail intermodal ramps into Chicago container yards. We handle US Customs clearance, ISF filing, and tariff documentation, eliminating customs clearance burdens for your procurement staff.
When should an electroplating facility specify closed-loop water cooling over forced-air cooling?
Water cooling is strongly recommended when: (1) Current ratings exceed 3,000A DC; (2) The power supply is physically situated within 20 feet of heated acid, cyanide, or caustic plating tanks where airborne corrosive vapors would attack cooling fan bearings and internal circuit board traces; or (3) Ambient shop temperatures exceed 35°C (95°F) during Midwestern summers. For clean laboratory environments, automotive R&D test benches, or low-amperage applications under 1,000A, forced-air cooling with filtered fan assemblies remains highly cost-effective and simple to maintain.
What international quality certifications, standards, and electrical safety marks apply?
Fenvix operates an audited ISO 9001:2015 Quality Management System verified on-site by TÜV Rheinland. Our power architectures comply with European CE directives including Low Voltage Directive (LVD 2014/35/EU) and Electromagnetic Compatibility (EMC 2014/30/EU), as well as RoHS hazardous substance restrictions. For plants adhering strictly to National Electrical Code (NEC) standards, our components utilize UL-recognized circuit breakers, contactors, and terminal blocks with comprehensive arc suppression.
What after-sales warranty, spare parts support, and technical commissioning services are offered?
All Fenvix power systems include a standard 12-month direct factory warranty covering all components, electronics, and magnetic assemblies. Because our units are engineered with modular IGBT bridges and standard control boards, critical maintenance components can be swapped in minutes. We provide full wiring schematics, pinout guides, and real-time video technical commissioning support directly with our senior electrical engineering team.
Upgrade Your Chicago Facility with Factory-Direct Power Precision
Eliminate high distributor markups and standard catalog compromises. Connect directly with Fenvix power application engineers to design, build, and deploy custom DC regulated power supplies tailored precisely to your operational loads.