Water-Cooled

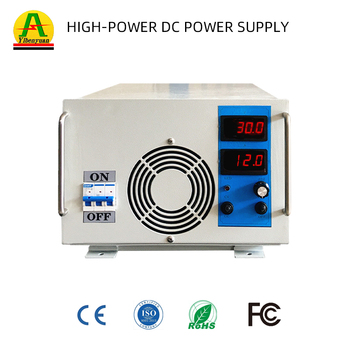
12V/15V 5000A-6000A 75kW Water-Cooled Plating Rectifier
- TopologyHigh Frequency IGBT
- Output Range0–15V / 0–6000A
- Cooling ModeDeionized/Tap Water
- Control StandardRS485 / Modbus RTU
Manufactured by Guangdong Fenvix Technology Co., Ltd. for extreme duty cycles, sub-1% current ripple, and advanced automated tank integration.






The Inn Valley corridor in Tyrol, centered around Innsbruck, represents one of Central Europe's most exacting hubs for high-precision mechanical engineering, alpine technology fabrication, high-voltage component manufacturing, and medical technology. Surface treatment in this Alpine environment requires strict adherence to environmental containment, energy-efficiency benchmarks (under Austrian and EU Energy Efficiency Directives), and micro-level consistency in layer thickness. As surface treatment operations in Innsbruck transition from legacy silicon-controlled rectifiers (SCR/Thyristor) to modern insulated-gate bipolar transistor (IGBT) topologies, the selection of switching frequency, ripple factor, and harmonic distortion control becomes decisive.
Guangdong Fenvix Technology Co., Ltd. serves industrial coaters, electroplaters, and R&D centers across Innsbruck by delivering high-frequency, water-cooled and sealed air-cooled DC power supplies that bridge European engineering standards with the agile scale of custom Chinese manufacturing. With switching frequencies running from 20 kHz to 50 kHz, our rectifiers deliver continuous current regulation with an ultra-low ripple (<1% RMS), substantially reducing the edge burn and uneven deposition commonly caused by traditional 50Hz thyristor spikes.
Tyrolean industrial production presents unique operating conditions: closed-loop thermal recovery systems, stringent municipal effluent laws, and components designed for harsh alpine cold or high-stress biomedical implantation. Below is how our surface treatment power systems integrate across key localized segments:
Innsbruck's specialized ropeway builders, ski lift component makers, and heavy winter infrastructure manufacturers require thick, crack-free hard chrome plating and duplex zinc-nickel coatings. Our water-cooled 5,000A to 15,000A IGBT rectifiers deliver unbroken continuous power under continuous bath load, ensuring flawless coating density resistant to extreme salt exposure, freeze-thaw cycles, and heavy mechanical shear.
Tyrol's medical devices cluster demands exceptional surface passivity and bio-compatible color-coding on titanium bone screws, plates, and dental fixtures. Fenvix Type II & Type III titanium anodizing power units (0–150V) offer programmable micro-ramping, fast transient response (≤10ms), and ripple ≤0.5%, guaranteeing uniform oxide thickness and complete color stability without crystal defects.
Tier-1 suppliers throughout the Inn Valley machining automotive cast parts and aerospace structural ribs utilize our programmable hard anodic oxidation rectifiers. With multi-step current ramps, automated bath-temperature interlocks, and RS485/Modbus networks, Tyrolean operators completely eliminate the hazard of localized burning during oxide pore construction.
The Federal State of Tyrol enforces stringent standards regarding industrial grid noise and energy preservation (in alignment with the Austrian Federal Energy Efficiency Act - EEffG). Plating shops in industrial zones like Rossau and Hall in Tirol are modernizing obsolete systems driven by three major local imperatives:
Traditional 6-pulse and 12-pulse SCR rectifiers inject high current harmonics into the municipal 400V grid, triggering power factor penalties from regional providers like TIWAG. Fenvix IGBT rectifiers maintain power factors exceeding 0.93 with drastically diminished total harmonic distortion, protecting sensitive local facility PLC networks.
Environmental guidelines in the Inn Valley discourage air-expelled industrial heat that raises ambient HVAC loads. Fenvix water-cooled rectifiers transfer thermal dissipation directly into central deionized cooling circuits, enabling Tyrol plants to recycle power conversion heat back into pre-treatment bath heating.
As chrome VI bans and chemical additives come under stricter monitoring, current distribution uniformity becomes crucial. The tighter the current control, the lower the chemical overdosing required to meet minimum plate thickness tolerances—cutting chemistry consumption by up to 18%.
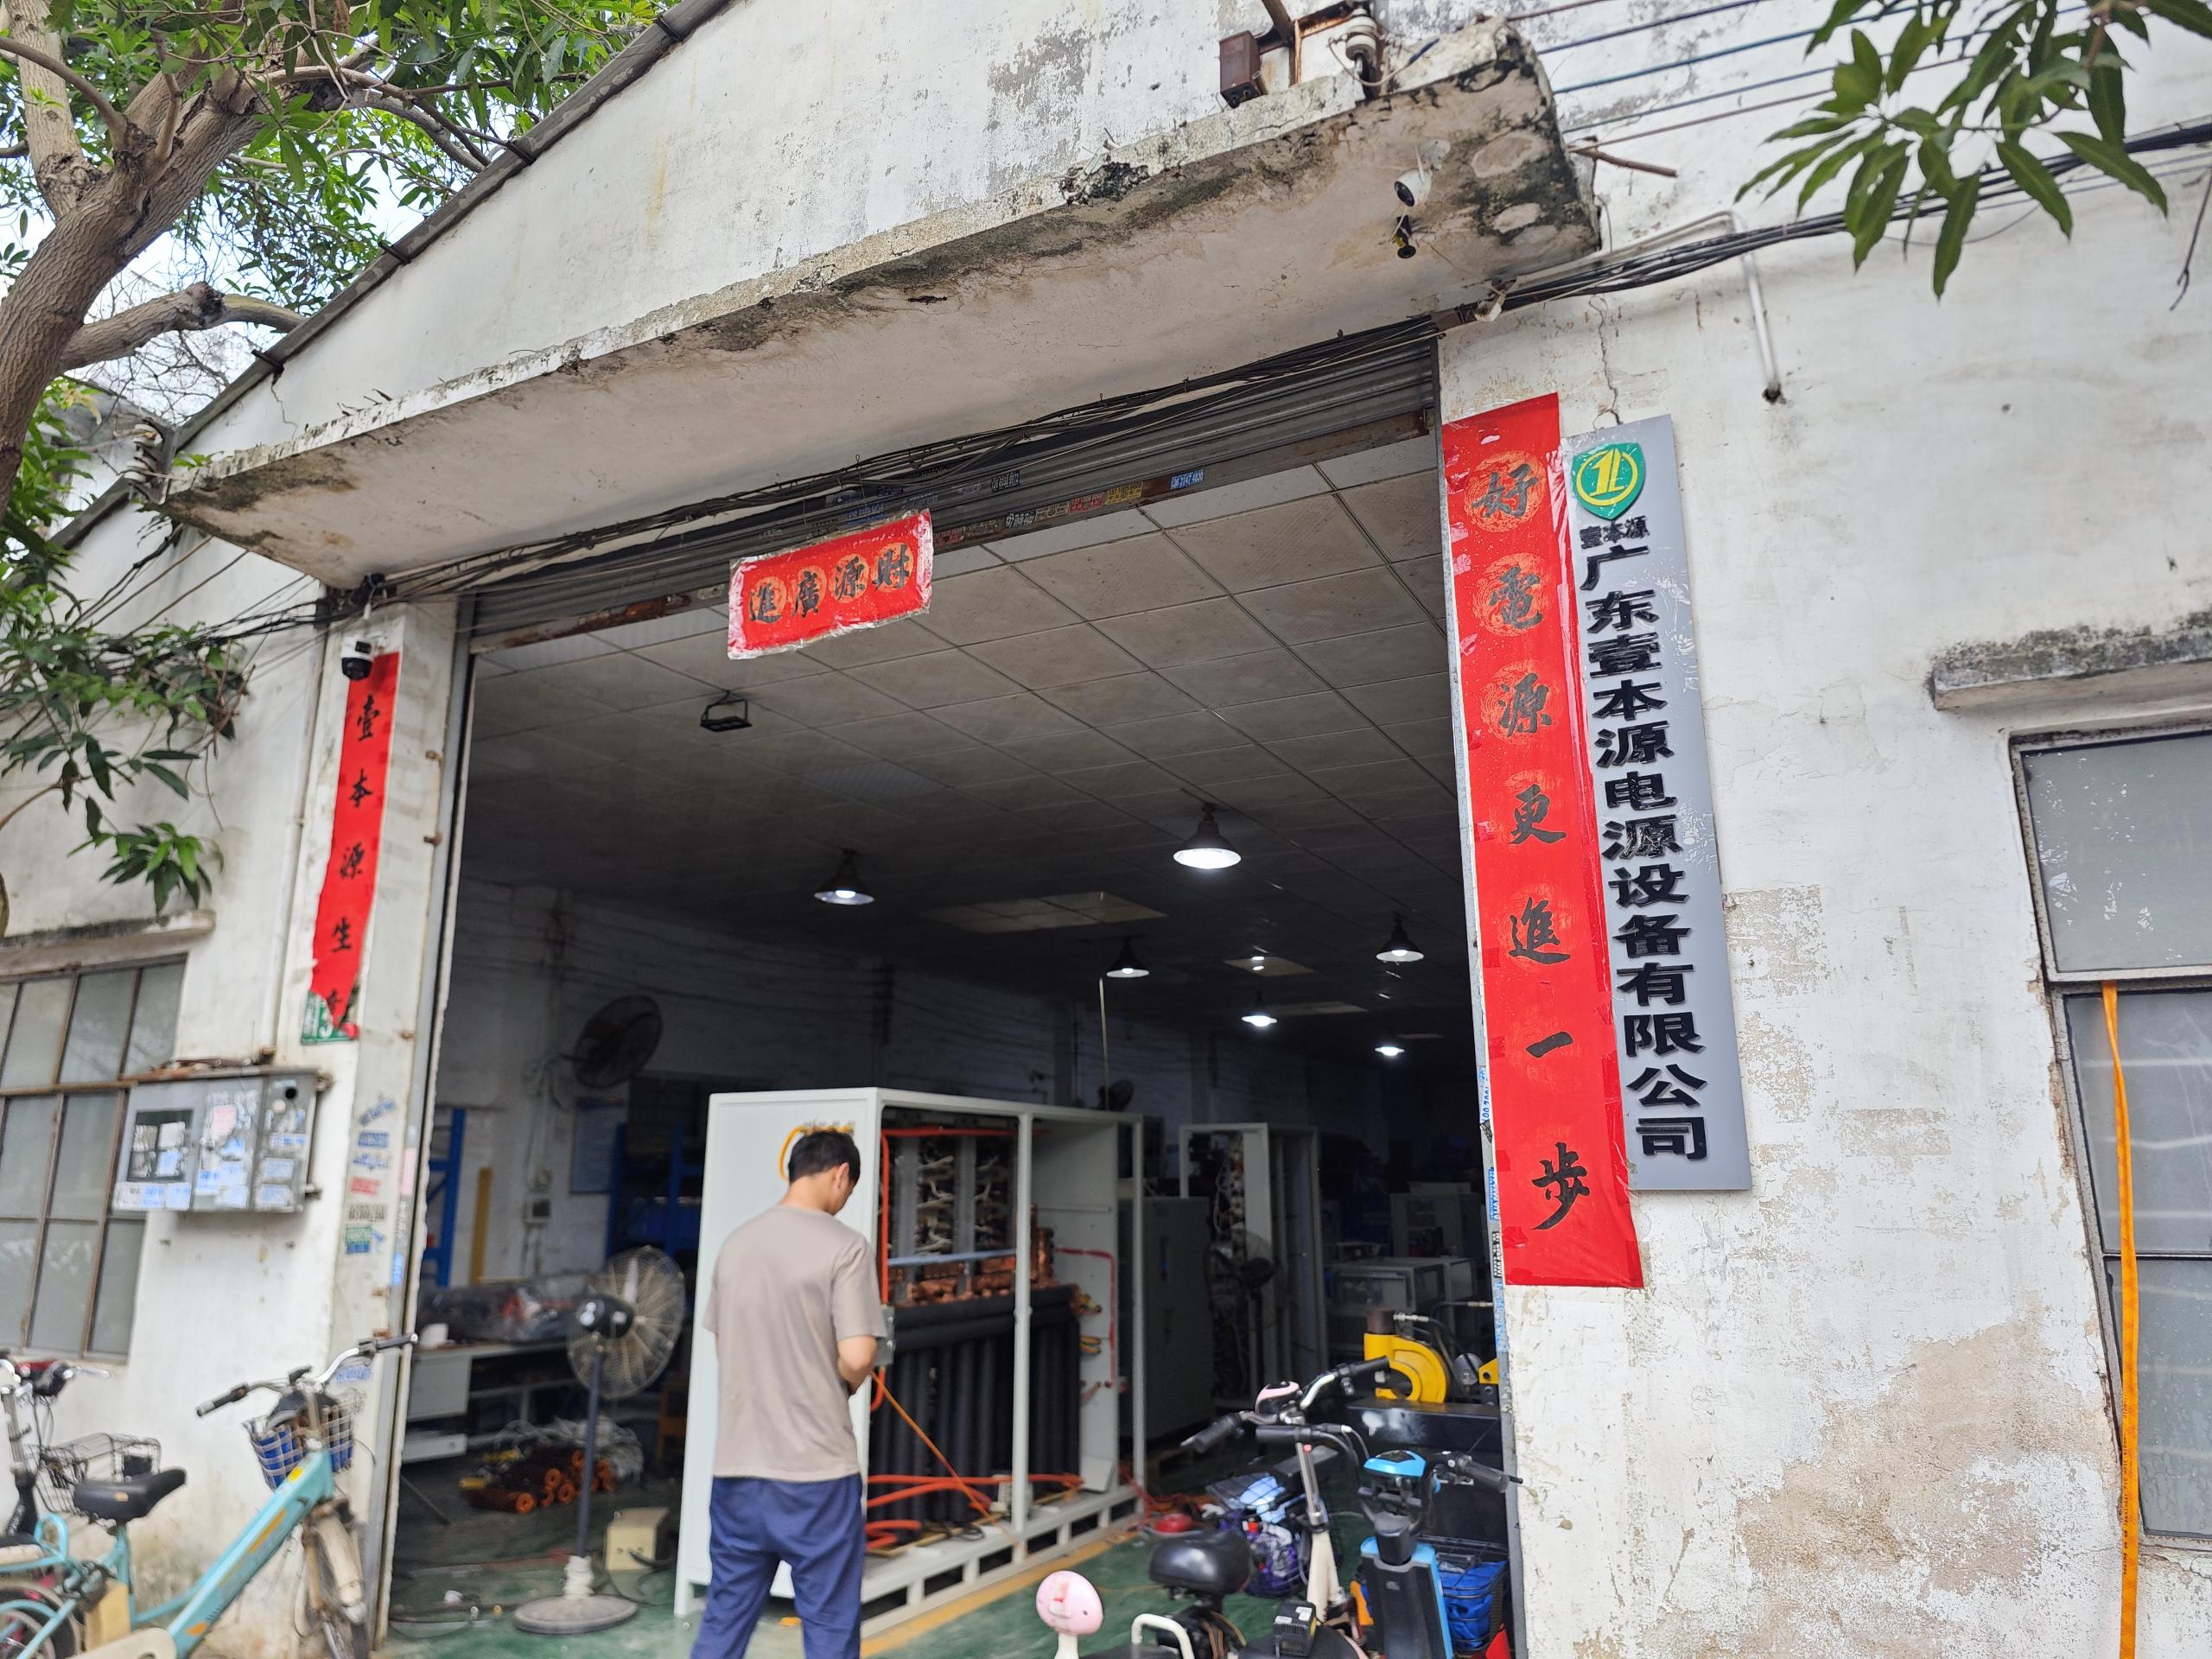
Operating since 2013 from our 3,000 m² production complex in Guangzhou, China. Direct factory engineering without trading-company margins.
Unlike assemblers who outsource structural fabrication, we maintain our own laser cutting, CNC shearing, milling, punching, and tapping facilities. We engineer high-purity T2 electrolytic copper busbars shaped specifically to lower thermal losses and minimize stray electromagnetic fields.
Whether your team in Innsbruck is prototyping a unique pilot electrolysis chamber requiring a non-standard 28V 1500A curve or building a full-scale 24-tank automated electroplating facility, we build single-unit prototypes with zero minimum order quantity penalty.
Every power supply undergoes strict incoming component qualification (utilizing genuine Infineon/Fuji IGBT modules), followed by continuous 8 to 24-hour resistive-load burn-in at elevated ambient temperatures before crating in seaworthy export-grade wooden packaging.




Addressing Austrian electrical compliance, DDP customs logistics, interface integration, and localized operating conditions.
Request an engineered proposal, customized 3D dimensions, and competitive factory-direct pricing tailored to your bath dimensions and production quotas.