Featured Industrial DC Power Systems & Converters for West Midlands Engineering
Factory-calibrated power supplies meeting harmonised EN 61204-3 standards, equipped with MODBUS/RS485 interfaces, forced water/air heat exchanging, and sub-1% current ripple performance.

12V/15V 5000A–6000A 75kW Water-Cooled DC Rectifier
- Topology: High-Frequency IGBT
- Output Range: 0–15V / 0–6000A
- Cooling: Deionised Water-Cooled Loop
- Ripple Factor: ≤ 2% RMS across 100% load

12V 4000A 48kW High-Frequency Plating Rectifier
- Efficiency: ≥ 90% at full rating
- Regulation: CV / CC Auto-Crossover
- Integration: RS485 / Profibus Option
- Protection: Overheat, Phase-Loss, Short

8000A 12V Water-Cooled Continuous Galvanizing Rectifier
- Enclosure: Sealed IP54 Anti-Corrosion
- Cooling: Isolated Copper Heat Sink
- Input Line: 400V 3-Phase 50Hz (UK Standard)
- Duty Cycle: 100% 24/7 Heavy Industrial

100A–3000A Precision Anodic Oxidation DC Rectifier
- Voltage Vector: 12V / 18V / 24V / 60V
- Ramping: Multi-Step Programmable Ramp
- Finish Quality: Hard Anodise & Titanium Spec
- Certifications: CE, LVD, EMC Compliant

800V 50A 20kW Programmable EV Component Test Supply
- Output Span: 0–800V DC / 0–50A
- Dynamics: < 5ms Dynamic Load Step
- Automation: SCPI, CANbus, 0–10V Analog
- Target: Traction Inverter & Battery Testing
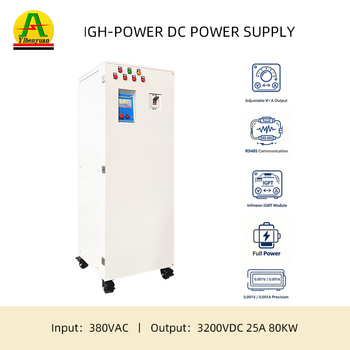
80kW 3200V High-Voltage Capacitor & Plasma DC Supply
- Voltage Ceiling: Up to 3,200V DC
- Precision: ≤ 0.1% Full Scale Accuracy
- Arc Extinction: Ultra-fast Spark Quenching
- Form Factor: Custom 19-inch Heavy Cabinet
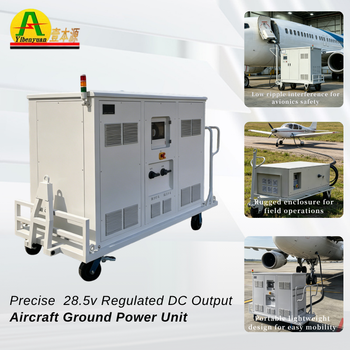
Portable 28.5V DC Aircraft Ground Power Unit (GPU)
- Continuous Load: 300A / 600A Peak Crank
- Standards: DFS 400 & ISO 6858 Compliant
- Construction: Heavy-Duty Mobile Enclosure
- Overload: Up to 2000A Starting Surges
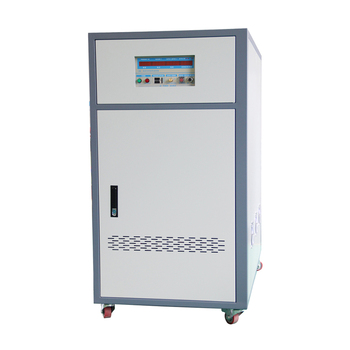
40kVA–500kVA 400Hz Solid-State Frequency Converter
- Input/Output: 50Hz/60Hz Input → 400Hz Output
- Voltages: 115V / 200V AC 3-Phase
- Total Distortion: THD < 2.5% Linear Loads
- Replaces: Rotary Motor-Generators
Engineering customized switch-mode power conversion platforms since 2013 under certified ISO 9001 systems.
Ultra-low ripple, continuous 24/7 duty rectifiers built for electro-winning, chrome plating, and heavy electrolysis.
Precision charging sources, electrostatic precipitation, and electrospinning drivers engineered for tier-1 labs.
Fully tested and verified by TÜV Rheinland for complete compliance with British electrical and safety codes.
Industrial Power Conversion Architecture for Birmingham’s Advanced Manufacturing Corridors
The West Midlands metropolitan county—anchored by Birmingham, Coventry, Solihull, Wolverhampton, and the Black Country—remains the indisputable heartland of the United Kingdom’s automotive manufacturing, aerospace systems design, and precision metal finishing industries. For decades, traditional manufacturing operations in the Jewellery Quarter, Aston, Tyseley, and Minworth relied on legacy oil-cooled silicone-controlled rectifiers (SCR) and bulky 50Hz iron-core step-down transformers. However, as Birmingham accelerates its transition toward modern, high-efficiency factory automation and carbon-neutral production mandates, the performance deficiencies of old thyristor infrastructure—namely poor power factor (0.65–0.75), high harmonic distortion (THD-I > 30%), excessive thermal dissipation, and substantial current ripple—have turned legacy power systems into severe production bottlenecks.
Guangdong Fenvix Technology Co., Ltd. supplies CE-certified, high-frequency Insulated Gate Bipolar Transistor (IGBT) switch-mode DC power systems specifically configured to integrate directly into the British 400V 50Hz industrial grid. By adopting modern PWM (Pulse-Width Modulation) topologies operating at switching frequencies between 20kHz and 40kHz, our power architectures achieve total conversion efficiencies exceeding 90%, near-unity power factor (≥ 0.95), and current ripple factors below 1% to 2% RMS. This level of precise wave manipulation is critical for high-spec surface engineering, e-mobility battery pack thermal burn-in, cathodic electro-deposition (e-coat), and aerospace non-destructive testing lines across the West Midlands.
Information Gain Directive for UK Engineering Teams: In precision electro-deposition and titanium anodic oxidation, current ripple is directly linked to internal stress, grain boundary morphology, and microporosity of the applied film. Replacing antiquated 6-pulse or 12-pulse SCR rectifiers with Fenvix IGBT high-frequency power supplies decreases surface roughness (Ra) by up to 28% while slashing baseline electricity consumption on the factory floor by 15% to 22%.
Localized Application Scenarios Across Birmingham & The Black Country
Automotive & EV Battery Cluster
Operating alongside tier-1 automotive supply networks linked to Jaguar Land Rover (Castle Bromwich & Solihull) and the UK Battery Industrialisation Centre (UKBIC), our programmable DC power racks (0–800V, up to 120kW) deliver the millisecond dynamic step response required for end-of-line battery module cycling, high-voltage traction inverter validation, and regenerative motor dyno test cells.
Aerospace Precision & MRO
Serving high-criticality aerospace machining contractors across the Midlands Aerospace Alliance (MAA) network, our 400Hz solid-state static frequency converters (115V/200V AC) and 28.5V DC Ground Power Units (GPUs) provide stable, pure sine-wave auxiliary power for avionics flight-deck testing, hydraulic actuator calibration, and hangar maintenance without the excessive noise and emissions of combustion engine sets.
Jewellery Quarter & Plating
From the precious metal electroplaters of Birmingham's historic Jewellery Quarter handling micro-layer gold and rhodium immersion, to heavy industrial zinc and hard-chrome lines across West Bromwich and Dudley, Fenvix DC rectifiers (12V–24V up to 15,000A) deliver steady current density control (CC/CV) to eliminate burning, nodule growth, and edge embrittlement.
Every unit destined for delivery to Birmingham is designed with localized operational environmental factors in mind. In electroplating and chemical pickling environments where ambient atmospheres carry acidic vapour droplets (such as hydrochloric, sulphuric, or chromic mists), conventional cooling fans draw contaminants across sensitive circuit boards, causing premature semiconductor tracking and failure. Fenvix resolves this common UK field challenge by building isolated, water-cooled rectifiers inside fully sealed, IP54-rated heavy gauge steel enclosures, venting heat entirely through stainless steel or pure copper plate heat-exchangers connected directly to external plant chilling loops.
Technical Comparison: Switching Topologies for UK Industrial Facilities
When evaluating total cost of ownership (TCO), Birmingham plant engineers must account for both thermodynamic thermal loading and electrical efficiency. The comparative table below outlines the core functional parameters between traditional thyristor hardware and modern Fenvix high-frequency switch-mode platforms.
| Performance Dimension | Legacy Silicon Thyristor (SCR) | Fenvix High-Frequency IGBT | Direct Operational Benefit in Birmingham |
|---|---|---|---|
| Operating Efficiency | 68% – 76% at average loads | 90% – 93% continuous | Cuts plant electrical bill under UK Climate Change Levy (CCL) |
| Output Ripple (RMS) | 5% to > 10% (requires massive chokes) | < 1% to 2% standard | Eliminates microscopic crystal defects in bright nickel/gold deposits |
| Power Factor (cos φ) | 0.60 – 0.78 (variable with firing angle) | > 0.94 at full operational load | Prevents reactive power penalty surcharges from UK grid operators |
| Cooling Footprint | Bulky open-air or massive oil tanks | Compact closed water-loop or ducted air | Up to 60% floor space reduction in crowded urban workshops |
| Transient Response | Slow (100ms – 300ms recovery) | Ultra-fast (< 2ms to 5ms dynamic step) | Prevents voltage collapse during fast-ramping automated E-Coat lines |
| Control & SCADA | Manual potentiometers / crude 0–10V | Digital DSP, RS485, MODBUS-RTU, Profinet | Fully integrated with Siemens, Omron, and Allen-Bradley UK PLCs |
| Standards Compliance | Often non-compliant with harmonic limits | Harmonised EN 61000-6-2/4 & EN 61204-3 | Seamless UKCA / CE declaration of conformity and machine sign-off |
In addition to electroplating, modern cathodic electro-deposition (E-Coat) lines used for automotive sub-frames require highly controlled dual-stage ramping. Fenvix supplies programmable electrophoresis power supplies delivering up to 800V DC at 100A, capable of executing soft-start soft-stop current curves that eliminate pinholes, orange peel texture, and flash burning when components enter the immersion paint bath.
Navigating Net Zero, UKCA Standards & Energy Productivity in the Midlands
British industrial manufacturing is operating under unprecedented structural shifts. The UK government's statutory target of reaching Net Zero carbon emissions by 2050, combined with volatile industrial commercial electricity tariffs across the UK national grid, has rendered energy-intensive manufacturing processes scrutiny targets. Across the Black Country and Birmingham, metal platers, heat treaters, and aerospace machine shops are subject to strict compliance under the Energy Savings Opportunity Scheme (ESOS) and the Streamlined Energy and Carbon Reporting (SECR) framework.
Power supplies represent one of the single largest consumers of incoming active and reactive electrical energy in an electro-chemical plating facility. For instance, running an older 12V 5,000A thyristor-based line for 6,000 hours per year at 72% efficiency dissipates approximately 23.3kW in parasitic heat loss alone. By contrast, replacing that system with a Fenvix water-cooled switch-mode unit operating at 91% efficiency cuts internal power dissipation down to roughly 5.9kW. The resulting net saving—over 104,000 kWh annually per rectifier line—yields a return on capital investment (ROI) that typically amortises within 14 to 22 months under prevailing British enterprise energy tariffs.
UKCA / CE Harmonisation Protocol: Although the UKCA (UK Conformity Assessed) marking is mandatory in Great Britain following post-Brexit regulatory realignments, the UK government has formally extended the recognition of CE marking indefinitely for goods covered by standard electrical safety directives (including the Low Voltage Directive 2014/35/EU and Electromagnetic Compatibility Directive 2014/30/EU). Every industrial power unit exported by Guangdong Fenvix Technology Co., Ltd. is manufactured to harmonised European standards, backed by full technical construction files (TCF), test certificates from accredited test bodies, and a formal Declaration of Conformity.
Furthermore, water conservation directives enforced by Severn Trent Water in the West Midlands have placed intense focus on wastewater remediation and closed-loop process effluent management. Fenvix supports local ecological compliance through our dedicated automatic polarity-reversing DC power supplies designed specifically for electrocoagulation and electrolytic descaling. By programmatically reversing anode and cathode polarities on customisable 4-segment cycles via internal digital timers, our systems actively dislodge lime and heavy-metal scale from electro-flocculation plates, preserving electrode service life and cutting maintenance downtime across Birmingham's industrial treatment facilities.
Why Birmingham Sourcing Managers & Chief Engineers Partner with Fenvix
Unlike trading intermediaries or catalog distributors that re-brand generic commodity chassis, Guangdong Fenvix Technology Co., Ltd. operates an integrated, 3,000-square-meter modern manufacturing facility located in Guangzhou, Guangdong, China. Founded in 2013, we control the entire lifecycle of industrial power conversion: from structural plate shearing, CNC punching, milling, drilling, and busbar bending to PCB surface-mount processing, magnetic transformer winding, assembly, and full load-bank burn-in.
No Minimum Order Quantity
Whether you require a single 1.5kW programmable benchtop DC power source for an advanced prototyping lab at the University of Birmingham or a multi-bay 15,000A water-cooled plating system for a high-volume coil coater in Smethwick, our factory welcomes single-unit orders (MOQ: 1 Set) with complete engineering customisation.
TÜV Rheinland Verified Factory
Our manufacturing site, production management, testing equipment, and export operations have undergone rigorous on-site audit and verification by TÜV Rheinland. We strictly uphold ISO 9001 quality management procedures from incoming component batch inspection (IQC) through finished-product load endurance burn-in.
Seamless UK Logistics & DDP
We manage export consignments across all major Incoterms—including FOB Guangzhou/Shenzhen, CIF Southampton/Felixstowe, or seamless DDP (Delivered Duty Paid) right to your Birmingham factory gate. We handle all export declaration documentation, sea/air shipping, and customs clearance support.
Every Fenvix power system undergoes a minimum 24-hour full-load thermal burn-in test before leaving our factory floor. Using high-precision digital power analyzers, spectrum harmonic probes, and high-bandwidth oscilloscopes, our certified electrical test technicians record voltage ripple, load step overshoot, insulation withstand capability, and temperature rise curves across all semiconductor heat sinks. This verifiable testing documentation is packaged with your equipment, ensuring rapid, painless statutory sign-off by UK factory insurance inspectors and health & safety officers.
Frequently Asked Questions by Birmingham Industrial Procurement Teams
Clear, transparent engineering and commercial guidance addressing import protocols, electrical integration, and technical specifications for UK mechanical, electrical, and plumbing (MEP) engineers.
Do Fenvix industrial power supplies comply with UK grid standards and voltage tolerances?
How does CE certification apply to industrial machinery imported into Birmingham post-Brexit?
What cooling architecture is recommended for high-current plating facilities in the West Midlands?
Can Fenvix rectifiers interface directly with existing UK factory SCADA and PLC control systems?
What is the typical lead time and shipping method for heavy power units delivered to Birmingham?
How do you provide after-sales warranty support, spare parts, and technical assistance for UK facilities?
Ready to Upgrade Your Birmingham Plant’s Power Conversion Systems?
Connect directly with our senior power electronics engineering division. Send us your load ratings, input parameters, duty cycles, and target operational requirements for an expedited technical review, system configuration, and commercial quotation within one business day.