12V 15V 5000A 6000A 75KW Water Cooled Plating Rectifier
- Output Power: 75 kW Constant CV/CC
- Input Rating: 380V / 400V 3-Phase ±10%
- Cooling Design: Deionized Water Chilled
- Digital Interface: RS485 MODBUS-RTU / PLC

Modular switch-mode power topologies engineered with German-imported Infineon IGBT architectures, featuring dynamic low-ripple DC precision, RS485 Profibus connectivity, and forced-air or sealed liquid-cooling designs.
From the high-throughput automotive corridors of Bratislava and Trnava to the heavy electromechanical machinery works of Košice and Žilina, modern Slovak factories require resilient DC power architecture designed for uninterrupted production.
Slovakia leads the world in per-capita vehicle production (Volkswagen, Stellantis, Kia, Jaguar Land Rover). Our 12V–24V / 5,000A–15,000A high-frequency rectifiers deliver ultra-low current ripple (<1%), eliminating micro-porosity in anti-corrosion zinc and electrophoresis coatings across automotive stamping and tier-one chassis fabrication plants.
With Slovakia's rapid electrification pivot in Western and Central regions, battery pack assembly lines in Nitra and Považská Bystrica require precise DC testing. Our programmable 800V–1000V high-voltage power supplies feature dynamic response times below 5 milliseconds and bidirectional safety cutoffs for thermal chamber burn-in and motor drive endurance cycles.
Heavy industry complexes around Košice deploy our industrial switch-mode rectifiers for continuous electro-descaling, titanium alloy anodization, and specialized electrolysis. Engineered with IP54 water-cooled sealed enclosures, our systems isolate internal IGBT modules from corrosive acid mists, airborne metal dust, and ambient industrial humidity.
An in-depth analysis of how technological evolution, ESG regulations, and rising industrial power tariffs are accelerating the shift from legacy thyristor (SCR) rectifiers to high-frequency switch-mode architectures.
Historically, Slovak chemical and electroplating plants relied on oil-immersed 12-pulse or 6-pulse thyristor transformers. While mechanically robust, SCR systems exhibit poor conversion efficiency (72%–78%), low power factor (0.65–0.75), and massive physical footprints. As electricity spot tariffs across Central Europe fluctuate, operational expenditure (OPEX) has become a primary boardroom metric. Transitioning to Fenvix high-frequency IGBT switching technology immediately delivers conversion efficiencies of up to 93%, saving tens of thousands of kilowatt-hours per high-current tank annually.
Operating within the European Single Market, Slovak plant managers face strict liability under EU Directive 2014/30/EU (EMC) and Directive 2014/35/EU (Low Voltage). Industrial rectifiers must not introduce parasitic electromagnetic interference into adjacent computerized CNC, robotics, or optical inspection lines. Fenvix integrates multi-stage LC electromagnetic filters and certified shielding to ensure complete Class A industrial electromagnetic compliance without requiring external line chokes.
With Slovakia's high degree of robotic integration, manual potentiometer control of electroplating and heating rectifiers is no longer acceptable. Modern installations mandate deterministic network integration. Our high-frequency power supplies feature isolated RS485 (MODBUS-RTU), Profibus-DP, and analog 0–10V / 4–20mA interfaces as standard, feeding real-time current density, voltage ramp curves, and thermal alerts directly into central SCADA and Siemens SIMATIC PLC architectures.
Unplanned line stoppage in automated stamping or surface treatment represents enormous financial losses. Slovak procurement engineers increasingly specify modular N+1 hot-swappable or parallel-running power modules. If an individual 1,000A sub-rack encounters a thermal or power fault, the master system throttles gracefully without dropping the batch, allowing maintenance technicians to service components without draining plating chemistry.
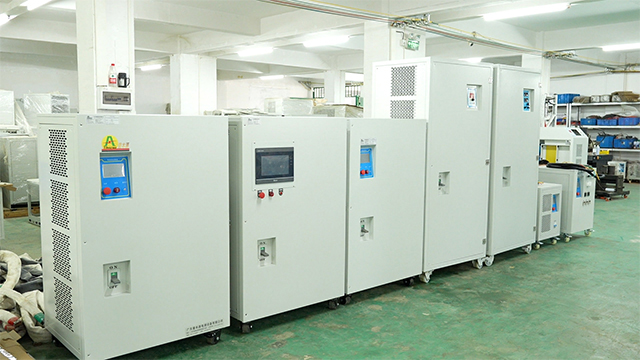
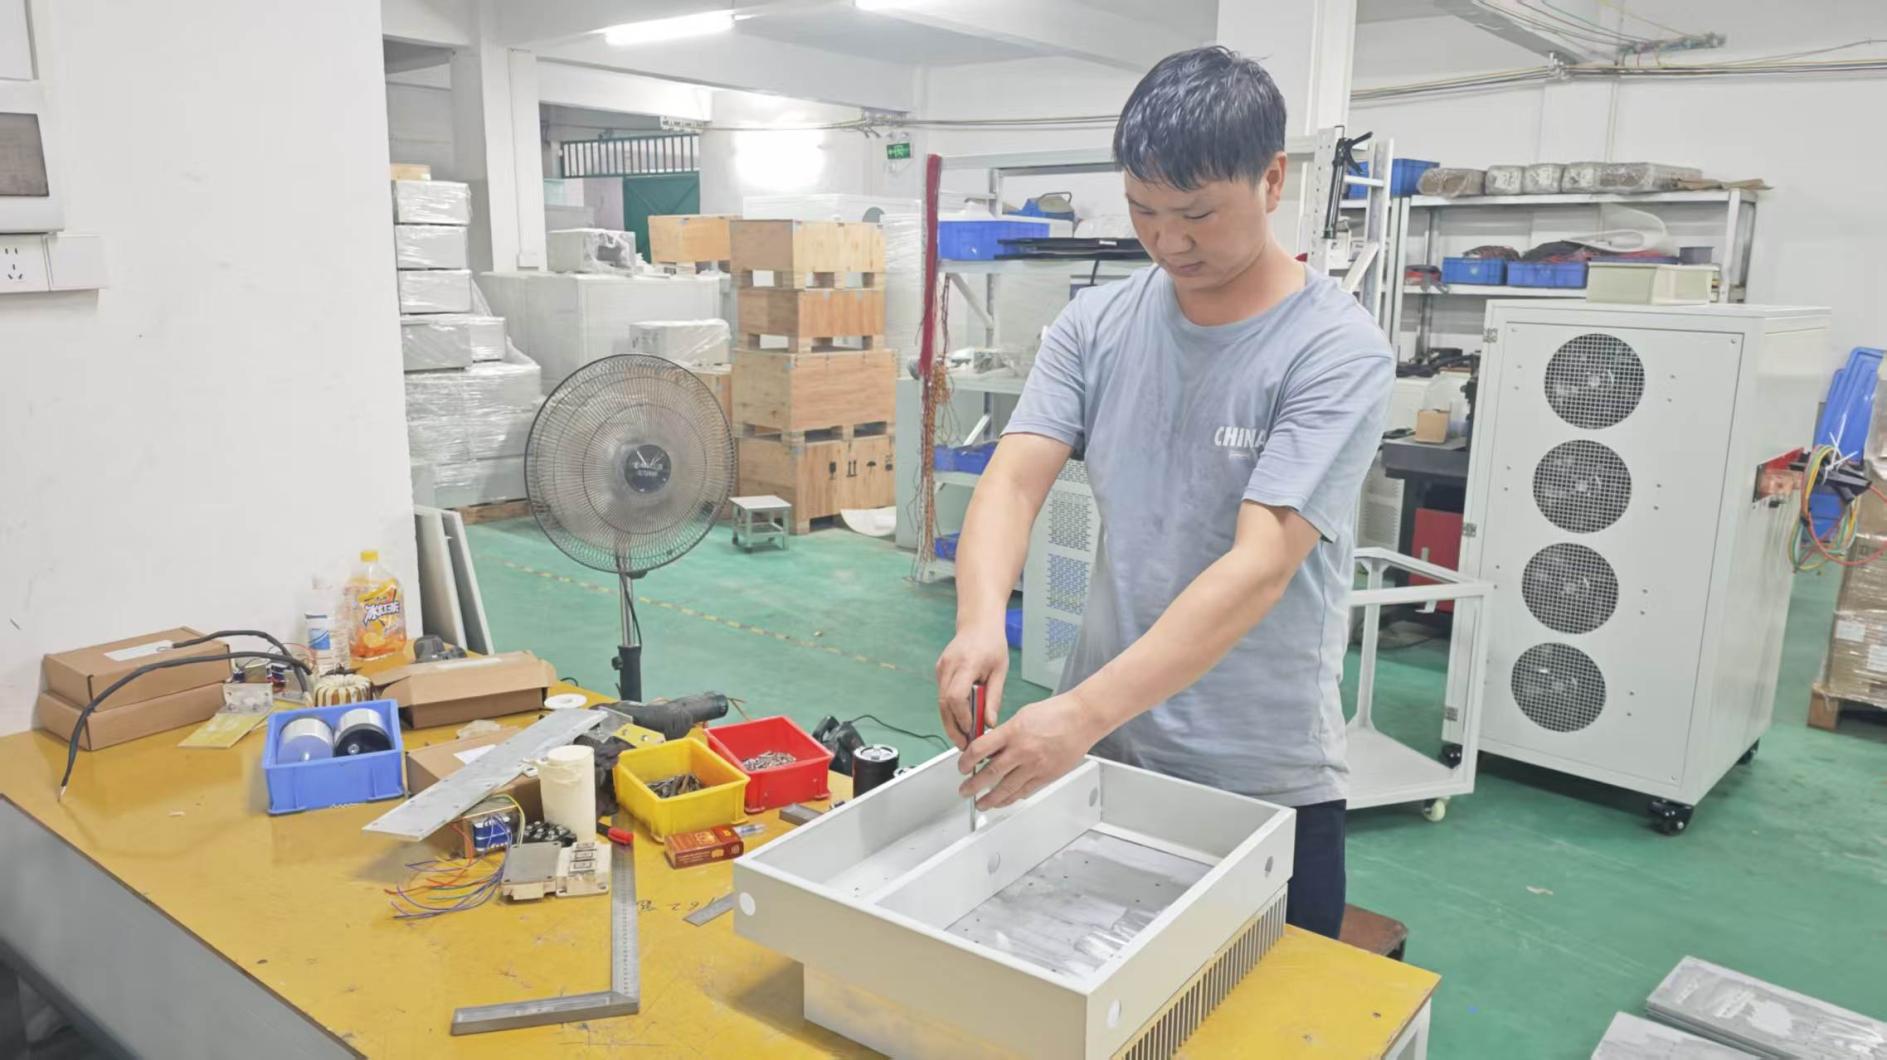
Unlike export trading agencies, Fenvix maintains full-cycle internal production across 3,000 m² of precision manufacturing facilities in Guangdong, China. We control mechanical cabinet punching, heavy-gauge copper busbar silver plating, SMT printed circuit board assembly, and 100% full-load thermal burn-in.
Senior power electronics engineers analyze bath chemistry, line duty cycle, harmonic requirements, and Slovak plant ambient ratings to determine exact IGBT sizing and cooling headroom.
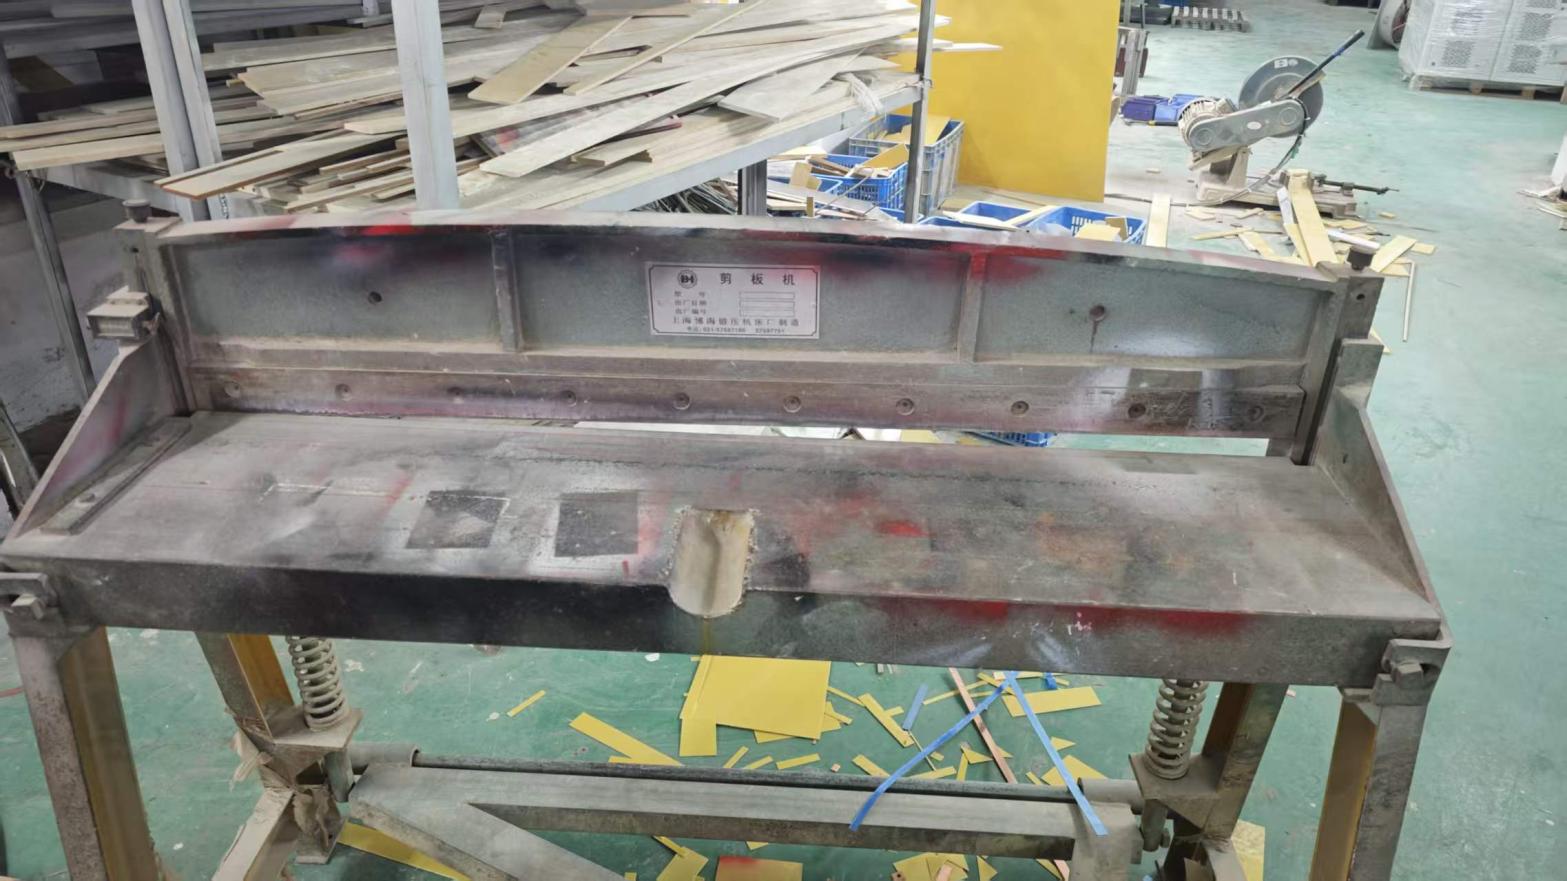
Plate shearing, automated turret punching, and milling of heavy copper conductor busbars ensure minimal contact resistance and maximum mechanical cabinet structural rigidity.
Control boards undergo automated SMT mounting followed by anti-corrosion, moisture-proof, and anti-acid polyurethane conformal triple-coating for harsh chemical environment survival.
Every power supply is coupled to high-power resistive loads and subjected to 72 hours of uninterrupted burn-in at full rated current, monitored by digital oscilloscopes and infrared thermography.


Every system shipped to Slovakia is accompanied by comprehensive CE Declaration of Conformity and Factory Inspection Records.


Essential answers regarding CE compliance, grid synchronization, DDP customs logistics into Slovakia, and long-term technical reliability.
All Fenvix power supplies supplied to European Union member states adhere strictly to the Low Voltage Directive (LVD 2014/35/EU) and Electromagnetic Compatibility Directive (EMC 2014/30/EU). Units bear genuine CE marks backed by independent third-party laboratory test reports. Galvanic safety isolation exceeds 3.5kV AC between the primary high-voltage utility stage and secondary low-voltage DC bus, guaranteeing complete worker safety and protection of sensitive line instruments.
Yes. Our digital control boards come natively equipped with optically isolated RS485 serial communication using standard MODBUS-RTU protocol. We provide full register memory mapping tables for rapid PLC programming. Optional Profibus-DP, Profinet, CANopen, or simple 0–10V / 4–20mA analog remote cards can be factory-fitted to interface with existing SCADA control desks across Slovak manufacturing lines.
For installations in Slovak plating shops operating above 3,000A continuous load, closed-circuit water cooling is strongly recommended. Water cooling enables a completely sealed IP54 cabinet, keeping toxic sulfuric, hydrochloric, or chromic acid mists away from sensitive power semiconductors and driver electronics. For clean testing laboratories, EV burn-in benches, or sub-2,000A currents, our high-flow forced-air configurations provide exceptional cooling with simplified installation.
We provide full multimodal export terms including EXW, FOB (Shenzhen/Guangzhou), CIF (Koper / Hamburg / Gdańsk), and complete DDP (Delivered Duty Paid) directly to your factory dock in Slovakia. Air freight transit is approximately 5–8 business days, while cost-effective rail freight (China-Europe Railway Express) or sea-rail intermodal routes deliver within 28–35 calendar days with all EU customs clearance and VAT paperwork handled smoothly.
We maintain a strict No Minimum Order Quantity (MOQ = 1 Unit) policy, allowing Slovak engineers to order single units for pilot automation trials, R&D laboratories, or custom retrofit prototypes. Customized power systems (bespoke voltage ranges, special physical dimensions, pulse frequencies) typically ship within 15–20 working days from final mechanical drawing approval.
All industrial systems come with an 18-month comprehensive factory warranty. In addition to supplying a complimentary emergency spare parts kit (IGBT drivers, firing cards, sensors) with larger orders, our technical support engineers are available via 24/7 digital channels for remote diagnostic assistance and wiring guidance. Field-replaceable modular sub-racks can be swapped in under 20 minutes to prevent line downtime.