[email protected]
ISO 9001 Certified Manufacturer Exporting to 4 Continents

CE Certified Burn In Test Power Supply Factories & Exporter in Novi Sad

High-Frequency Programmable DC Rectifiers, Heavy-Duty Burn-In Test Systems & Aviation Load Solutions Engineered for Autonomous Province of Vojvodina Industrial Tech Hubs

Industrial White Paper & Sourcing Directive

Engineering Reliable Thermal Stress & Electrical Burn-In Power in Novi Sad

As Novi Sad solidifies its position as Serbia’s leading research, automotive development, and electrical manufacturing corridor—anchored by the Science and Technology Park Novi Sad (NTP), the University of Novi Sad Faculty of Technical Sciences (FTN), and rapid expansions across the Sever 4 and Radna Zona Sever economic estates—the demand for precision-grade, CE-compliant burn-in and lifetime endurance testing systems has escalated. Guangdong Fenvix Technology Co., Ltd. delivers high-frequency, IGBT-based adjustable switching DC power supplies engineered specifically to meet the continuous duty requirements (24/7/365) of European Tier-1 automotive electronics suppliers, power semiconductor fabricators, and telecommunication hardware assemblies.

Strategic Alignment with Serbian & European Standards

All export configurations delivered into the Novi Sad and wider South Bačka district undergo rigorous pre-shipment validation under our ISO 9001 certified and TÜV Rheinland on-site inspected facility. Units feature full conformity with EU Low Voltage Directive (LVD 2014/35/EU), Electromagnetic Compatibility (EMC 2014/30/EU), and RoHS 2011/65/EU directives, guaranteeing low harmonic feedback into local utility feeds (EPS distribution network) and seamless integration into SCADA, Profinet, and Modbus-automated production lines.

13+
Years Engineering Expertise
0–100kV
Adjustable DC Range
Up to 15,000A
High-Current Plating & Test
TÜV / CE
Factory & Model Verified
Factory Direct Sourcing

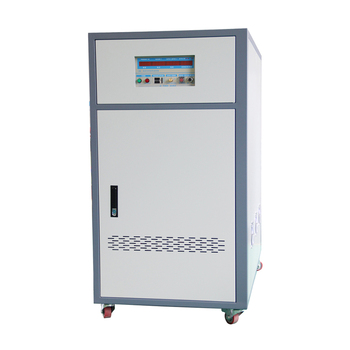
Featured Burn-In & Industrial DC Power Systems for Novi Sad

Factory-calibrated power supplies configured for component stress screening, high-voltage aging benches, electrochemical plating, and continuous testing lines.

Operational Environments

Localized Application Scenarios across Novi Sad’s Industrial Zones

Analyzing the exact production criteria in Sever 4, Kać, Rimski Šančevi, and Bačka Palanka manufacturing clusters.

Tier-1 Automotive Component Burn-In

Novi Sad houses prominent automotive engineering operations specializing in motor controllers, onboard chargers (OBC), and wiring harnesses. During elevated temperature burn-in testing (HTOL - High Temperature Operating Life), power supplies must deliver ultra-stable current under fluctuating thermal ambient conditions up to 55°C without thermal derating or premature safety tripping.

  • Zero-voltage drift across 168-hour endurance cycles
  • Galvanic isolation preventing transient surges between racks
  • Dual constant voltage/constant current (CV/CC) transition

Power Semiconductor & Inverter Stress

With research initiatives at FTN Novi Sad driving power electronics innovation, test benches require fast rise-time programmable DC sources. When evaluating SiC and GaN MOSFET switches, our 800V–2000V DC switching modules allow programmable step slopes, voltage ramp cycling, and millisecond-level overcurrent clamping to avoid damaging prototype wafer lots during avalanche stress runs.

  • Programmable slew rates for di/dt and dv/dt testing
  • Internal memory buffers for custom stress sequence loops
  • Low output capacitance for ultra-fast voltage drop-off

Harsh-Environment Metal Finishing & Anodizing

Vojvodina’s heavy machinery and agricultural equipment fabricators depend on high-durability surface coatings. Fenvix water-cooled rectifiers operate inside fully sealed NEMA 4X / IP54 equivalent steel enclosures, entirely isolating internal IGBT modules and copper planar buses from ambient acidic vapors, hydrochloric mist, and airborne conductive dust common to electroplating plants.

  • Zero ambient airflow drawn across internal electronics
  • Corrosion-resistant titanium or 316L stainless heat exchangers
  • Forward/reverse automated polarity commutation with cycle timers
Regional Market Analysis

Industrial Modernization Trends in Vojvodina's Manufacturing Sector

Navigating the transition toward high-efficiency power electronics, energy optimization, and Industry 4.0 integration.

The manufacturing ecosystem in Novi Sad is undergoing a profound structural upgrade. Historically centered around agro-processing and light mechanical assembly, the capital of Vojvodina has transformed into an epicenter of foreign direct investment (FDI) from Germany, Japan, Switzerland, and Austria. This industrial re-orientation has generated three critical shifts impacting test engineering and power equipment procurement:

1. Transition from Obsolete Thyristor (SCR) Rigs to High-Frequency IGBT Topologies

Older workshops across Novi Sad’s older industrial corridors frequently operate legacy silicon-controlled rectifier (SCR) sets. While rugged, these units exhibit poor efficiency (often below 72%), high displacement factor, and substantial ripple (exceeding 5% without bulky LC filter banks). Modern quality standards—such as ISO/TS 16949 for automotive validation—strictly prohibit excessive output ripple because it distorts component thermal curves during accelerated lifetime screening. Fenvix switch-mode rectifiers operate at 20kHz–50kHz switching rates, achieving efficiency figures above 90% while slashing physical cabinet footprint by up to 65%.

2. Stringent Energy Efficiency and Harmonic Distortions Mandates

With electricity tariffs rising across Southeast Europe and stricter EPS enforcement of grid harmonic limits (standard EN 61000-3-12), plant engineers cannot afford poor power factor equipment that incurs grid penalty tariffs. Fenvix programmable systems are engineered with active power factor correction (PFC ≥ 0.98) and low harmonic distortion topologies (THD < 5%), safeguarding facility power distribution from voltage sags, neutral line overheating, and inductive interference on neighboring automated PLCs.

3. Complete Automation & Digital Telemetry Protocol Standardization

Manual knob adjustments are being eliminated in favor of digitized, unattended burn-in testing chambers. Factories along the Novi Sad-Subotica industrial artery require power sources that integrate immediately into LabVIEW environments, Siemens Step 7 architectures, and custom Python data loggers. Standardizing on RS485 (Modbus RTU), isolated 0–5V/0–10V analog signals, and Ethernet-ready protocols allows plant supervisors to log voltage, current, and chamber status directly into enterprise MES databases.


Performance Parameter Legacy SCR / Thyristor Rectifier Fenvix High-Frequency IGBT Supply Impact on Novi Sad Testing Plants
Operating Efficiency 70% – 76% 90% – 93% Lowers thermal room load; saves 18–22% kWh per test bank
Output Ripple Factor ≥ 5% RMS (standard) ≤ 1% – 0.2% RMS Guarantees true component thermal stress; eliminates fake failures
Enclosure Protection Open Louver / IP20 Air Sealed IP54 / Water-Cooled Survives corrosive industrial atmospheres without PCB corrosion
Dynamic Slew Rate Slow (> 150ms response) Fast (< 5ms step response) Essential for rapid automotive load-dump and cyclic testing
CE Compliance Rigor Self-declared baseline CE / LVD / EMC + TÜV Audited Simplifies EU safety audits and workplace safety (ZNR) protocols
Procurement Engineering Matrix

How to Size Your Burn-In Test Power Supply

Step-by-step engineering calculation to avoid undersizing power stages or overpaying for cooling overhead.

Step 1: Calculate Duty Load Margin

Burn-in testing operates at uninterrupted full load for 24 to 240 hours. Sizing calculations must not plan operation at 100% rated capacity. Always apply a 20% continuous duty derating margin:

Rated Current (A) = (Max Load Current * 1.25)
Rated Voltage (V) = (Max Component V * 1.15)

This buffer guarantees long IGBT life and prevents thermal tripping in non-air-conditioned factory zones in summer.

Step 2: Thermal Management Selection

Evaluate your facility infrastructure before specifying air or water cooling:

  • Forced Air Cooling: Best for R&D benches ≤ 30kW with clean ambient airflow below 35°C.
  • Closed Water Cooling: Mandatory for total power > 50kW, high-dust areas, or testing labs where acoustic fan noise must remain < 65 dBA.

Fenvix supplies matched stainless-steel heat exchangers with inlet/outlet temperature interlocking.

Step 3: Signal & Rack Integration

Prevent ground loops and control signal interference in multi-channel rack arrays:

  • Select Optically Isolated RS485 or Ethernet interfaces to protect supervisory PCs from ground offset.
  • Incorporate remote voltage sensing lines (Sense + / Sense -) to compensate for voltage drop across long test chamber bus lines.

Fenvix control boards feature standard 1.5kV optical isolation across all logic and measurement outputs.

Manufacturing Integrity

In-House Manufacturing: From Copper Busbars to Full Load Testing

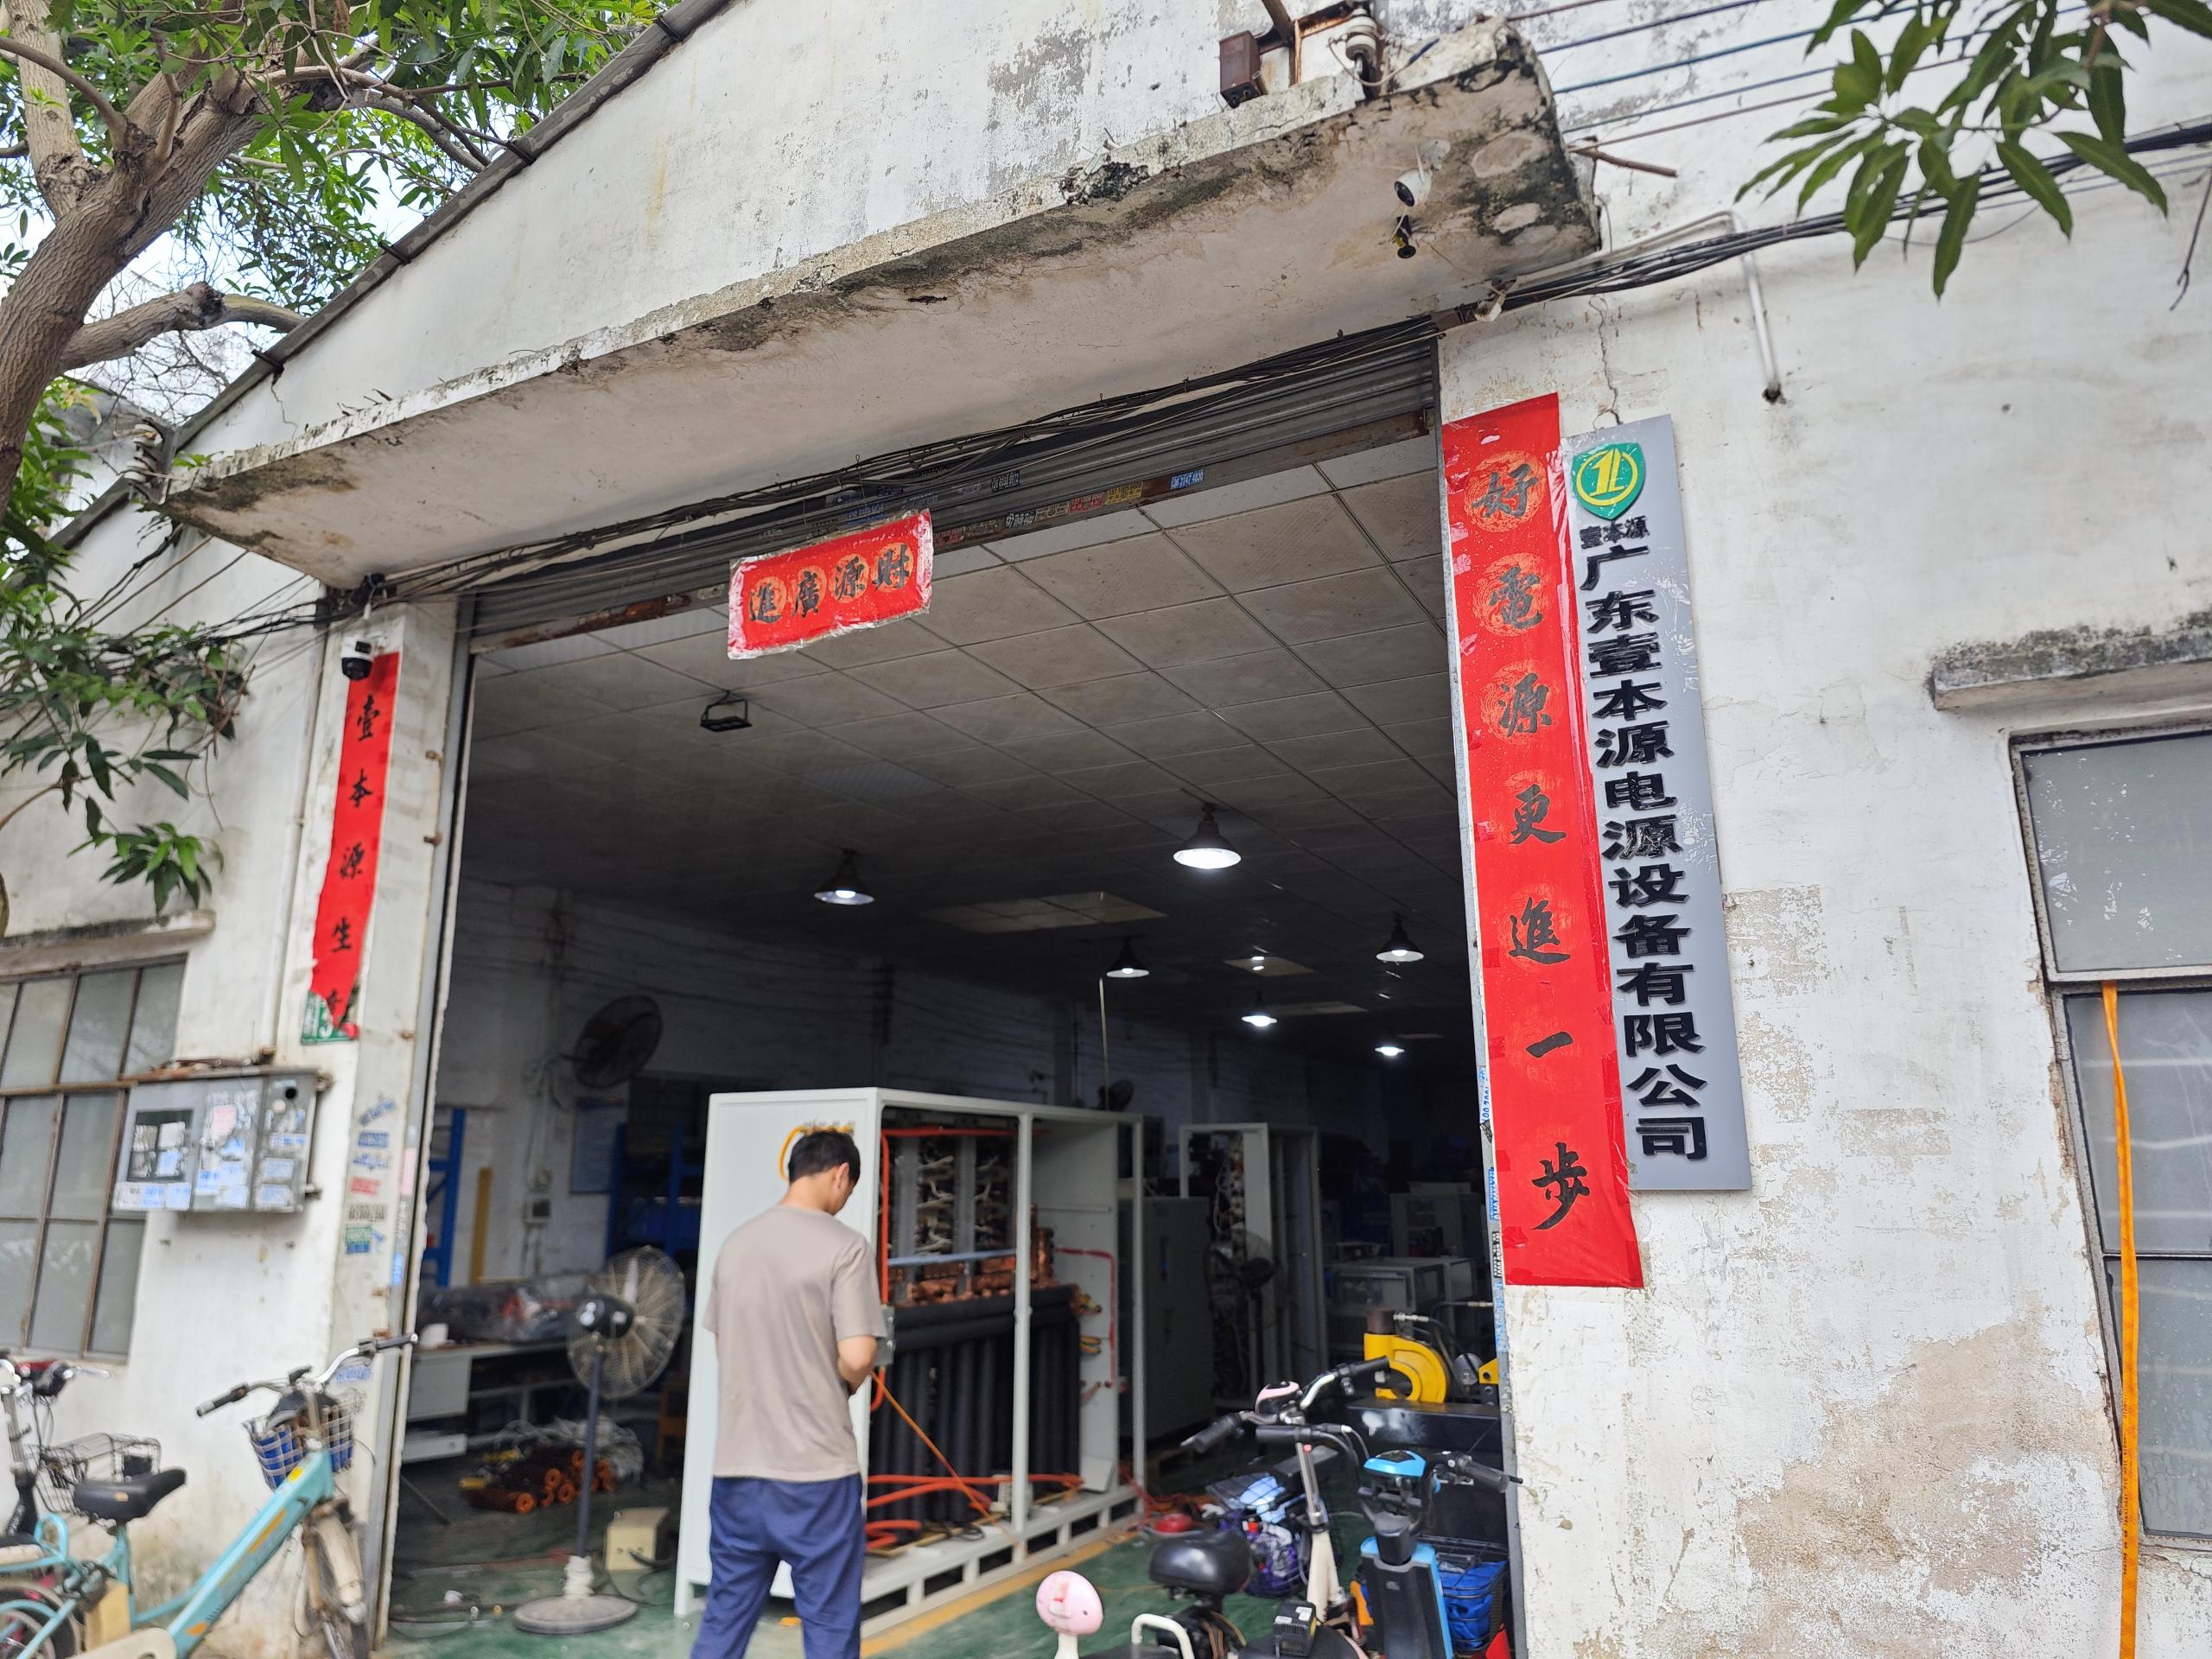
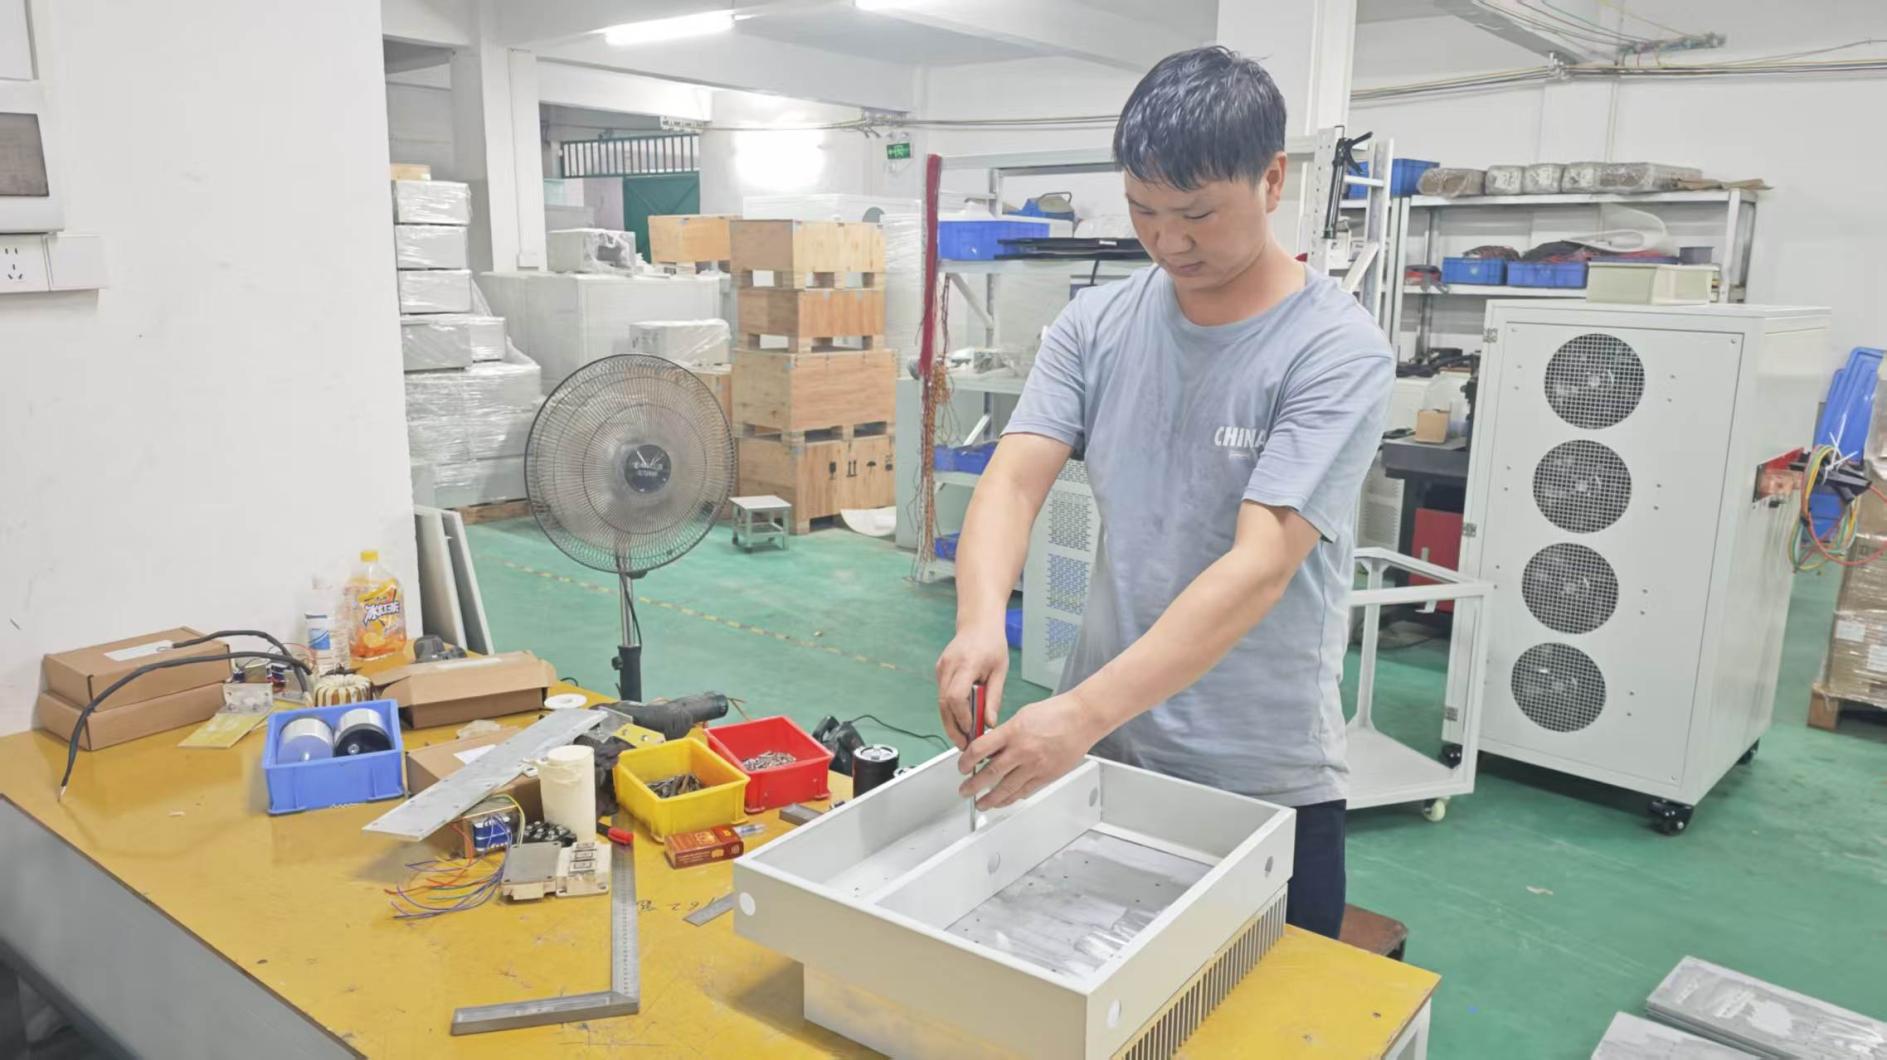
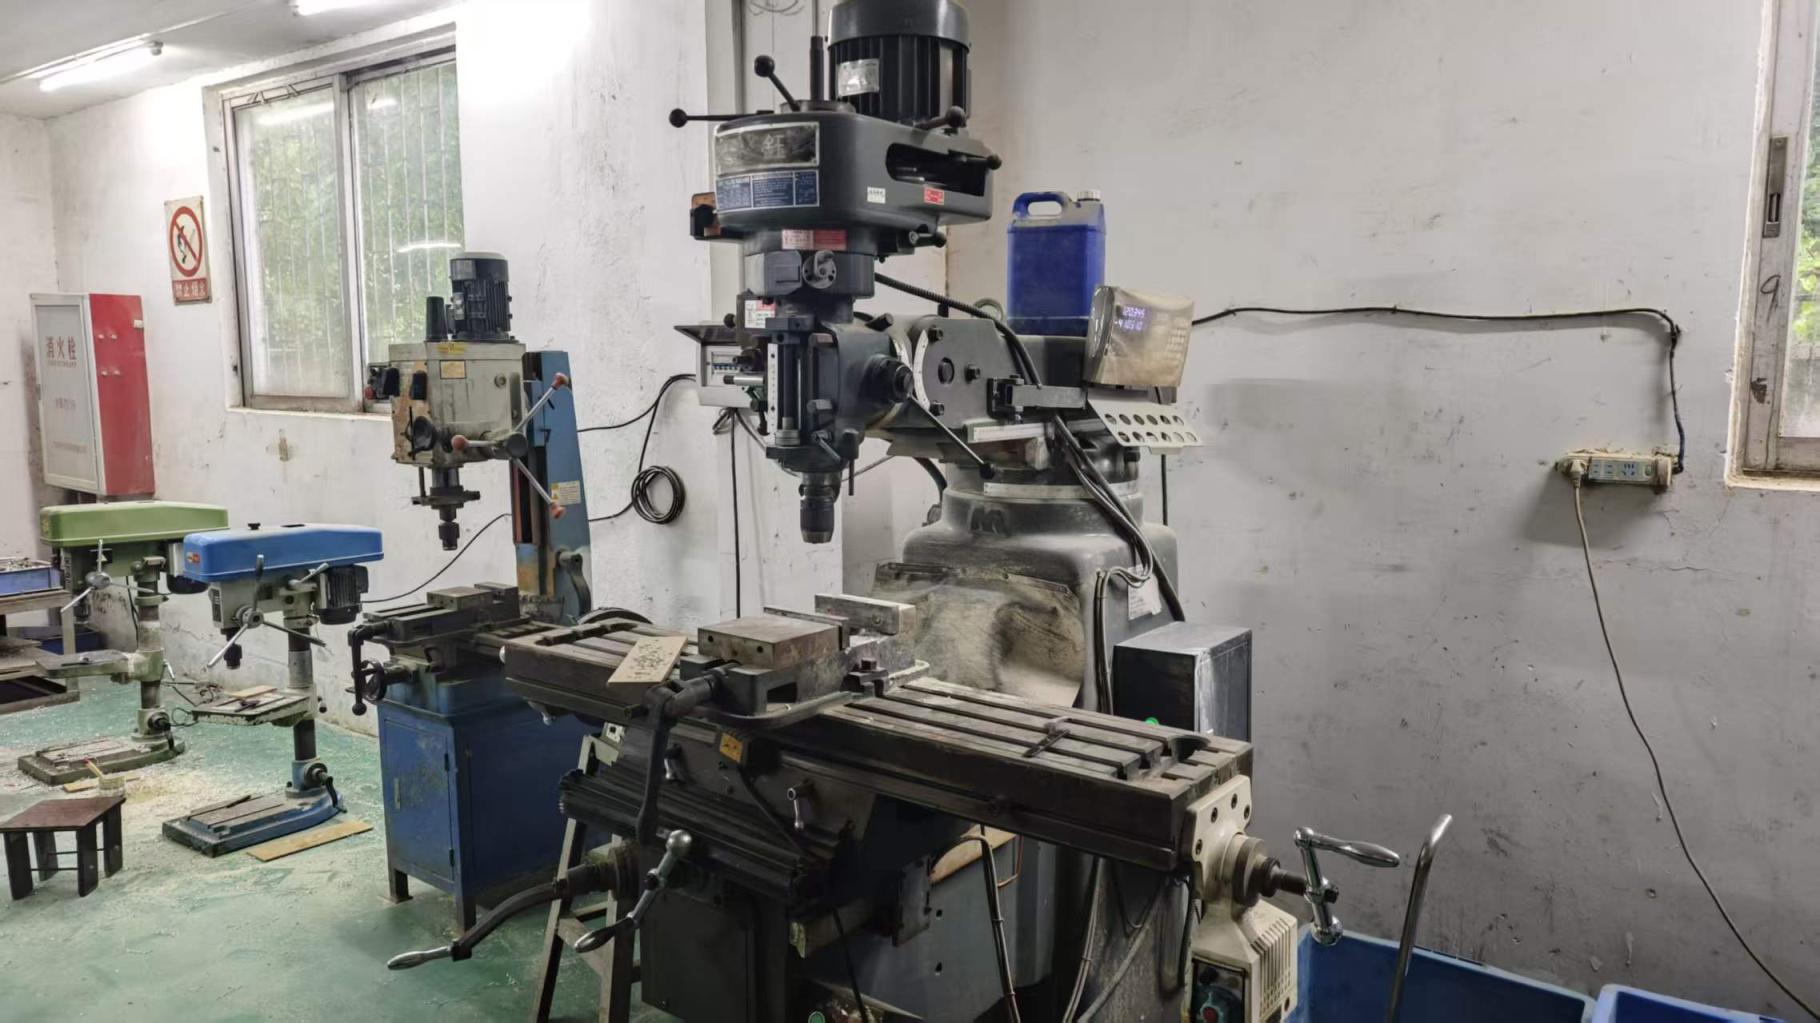
Guangdong Fenvix maintains 100% internal control over sheet metal machining, copper milling, electronic assembly, and pre-export load testing.

Guangdong Fenvix Technology Co., Ltd. modern production workshop in Guangdong

Direct Factory Execution Eliminates Intermediary Risks

Unlike commercial exporters who rebrand generic chassis, Fenvix controls every tier of production in our 3,000 m² factory in Guangdong. Our CNC shearing, punching, and milling machines fabricate custom heavy-gauge enclosures tailored to your facility dimensions. Heavy electrolytic copper busbars are silver- or nickel-plated in-house to minimize junction contact resistance and avoid hotspots during multi-day high-current burn-in runs.

01.
Material Verification: 100% incoming inspection of Infineon/Fuji IGBT modules, TDK capacitors, and nanocrystalline magnetic cores.
02.
100% Full Load Burn-In: Every unit is tested on an inductive/resistive load bank at maximum capacity for 24–72 hours prior to crating.
03.
Oscilloscope & Ripple Proof: Every shipment includes an individualized calibration sheet, harmonic printout, and CE conformance docket.
The Fenvix Advantage

Why European Plant Managers & Sourcing Officers Partner with Fenvix

Over a decade of solving non-standard industrial challenges where catalogue power supplies fall short.

Strict OEM / ODM Non-Standard Sizing

Whether you require a low-voltage high-current 12V/6000A setup, an ultra-compact 19” sub-rack chassis, or a massive 100kV capacitor charging installation, our team configures power stages directly to your physical spatial constraints and thermal cooling infrastructure without high engineering redesign surcharges.

No Minimum Order Quantity (MOQ: 1 Set)

We understand the prototyping demands of universities, research laboratories, and pilot automotive lines in Vojvodina. We accept single-unit orders for specialized testing rigs while retaining the manufacturing capacity and 50+ qualified supplier chain to deliver repeat multi-cabinet production orders.

Verified Compliance & On-Site Audits

Our production plant operates under a certified ISO 9001 Quality Management System and has been comprehensively audited on site by TÜV Rheinland. Products are certified under CE (LVD & EMC) and RoHS standards, giving Serbian customs clearance brokers and corporate safety auditors complete peace of mind.

CE Certified RoHS Compliant LVD Directive EMC Directive TÜV Rheinland Verified Factory
Procurement FAQ

Frequently Asked Questions by Industrial Buyers in Novi Sad

Addressing import logistics, grid compliance, technical parameters, and on-site integration in Serbia.

How do Fenvix burn-in power supplies comply with the local 400V 50Hz grid in Serbia?
All three-phase power supplies exported to Serbia are natively configured for 3-phase 380V/400V/415V AC ±10%, 50Hz standard grid inputs. Internal soft-start circuitry prevents severe inrush current upon energization, ensuring your plant circuit breakers (such as Schneider or ABB Type D curve breakers) do not experience nuisance trips during mass system startup.
What documents and CE certifications are provided for Serbian customs clearance?
Every shipment arrives with complete English documentation, including EU Declarations of Conformity under the Low Voltage Directive (LVD 2014/35/EU) and Electromagnetic Compatibility (EMC 2014/30/EU), an individualized factory load test report (with ripple and harmonic data), schematic wiring prints, and an operation/maintenance manual. This documentation package enables your local customs broker in Novi Sad or Belgrade to clear customs smoothly without administrative delays.
What specific technical data is needed to configure a custom burn-in power supply?
To ensure correct sizing, please specify: (1) Main input voltage and phase; (2) Required output voltage and current ranges; (3) Desired operational mode (Constant Voltage, Constant Current, or programmable multi-step profiles); (4) Allowable voltage/current ripple percentage; (5) Ambient operating temperature and available cooling mechanism (forced air or chilled water); (6) Digital control protocol (RS485 Modbus RTU, 0–10V analog, Profinet, etc.).
What trade terms (Incoterms) and payment methods are available for Serbian companies?
We routinely ship under CIF or CFR terms (Port of Bar, Montenegro; Port of Rijeka, Croatia; or Port of Koper, Slovenia) with forwarding directly into Novi Sad. Air freight is available to Belgrade Nikola Tesla Airport (BEG) for urgent prototypes. We also handle EXW, FOB, and DDP shipments. Payments are accepted via Telegraphic Transfer (T/T), Letter of Credit (L/C), and major global currencies including EUR, USD, and CNY.
How is warranty coverage and technical assistance delivered for overseas installations?
We provide a comprehensive 12-month factory warranty backed by direct remote engineering assistance via video conferencing, email, and instant messaging. In case of field component issues, pre-tested replacement control boards or IGBT driver modules are dispatched via DHL/FedEx within 48 hours. Our facility has also undergone independent third-party verification confirming our capacity for overseas technical guidance.
Why choose a water-cooled rectifier over an air-cooled unit for industrial aging?
In industrial settings where corrosive fumes, metal shavings, or chemical vapors are present—or in enclosed testing cleanrooms where fan acoustic noise is unacceptable—closed-circuit water cooling offers superior reliability. Water-cooled units feature a fully sealed IP54/NEMA 4 cabinet. Heat is transferred out of the cabinet via a liquid loop, preventing dust accumulation on high-voltage circuit traces and significantly extending IGBT operating lifespan.
Custom Engineering Request

Ready to Configure Your Burn-In Power System?

Send your voltage, current, and chamber specifications to our senior power engineering team. Receive an engineering proposal and quote within one business day.

Inquire Now