






1. Technical Whitepaper: Anodizing Rectification Architecture for Mitrovica's Metallurgical Operations
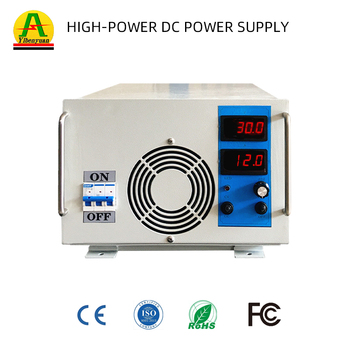
Mitrovica holds an established industrial legacy centered on mining, non-ferrous metallurgy, and alloy processing, anchored geographically by the Trepča industrial basin. As local engineering firms and contract coating facilities transition from legacy, energy-intensive silicon-controlled rectifiers (SCR/Thyristor systems) to modern high-frequency Switch-Mode Power Supplies (SMPS), the necessity for reliable anodizing rectifier manufacturers & factories for Mitrovica has increased significantly.
Anodic oxidation demands exceptional control dynamics. Aluminum anodizing (whether architectural Type II or engineering hard-coat Type III under MIL-A-8625 specifications) requires the precise synthesis of constant current (CC) ramps, voltage step-up control, and negligible AC ripple. When DC ripple factors exceed 5%, local workshops experience structural defects in the micro-porous barrier layer, inconsistent dye absorption, and burning on edge geometries caused by local current concentration. Fenvix integrates high-frequency insulated-gate bipolar transistor (IGBT) topologies coupled with nano-crystalline magnetic cores, driving output ripple below 2% across 10% to 100% duty windows. This precise dynamic response maintains an ideal current density across large batch tanks, irrespective of bath conductivity variations.
Engineering Note on Power Efficiency: Legacy thyristor equipment common across historic Balkan processing facilities typically operates with an electrical conversion efficiency between 68% and 75%, generating excessive heat and poor power factors. Modern IGBT anodizing rectifiers deliver conversion efficiencies ≥90%, directly reducing local electrical consumption in high-amperage installations.
2. Localized Industrial Application Scenarios in Northern Kosovo
The industrial landscape in Mitrovica and surrounding technical centers demands specialized electrical power equipment tailored to varied electrolytic environments:
Heavy Architectural Extrusion & Building Profiles: Anodizers supplying construction materials across the region require 12V–24V continuous-duty DC power supplies with capacities spanning 2,000A to 8,000A. The integration of automated multi-stage current ramping prevents localized burns when immersing expansive extrusions into sulfuric acid baths.
Defense, Aviation, and Precision Component Anodizing: Engineering facilities processing aerospace fittings, automotive parts, and defense structural alloys require hard-coat anodizing reaching up to 100V–150V at lower current densities. These operations depend on programmable soft-start current regulation and pulse features to control heat generation at the substrate interface.
Electrochemical Remediation and Hydrometallurgy: Beyond traditional anodizing, facilities associated with mineral processing and metal recovery in the Mitrovica basin utilize high-current electrolysis supplies with automatic polarity reversal. Polarity switching clears scaling on subsea-grade titanium electrodes without manual acid rinsing, cutting system downtime.
3. Modernization & Regional Industrial Trends (2025–2030)
Mitrovica is experiencing gradual modernization of light manufacturing, metal fabrication, and assembly lines serving both local and European Union markets. These developments drive three technical shifts in rectifier procurement:
Automation Integration via Industrial Fieldbus: Manual potentiometers are being replaced by automated manufacturing controls. Rectifiers deployed in modern plants must feature isolated RS-485 Modbus, Profibus, or 0–10V analog communication loops to interface with central PLC cabinets for complete batch tracking and quality logging.
Harsh-Environment Sealing: Plating and anodizing facilities feature corrosive airborne mists containing sulfuric, chromic, or nitric acids. Standard industrial cabinets experience rapid internal failure under these conditions. Next-generation systems feature separated air ducts or closed-loop water-cooling schemes, isolating IGBT switching modules, drive circuitry, and control PCBs inside IP54/NEMA 12 enclosures.
Decarbonization and Grid Power Quality Compliance: Rising industrial utility rates across the Balkans make high power factor (>0.93) and minimized harmonic distortion critical to avoiding penalty surcharges from electrical distribution operators.
| Anodizing Application | Typical DC Output | Cooling Design | Critical Control Capability |
|---|---|---|---|
| Type II Architectural Anodizing | 12V – 24V | 1,000A – 6,000A | Forced Air / Water | Constant Current Ramp, Bath Temperature Feedback |
| Type III Hard Anodizing | 60V – 100V | 500A – 3,000A | Closed-Loop Water | Voltage Step-up, Pulse Superimposition, Low Ripple (≤2%) |
| Titanium Anodizing (Color & Hard) | 100V – 150V+ | 50A – 300A | Forced Air | Micro-second Response, Overvoltage Clamping |
| Industrial Electropolishing & Plating | 15V – 30V | 2,000A – 15,000A | High-Flux Water | Continuous CC/CV Mode, Heavy-Duty Busbar Connections |
4. Direct Manufacturer Advantages: Engineering & Quality Control
Working directly with Guangdong Fenvix Technology Co., Ltd. eliminates intermediate trading markups while providing deep technical alignment. Established in 2013, our production facility features over 3,000 square meters of assembly floor space supported by ISO 9001 quality management protocols and verified on-site by TÜV Rheinland.
Every anodizing rectifier built for industrial deployment undergoes strict quality assurance:
• In-House Mechanical Fabrication: Cabinet production, copper busbar milling, drilling, and tapping are completed in our workshop, ensuring thermal contact tolerances and structurally robust enclosures.
• Component Selection: We utilize European and Japanese IGBT power switches, nano-crystalline magnetic cores, and specialized electrolytic capacitors rated for high thermal endurance.
• Full Load Burn-In Testing: Prior to seaworthy packing, every unit is subjected to extended full-load burn-in cycles, monitored via multi-channel digital oscilloscopes and infrared thermal imaging to guarantee electrical stability.
• Flexible Customization with No MOQ: Whether you require a single 150V/50A prototype for titanium anodizing or multiple 15,000A water-cooled units for automated processing lines, we manufacture to your required input voltage (e.g., 380V, 400V, 415V, 480V 50/60Hz).
Certified Integrity
ISO 9001 certified manufacturing, CE, RoHS, LVD, and EMC verified compliance, with on-site factory verification by TÜV Rheinland.
Custom Engineering
Full OEM/ODM manufacturing capability. Tailored busbars, custom cooling paths, specific communication interfaces, and precise voltage spans.
Global Logistics
Exporting to over 4 continents with support for FOB, CIF, EXW, and DDP terms, paired with international technical guidance.