Engineered Rectification Systems for Hardcoat, Bright & Titanium Anodizing
Delivering high-current switch-mode architecture, sub-1% low ripple output, and microsecond-level CC/CV regulation tailored to precision metal treaters across Maribor and neighboring Austrian metallurgical hubs.

12V 15V 5000A 6000A 75KW Water Cooled Rectifier
- Current Range0–6000A Adjustable
- Voltage Output12V / 15V Digital CV/CC
- Cooling TopologyClosed-Loop Deionized Water
- Efficiency≥ 90% (Full Load)

100A–3000A Modular Anodic Oxidation Rectifier
- Current Rating100A to 3000A Continuous
- Voltage Sweep12V / 24V / 48V DC
- Current Density ControlProgrammable Multi-Step Ramp
- Ripple Factor≤ 2% RMS Low Harmonic
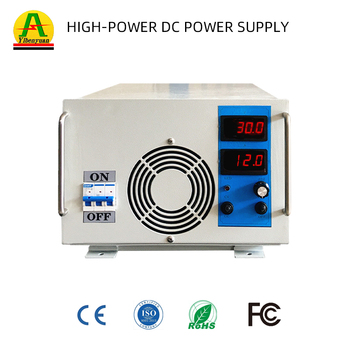
Titanium Alloy Anodizing 150V 50A Source
- Output Ceiling150V DC High Voltage Sweep
- Current Limit50A Ultra-Stable Constant Current
- Target MetallurgyTi-6Al-4V Medical & Aero
- Control BusRS485 / Modbus-RTU / 0-10V

12V 4000A 48kW IGBT Anodizing Rectifier
- Primary Output12V DC @ 4000A Continuous
- Power Conversion48kW High-Frequency Switchmode
- Chassis TypeIP54 Sealed Electronics Enclosure
- Thermal ControlForce Air Duct Isolation

8000A 12V Water-Cooled Hard Anodizing Unit
- DC Capability12V @ 8000A Constant Load
- Cooling MediumLiquid Cold-Plate Exchanger
- Duty Rating100% 24/7 Heavy Chemical Duty
- ProtectionOver-temp, Short, Phase Loss

48V 625A Auto-Polarity Reversing Power Unit
- Nominal Capacity30kW (48V / 625A)
- Switching DynamicSolid-State Polarity Reversal <10ms
- Cycle Timer4-Segment Forward/Reverse Cycle
- ApplicationElectropolishing & Pre-Treatment

300kW 20V 15,000A Heavy-Duty DC Rectifier
- Current Amplitude15,000A Continuous DC
- Voltage Range0–20V Micro-Stepped CV/CC
- Primary Grid380V/400V/440V 3-Phase 50Hz
- ComplianceCE LVD, EMC, ISO 9001 Factory

5kW Programmable E-Coat & Sealing Power Source
- Voltage Handling0–300V Adjustable Ramping
- Operating ModesMulti-Step Voltage Soft Ramp
- Process SuitabilityElectrophoretic Lacquer & Sealing
- Digital RemoteDry Contacts & Modbus Architecture
Technical Sizing & Ripple Management for Industrial Maribor Anodizers
Maribor, recognized as the industrial heart of northeastern Slovenia and the Podravska economic basin, serves as a mission-critical sub-tier manufacturing hub supplying German, Austrian, and northern Italian supply chains. From structural lightweighting components produced in the Kidričevo aluminum corridor to high-tolerance automotive powertrain assemblies and medical implants, surface finishing operations in the Drava region face rigorous European structural criteria. High-frequency switch-mode power supplies (SMPS) utilizing insulated-gate bipolar transistor (IGBT) technology have fundamentally displaced conventional silicon-controlled rectifiers (SCR/thyristors) across Maribor's premium metal finishing facilities.
The primary electrochemical driver behind this operational migration lies in voltage ripple attenuation and current regulation speed. Traditional 50Hz thyristor systems produce high residual low-frequency ripple (often 5% to 8% RMS) when dialed down from maximum voltage ratings. In sulfuric acid anodizing (Type II and Type III Hardcoat per MIL-A-8625 or ISO 10074), low-frequency ripple induces excessive localized Joule heating within the microscopic barrier layer, causing localized pore dissolution, micro-cracking, burnt rack contact tips, and non-uniform anodic film growth. Fenvix custom switch-mode rectifiers operate at switching frequencies from 20kHz to 40kHz, ensuring that total current ripple stays strictly below 1% to 2% across 10% to 100% of the operational range.
| Performance Metric | Legacy SCR (Thyristor) | Fenvix High-Frequency IGBT |
|---|---|---|
| AC-to-DC Conversion Efficiency | 68% – 76% (poor at lower output) | 89% – 93% continuous |
| Ripple Factor (Low Load) | 8% – 15% RMS (degrades oxide) | ≤ 1% to 2% stable across span |
| Power Factor (cos φ) | 0.65 – 0.75 (harmonic penalties) | ≥ 0.94 – 0.98 built-in PFC |
| Response Time (Step Ramp) | 100ms – 300ms | < 5ms microsecond transient |
| Footprint & Weight | 100% base index (heavy oil/air) | 35% – 45% of SCR cabinet volume |
For Maribor's extrusion coaters, pulse-reverse capability further transforms hardcoat operations. By reversing current polarity for precise millisecond bursts, the rectifier clears depleted hydrogen cations from deep micro-pores, allowing bath temperatures to be elevated from 0°C to 8°C–10°C without risk of film burning. This significantly reduces refrigeration electrical loads for Maribor plant operators while boosting Rockwell C micro-hardness past 60–65 HRC.
Localized Application Scenarios in Podravska & Eastern Slovenia
Targeted electrochemical power architectures matched with regional metallurgical workflows, export mandates, and shop-floor operating conditions.
Automotive Structural Castings & EV Busbars
Tier-1 and Tier-2 suppliers clustered around Maribor, Celje, and Ptuj manufacture structural lightweight die-cast aluminum brackets, battery tray housings, and liquid-cooled EV motor inverter covers. These applications demand uniform Type II chromic-free anodizing with tight salt-spray corrosion resistance (>1,000 hours per ASTM B117). Fenvix constant-current digital rectifiers ensure repeatable barrier layer formation across high-silicon aluminum cast alloys (A380, ADC12), preventing localized arc breakdown.
Extruded Architectural & Glazing Profiles
Tied closely to the downstream processing of billets from Kidričevo, Slovenian architectural extrusion houses operate automated vertical and horizontal dip-tanks. These high-volume lines require 6,000A to 12,000A rectifiers running continuous shifts. Fenvix water-cooled switch-mode units operate flawlessly inside aggressive acid mist environments, eliminating fan intake vulnerabilities and ensuring consistent film thickness (±1μm) across standard 6.5-meter architectural profiles.
Orthopedic & Dental Titanium Color Anodizing
Precision medical device engineering shops throughout eastern Slovenia utilize titanium alloy micro-machining for orthopedic pins, bone screws, and dental fixtures. Fenvix 150V programmable constant-current DC rectifiers allow micro-stepped, high-voltage sweep control for electrochemical oxidation (AMS 2488 Type II / ISO 5832-3). This precise voltage profiling ensures distinct optical interference coloring, complete surface passivation, and superior biocompatibility without chemical dyes.
Toolmaking, Mold Machining & Hardcoat Finishing
Maribor's celebrated heritage in precision machine tool manufacturing and plastic injection mold fabrication utilizes specialized aluminum components (such as 7075-T6 and 6082-T6 tooling plates). Achieving thick hardcoat layers (>50μm) without crazing or burning requires our 10-step automatic current ramping programs. Fenvix units slowly elevate voltage as the dielectric resistance of the growing anodic oxide layer increases, avoiding destructive thermal runaway.
Surface Preparation, Etching & Electropolishing
Before anodizing, high-spec components undergo alkaline cleaning, chemical etching, and deoxidation. Fenvix bi-directional and polarity-reversing DC power supplies allow Maribor finishing shops to integrate automated electrolytic descaling and electropolishing routines into the same line. Switching anode/cathode polarity via solid-state IGBT bridges removes persistent surface silicates and iron residues, establishing flawless baseline reflectivity prior to final anodizing.
Evolving Industrial Trends in Maribor & The Wider Podravska Region
Manufacturing in Maribor and northern Slovenia is experiencing a structural shift accelerated by European Green Deal mandates, rising energy tariffs, and the digital transformation of metal surface treatment (Industry 4.0). Factory managers can no longer absorb the electrical penalties and process variabilities imposed by antiquated electrical rectifiers.
Three pivotal macroeconomic trends are directly impacting capital equipment selection across Maribor surface finishing installations:
- • Grid Decarbonization & Peak Load Mitigation: With Slovenian industrial energy charges structured around high peak-demand penalties and cos φ power factor enforcement by utilities like Elektro Maribor, Fenvix rectifiers with active power factor correction (≥0.94) and high efficiency (>90%) provide substantial operational savings over legacy transformers that routinely drop power factors below 0.70.
- • Stringent REACH Compliance & Non-Chrome Chemistries: Transitioning away from hexavalent chromium (chromic acid anodizing - CAA) to modern thin-film sulfuric acid-boric acid (SBAA) or tartaric-sulfuric acid (TSA) processes requires extraordinarily tight voltage tolerance (±0.2V). Fenvix switch-mode units ensure dynamic stabilization against supply line fluctuations.
- • Fully Traceable SCADA & MES Integration: Exporting to German OEMs demands full bath-level data logging. Every Fenvix unit comes equipped with isolated RS485 Modbus-RTU, Profibus, or standard analog 0–10V/4–20mA interfaces for real-time reporting of amp-hours, voltage ramps, bath temperature telemetry, and fault tracking.
Process Capability Comparison Matrix
How high-frequency IGBT rectification enhances specific anodic processes across Maribor shops:
Reduces dye-leaching problems by creating strictly parallel, uniform pore channels with zero low-frequency striations.
Constant-current mode ramps voltage up to 60V–80V as barrier layer resistance surges, maintaining exact current density without pitting.
High voltage switch-mode architecture (up to 400V–800V DC) tailored for advanced ceramic oxide conversion on magnesium and light alloys.
Why Maribor Procurement Teams Partner Directly with Fenvix
Combining direct OEM pricing, fully bespoke electronic engineering, and verified European export reliability since 2013.
True Factory OEM Engineering
We are not intermediate export traders. Operating out of our 3,000m² production complex in Guangdong, our in-house mechanical and electrical engineering departments handle busbar fabrication, sheet metal punching, high-frequency transformer winding, and complete PCB surface mounting under strict ISO 9001 quality controls.
TÜV On-Site Verified Facility
Our operational capability, electrical test labs, and supply chain integrity are independently audited and verified on site by TÜV Rheinland. Selected power supply lines carry verified CE conformity, meeting European Machinery (MD), Low Voltage (LVD), and Electromagnetic Compatibility (EMC) Directives required for seamless installation in Slovenia.
Robust Marine & Corrosive Protection
Surface finishing plants run hot, humid, and acidic atmospheres. Fenvix anodizing rectifiers feature dual-chamber physical enclosure layouts: sensitive microcontroller and control circuitry reside in a sealed, conformal-coated compartment, while power semiconductor heatsinks are cooled via isolated forced-air tunnels or sealed liquid-cooling cold plates.



Frequently Asked Questions by Maribor & Slovenian Industrial Buyers
Key technical, commercial, and operational considerations when importing industrial DC rectifiers from Fenvix.