Precision DC Power Supplies & Rectifiers for Industrial Deployments
Engineered for Plzeň's electroplating lines, EV testing labs, automated manufacturing cells, and aviation facilities. Designed for continuous duty (100% duty cycle) with modular scalability.

12V/15V 6000A 75kW Water-Cooled DC Rectifier

12V 4000A 48kW High-Frequency Plating Unit

8000A 12V High-Current Galvanizing DC Supply

800V 50A 20kW Programmable DC Test Source
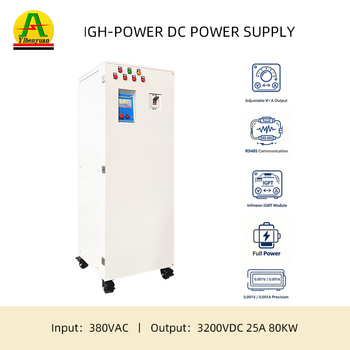
80kW 3200V High-Voltage Capacitor Charger
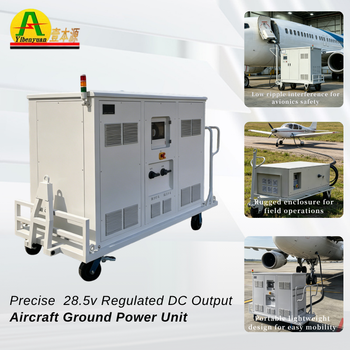
28.5V DC Mobile Aircraft Ground Power Unit
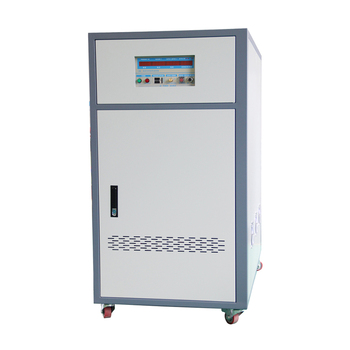
400Hz Solid-State Static Frequency Converter

48V 625A Auto-Polarity Reversing Source
Engineering Context: Power Conversion Demands in Plzeň
The Plzeň industrial basin (Plzeňský kraj) represents one of Central Europe's dense engineering clusters. From heavy machinery and rail propulsion plants at Borská Pole to high-precision automotive supply chains along the D5 corridor, localized operational challenges require robust power conversion topologies.
Rail Rolling Stock & Heavy Traction
Plzeň is internationally recognized for electric locomotives, light rail vehicles (trams), and trolleybus systems. Traction component test beds demand high-power programmable DC sources capable of simulating overhead line voltage fluctuations (600V DC, 750V DC, up to 3000V DC). Our heavy-duty DC units provide dynamic ramp control, bidirectional energy feedback options, and low-ripple characteristics necessary to validate auxiliary converters and DC traction motor insulation.
Automotive Tier-1 Surface Coating & Galvanizing
Serving OEM plants across the Czech-Bavarian industrial corridor, surface coaters across West Bohemia face strict anti-corrosion specifications. Our high-frequency switch-mode rectifiers supply exceptionally uniform current density across large cathode jigs, eliminating thermal stratification and nodule formation in chrome, zinc-nickel, and decorative anodizing tanks. Water-cooled designs isolate internal power electronics completely from ambient corrosive acid mists.
EV Power Electronics & Battery Module Aging
As tier-1 powertrain and battery suppliers expand production along the D5 motorway network, R&D centers require precise DC sources for cyclic charge-discharge validation and inverter stress-screening. Fenvix units offer high slew rates (<5ms 10% to 90% rise time), sub-0.1% setpoint accuracy, and seamless integration into automated test benches via standard industrial fieldbus architectures.
Industrial Wastewater Treatment & Descaling
Stringent European environmental directives (Water Framework Directive) force manufacturing facilities around Plzeň to improve closed-loop wastewater recovery. Fenvix auto-polarity reversing power supplies prevent cathodic scaling in electrocoagulation, electrochemical precipitation, and advanced oxidation cells without requiring expensive and corrosive chemical wash downtime.
Aviation MRO & Subsystem Testing
Regional aerodromes and general aviation service facilities require ultra-clean, transient-free ground electrical supplies. Fenvix solid-state 400Hz frequency converters replace outdated rotary converters, eliminating acoustic noise, mechanical vibration, and continuous brush servicing while providing tight voltage stability (±1%) for sensitive avionics, radar racks, and turboprop starting sequences.
Technical White Paper: Legacy Thyristor vs. Fenvix High-Frequency IGBT
For engineering directors and technical procurement managers upgrading Czech production facilities, understanding topology trade-offs is essential to long-term lifecycle ROI and energy footprint reduction.
| Operational Metric | Traditional SCR (Thyristor) Rectifier | Fenvix High-Frequency IGBT Technology | Engineering Advantage in Plzeň Operations |
|---|---|---|---|
| Electrical Conversion Efficiency | 68% – 76% (Phase angle firing losses) | 90% – 93% across 30% to 100% load | Substantial electricity cost reductions under European industrial power tariffs. |
| Output Current Ripple | High (5% to 8% RMS without giant chokes) | Ultra-low (≤ 2% RMS native ripple) | Superior metal crystal density, lower porosity, and faster electrodeposition rates. |
| Power Factor (cos φ) | Degrades to 0.5–0.7 at low output voltages | Constant ≥ 0.94 throughout full voltage control range | Avoids penalty charges from local grid operators (ČEZ Distribuce) for reactive power. |
| Physical Footprint & Weight | Massive, requires floor-reinforced foundation | 1/3 the volume and weight of equivalent SCR setups | Frees up valuable plant floor space within existing factory boundaries. |
| Response Dynamics | Slow (100–300ms reaction times) | Microsecond-level switching (< 20ms full scale) | Immediate arc suppression, minimizing rejected electroplated or tested batches. |
Emerging Power Supply Trends in the West Bohemia Market
Procurement teams across the Czech Republic are moving beyond pure initial-cost purchasing, evaluating systems through total life-cycle performance, Industry 4.0 integration, and ESG compliance.
1. Electrification & High-Voltage Transition
With Czech automotive facilities aligning with European e-mobility roadmaps, component testing has surged from legacy 12V/48V benches toward 400V, 800V, and 1200V architectures. Power supplies must feature integrated crowbar protection, rapid discharging relays, and high-voltage insulation barriers to safeguard both test technicians and high-value prototypes.
2. Factory Automation & Fieldbus Telemetry
Plzeň's smart manufacturing plants operate sophisticated MES (Manufacturing Execution Systems). Standalone analog control knobs are being replaced by RS485 Modbus, Profinet, and Ethernet/IP protocols. Our equipment enables cycle logging, millisecond error-stamping, and real-time voltage/current streaming directly into production dashboards.
3. Aggressive Thermal Efficiency & Decarbonization
High baseline electricity costs across Central Europe make heat loss intolerable. Upgrading from legacy transformer rectifiers to IGBT switch-mode topologies amortizes system capital expenditure within 12 to 18 months via direct kWh savings, while reducing HVAC facility cooling loads in enclosed workshops.
Guangdong Fenvix Technology: Manufacturing & Engineering Credentials
Headquartered in Guangzhou, Guangdong, Fenvix has served as a specialized original manufacturer of heavy industrial power systems since 2013, combining complete in-house sheet-metal fabrication with rigorous laboratory testing.
Years Industrial R&D
Founded in 2013, our specialized engineering focus remains solely on non-standard, heavy-current, and high-voltage power conversion equipment.
Integrated Production Floor
Housing our own plate shearing, CNC punching, milling, tapping, cabinet assembly, and multi-bay burn-in testing bays under one roof.
On-Site Verified Facility
Factory facilities, manufacturing capabilities, and quality controls independently verified on-site by TÜV Rheinland inspectors.
Single Prototype Engineering
We actively support 1-set custom prototype builds for specialized European engineering projects, R&D pilots, and OEM machinery integrations.




Procurement & Technical FAQ for Czech Industrial Buyers
Clear, direct answers regarding grid compatibility, shipping logistics, spare parts, and customization specifications.
Are Fenvix units directly compatible with Czech grid electrical standards?
Yes. All units configured for the Czech and wider Central European market are built to accept standard 400V AC ±10% three-phase, 50Hz mains power (or 230V single-phase for lab units). Input EMI filters comply with EN 61000-6-2 (Immunity for industrial environments) and EN 61000-6-4 (Emission standard for industrial environments).
What documentation and CE compliance certificates accompany shipments to the EU?
Every unit ships with a dedicated CE Declaration of Conformity referencing the Low Voltage Directive (LVD 2014/35/EU) and Electromagnetic Compatibility Directive (EMC 2014/30/EU). In addition, shipments include factory routine test certificates, comprehensive wiring diagrams, calibration protocols, and English language user manuals.
What is the typical lead time and customs delivery process into the Plzeň region?
Standard modular units generally complete assembly, burn-in testing, and inspection within 2 to 4 weeks. Delivery terms can be arranged under DAP or DDP (Delivered Duty Paid) Plzeň directly to your facility, handling EU customs clearance, customs duties, and cross-border logistics via direct air express or consolidated sea freight into European ports.
When should we configure water cooling versus forced-air cooling?
For installations in electroplating, anodizing, or hot chemical environments where the air contains acid aerosols or high particulate counts, water cooling (closed-loop heat exchanger or tap water) is highly recommended. It completely seals internal IGBTs and driver cards inside an IP54 enclosure. For clean test laboratories, forced-air cooling with front-to-rear ducting is standard and reduces initial plumbing complexity.
How does Fenvix support technical servicing, spare parts, and warranty replacements?
We provide a standard 12-month full warranty backed by modular field-replaceable subassemblies. Because our systems use standardized internal driver boards, power modules, and control interfaces, client maintenance teams can swap out components quickly. Remote engineering support via video link and direct electrical engineering consultation ensures zero operational downtime.
Can you provide custom polarity reversing, pulse plating, or high-voltage ramping profiles?
Yes. Custom firmware controls are a core competency. We configure precise pulse parameters (frequency up to 10kHz, adjustable duty cycles), multi-stage programmable current ramps for hard anodizing, and millisecond-level H-bridge polarity reversals for water treatment and descaling applications directly from factory specifications.
Accelerate Your Project with Custom Industrial Power Systems
Whether you are designing a new surface finishing line, building an EV traction test bench, or modernizing an aviation maintenance bay in West Bohemia, our senior engineering team is ready to review your technical parameters and provide full design recommendations within 24 hours.