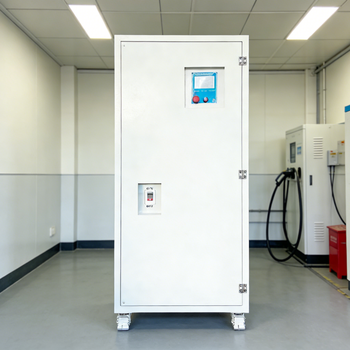
12V/15V 5000A–6000A 75kW Water-Cooled Electroplating Rectifier
- Output Power: 75kW Continuous
- Voltage / Current: 0–15V / 0–6000A
- Cooling Design: Deionized Water Cooling
- Control Architecture: Digital CV / CC Dual Mode

Precision constant current (CC) and constant voltage (CV) topologies engineered to reduce cathode burning, optimize chemical bath consumption, and handle 100% 24/7 duty cycles.
A comprehensive comparative analysis between legacy Thyristor/SCR power supplies and modern High-Frequency Switch-Mode Rectifiers (SMPS) utilizing insulated-gate bipolar transistors (IGBTs).
Acid chloride and alkaline zinc plating require consistent micro-crystallization. High-frequency rectifiers deliver a current ripple under 2% (compared to 5-10% from legacy SCRs), significantly minimizing hydrogen embrittlement, reducing pinhole porosity, and ensuring uniform zinc layer deposition across high and low current density zones.
By replacing heavy 50Hz copper transformers with high-frequency nanocrystalline magnetic cores operating at 20kHz to 50kHz, electrical conversion efficiency surges to 90–93%. Plating plants running multi-thousand-ampere lines 24/7 recover the initial capital expenditure of the machine in power bill savings within 8 to 14 months of operation.
Every Fenvix zinc plating rectifier integrates closed-loop DSP logic with 0.1% control resolution. Seamless connection to SCADA or centralized PLC networks is standard via RS485 Modbus, Profinet, or isolated analog 0–10V/4–20mA, recording amp-hour totals for precise automated chemical bath replenishments.
| Evaluation Parameter | Legacy Silicon Controlled Rectifier (SCR/Thyristor) | Fenvix High-Frequency IGBT Plating Rectifier | Operational Impact on Plating Workshop |
|---|---|---|---|
| Conversion Efficiency | 68% – 76% (Low efficiency at low current) | 90% – 93% Efficiency | Cuts plant electrical utility expenditure by 15% to 25% annually. |
| Current Ripple Rate (RMS) | 5% to 15% (Requires heavy inductor filters) | < 2% Ultra-Low Ripple | Prevents burnt edges; yields mirror-like zinc crystal lattice. |
| Physical Footprint & Weight | Massive oil/air tanks; weights reach 1,200kg+ | Compact Modular (~280kg) | Saves 65% floor area; enables mounting immediately adjacent to tanks. |
| Dynamic Response Time | Sluggish response (200ms to 400ms) | < 10ms High-Speed Loop | Eliminates initial over-voltage spikes during rack submersion. |
| Environmental Resistance | Susceptible to acid bath corrosion | IP54 Fully-Sealed Deionized Water Cooled | No acid vapors circulate internally; protects internal electronics. |
Analysis of global electroplating plant capital expenditure (CAPEX) criteria shifting towards sustainability, intelligent telemetry, and ultra-high reliability.
In high-throughput barrel zinc lines and alkaline zinc-nickel processes, acidic airborne droplets drastically degrade air-cooled power boards within 2 years. Global purchasers are shifting aggressively towards closed-circuit, water-cooled IGBT power systems (IP54/NEMA 4X equivalent). Eliminating internal cooling fans completely prevents toxic chemical vapors from contacting critical electronic components, doubling mean time between failures (MTBF).
Pulse-reverse plating (PRP) is transitioning from precious metal labs into high-end automotive fasteners and anti-corrosion chassis hardware plating. Periodic micro-second current interruption dislodges trapped hydrogen bubbles before zinc occlusion occurs, mitigating post-plate hydrogen embrittlement bake requirements for high-tensile steel (Grade 10.9 & 12.9) without sacrificing bath throughput.
Exporting electroplated automotive and solar structural components to Europe and North America now demands verification of low-carbon manufacturing. Modern rectifiers featuring continuous energy metering and power-factor correction (>0.95 PF) minimize total kVA demand charges, protecting Tier-1 electroplating processors against escalating carbon tariffs.
A true original equipment manufacturer (OEM/ODM) providing direct engineering dialogue, precision copper manufacturing, and uncompromised quality assurance.
Our 3,000m² manufacturing facility in Guangdong, China has been audited on-site by TÜV Rheinland. We enforce incoming component IQC, strict assembly controls, and mandatory 100% full-load burn-in testing before export authorization.
Unlike assemblers who buy generic enclosures, Fenvix maintains internal plate shearing, CNC punching, milling, drilling, and tapping capabilities. We fabricate thick pure T2 electrolytic copper conductors, ensuring minimal voltage drops and optimal thermal equilibrium.
We believe in supporting innovative engineering from initial pilot runs to complete plating lines. We maintain a strict No-MOQ policy: single-unit custom engineering builds for prototypes receive the exact same engineering care as multi-unit automated line packages.
Communicate directly with experienced power electronics specialists rather than commissioning agents. We verify tank sizing, bath electrical conductivity, busbar length losses, and cooling heat dissipation before issuing a technical drawing and quote.
Seamless cross-border procurement backed by clear incoterms: FOB, CIF, CFR, EXW, FCA, and complete DDP door-to-door delivery with customs cleared. We process multi-currency settlements including USD, EUR, GBP, AUD, CAD, JPY, and CHF.
Every delivered shipment contains detailed circuit schematics, calibration certificates, oscilloscope load-testing ripple verifications, and comprehensive spare parts lists, minimizing installation and commissioning cycles overseas.
Essential answers regarding engineering specifications, thermal management selections, communication protocols, and global export packaging.
Connect directly with our senior power supply designers for custom sizing, CAD busbar drawings, and a competitive factory quotation delivered within 24 hours.