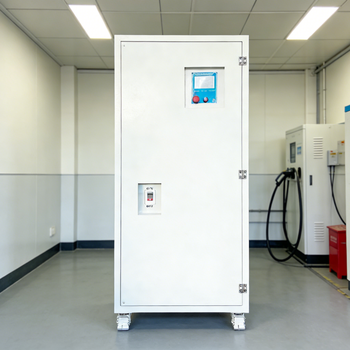
Precision IGBT Switch-Mode DC Rectification Architectures (6V–3200V / up to 15,000A) Engineered for Hard Chromium, Decorative Trivalent Plating, Anodizing, and High-Duty Electrochemical Applications.
Engineering Catalog & Selection
Industrial Hard Chrome & Electroplating Rectifiers
Customized switch-mode DC power supplies built to withstand corrosive acid-mist atmospheres. Standardized with Constant Voltage (CV), Constant Current (CC), digital touch interfaces, and intelligent fieldbus automation.
Switch-Mode IGBT vs. Traditional Thyristor (SCR) Rectifiers
Precision electrodeposition of industrial hard chromium and micro-crack decorative chrome demands rigorous current density regulation. Compare the operational characteristics of modern high-frequency switch-mode power supplies against legacy line-frequency SCR units.
Performance Vector
Fenvix High-Frequency IGBT Rectifier
Traditional Thyristor (SCR) Rectifier
Impact on Chrome Plating Quality
Output DC Ripple (RMS)
✔ ≤ 1% to 2% Peak-to-Peak
5% to 8% (requires massive LC filters)
Eliminates burning, burning at high current density edges; optimizes crack-density.
Conversion Efficiency
✔ 90% – 93% Typical
70% – 78% Typical
Reduces utility electrical costs by up to 20–25% under 24/7 continuous operation.
Dynamic Response Time
✔ < 5 ms (20kHz–40kHz Switching)
60 ms – 100 ms (50/60Hz Mains Cycle)
Instantly compensates for bath load shifts, preventing cathode layer starvation.
Footprint & Cabinet Weight
✔ Ultra-Compact (1/3 Weight & Size)
Extremely Heavy (Massive Iron Cores)
Saves premium plating shop floor space; simplifies tank-side mounting to reduce copper busbar run losses.
Power Factor (cos φ)
✔ ≥ 0.94 (Low Harmonic Distortion)
0.65 – 0.75 (Degrades severely at low output)
Avoids utility kVA penalties; eliminates expensive external power factor correction banks.
Corrosive Acid Resistance
✔ Sealed IP54 / Deionized Water Cooling
Open Forced Air with internal dust pull
Protects sensitive silicon and driver circuits against violent chromic acid (H₂CrO₄) mist erosion.
Enterprise Manufacturing Capabilities
Direct Factory Engineering Excellence by Fenvix
Since 2013, Guangdong Fenvix Technology Co., Ltd. has delivered non-standard, custom-engineered power solutions across North America, Europe, Southeast Asia, and the Middle East. Sourcing directly from an accredited OEM/ODM eliminates middleman markups and guarantees precision engineering alignment.
In-House Metal Fabrication & CNC Machining
Unlike assembly-only vendors, Fenvix controls every mechanical step within our 3,000m² facility. Equipped with plate shearing machines, punching, milling, drilling, and tapping units, we fabricate our own structural cabinets, corrosion-resistant chassis, and heavy-gauge solid T2 copper busbars, achieving unmatched thermal coupling and lead-time control.
TÜV Rheinland Audited & ISO 9001 Certified
Our quality management workflow enforces incoming component qualification (IQC), in-process assembly quality verification (IPQC), and 100% full-load burn-in testing under simulated environmental extremes. Factory capabilities, trade integrity, and engineering equipment have been comprehensively confirmed via on-site assessments by TÜV Rheinland.
Zero-MOQ Tailored ODM Engineering
Whether you require a single 150A prototype for laboratory chemical testing or twenty 10,000A water-cooled rectifiers for automated continuous hard chrome lines, we offer full design-based customization with no minimum order requirements. Input voltages (208V, 380V, 415V, 480V) and communication interfaces are built directly to spec.
Advanced Nanocrystalline Core Magnetic Circuits
We wind proprietary ultra-microcrystalline (nanocrystalline) soft magnetic transformers that drastically mitigate eddy-current and core saturation losses under high-frequency operation (up to 40kHz). This architecture enables sustained 100% duty cycles in ambient temperatures reaching 45°C without thermal degradation.
Global Field Support & Flexible Trade Terms
Fenvix delivers turnkey logistics across EXW, FOB, CIF, DDP, and door-to-door express. We maintain multi-currency transaction accounts (USD, EUR, GBP, AUD, CNY) and back our equipment with free pre-sales system sizing, full schematics, remote oscilloscope commissioning assistance, and third-party certified on-site technical support.
Comprehensive Compliance Certification
Our industrial power units are engineered to meet strict international standards, including CE Marking conformity under the Low Voltage Directive (LVD 2014/35/EU), Electromagnetic Compatibility (EMC 2014/30/EU), and RoHS environmental safety. Factory inspection reports and dielectric insulation test records accompany every delivered crate.
Industry White Paper Analysis
Future Technological Trends in Chrome Plating Rectifiers
The surface finishing sector is undergoing rapid transformation driven by environmental mandates (such as REACH restrictions on Cr6+), higher aerospace metallurgical standards, and digital automation. Sourcing strategies must adapt to the following technological paradigms.
1. Trivalent (Cr3+) Hard Chromium Demands
The global transition from hexavalent chromium to environmentally safer trivalent formulations requires unprecedented current stability. Trivalent baths operate at narrower electrochemical windows where voltage dips cause instantaneous passive layer formation. Modern rectifiers incorporate ultra-low ripple (<1%) and millisecond-level response to maintain uniform deposition rates without dark burning.
Ripple Threshold: < 1% Peak-to-Peak
2. Programmable Pulse & Pulse-Reverse (PRC)
High-frequency periodic pulse reverse current (PRC) is replacing flat DC in demanding aerospace and hydraulic cylinder plating. By alternating forward deposition with microscopic reverse deplating pulses, the cathode diffusion layer is continuously replenished. This eliminates hydrogen embrittlement, reduces micro-cracking defects, and increases deposit microhardness up to 1100 HV.
Microhardness Boost: +15% to 25%
3. Closed-Loop Deionized Water Cooling
Air-cooled rectifiers draw acidic ambient fumes across sensitive internal power modules, accelerating circuit board corrosion and short circuits. The industry standard is shifting toward sealed IP54/IP55 water-cooled enclosures. Circulating deionized water directly through copper chill-blocks removes thermal heat while isolating internal electronics completely from ambient corrosive bath fog.
MTBF Extension: > 80,000 Hours
4. IIoT, Modbus-TCP & Predictive Maintenance
Modern plating plants require complete traceability for automotive and defense compliance. Modern rectifiers integrate high-speed industrial Ethernet, Profinet, and Modbus-TCP architectures. Real-time logging of amphour consumption, bath impedance, thermal heatsink gradients, and ripple anomalies enables automated chemistry replenishment and predictive IGBT failure alerts.
SCADA & Industry 4.0 Native
Strategic Sourcing Guide
Global Sourcing & Procurement Trends for Industrial Rectifiers
B2B procurement executives are evaluating power electronics not merely as capital assets, but as strategic drivers of electrical efficiency, production reliability, and operational lifecycle cost reduction.
Total Cost of Ownership (TCO) vs. Initial CapEx
Operating a 10,000A / 12V hard chrome tank 24 hours daily consumes over 1,000,000 kWh annually. Upgrading from a legacy 75% efficient SCR unit to a 92% efficient high-frequency IGBT rectifier saves more than 200,000 kWh each year per tank. Procurement teams now recognize that energy savings frequently offset the entire capital acquisition price within 14 to 18 months of commissioning.
Payback Window: < 18 Months
Modular N+1 Redundancy Architectures
In high-throughput plating operations, unexpected rectifier outages cause severe plating stratification, requiring costly workpiece stripping or outright scrap. Modern procurement mandates modular N+1 architecture. If one 2,000A sub-rack module triggers a thermal fault, the remaining parallel modules instantaneously increase current to maintain the required cathode density without tank interruption.
Zero Unscheduled Line Stops
Direct OEM/ODM Strategic Partnerships
Procurement directors are bypassing regional distributor markups to collaborate directly with verified manufacturing plants like Fenvix. Working directly with factory design teams ensures exact matching of copper busbar exit configurations, tank drop locations, local utility voltages (e.g., 480V 60Hz North America vs. 400V 50Hz Europe), and custom software ramp protocols.
Direct Factory Cost Advantage
Regulatory Compliance & Traceability Auditing
Aerospace (Nadcap), automotive (CQI-11), and medical plating specifications mandate stringent calibration records and certified power quality. Buyers are demanding validated test certificates, CE conformity (LVD/EMC), RoHS compliance, and verifiable factory audit documentation (TÜV Rheinland) prior to issuing letters of credit or production approvals.
Technical guidance for manufacturing engineers, process chemists, and sourcing managers preparing non-standard rectifier specifications.
What parameters are critical to calculate the correct rectifier amperage and voltage?
Sizing an industrial chrome plating rectifier requires four core parameters:
1. Cathode Surface Area: The total square decimeters (dm²) or square feet (ft²) of workpieces loaded into the bath simultaneously.
2. Target Current Density: Hard chromium typically requires 30 to 60 A/dm² (2 to 4 A/in²), whereas decorative trivalent or hexavalent chrome operates around 10 to 20 A/dm².
3. Tank Busbar & Distance Drops: Calculate the I²R resistive voltage drop across the copper busbars, anode hook contacts, and bath electrolyte. Most hard chrome operations require 12V to 15V output, while continuous strip or long anode configurations may require 18V to 24V.
4. Duty Factor Safety Margin: Fenvix recommends sizing your continuous operational load at 80% of the rectifier’s rated capacity to extend module lifespan.
Why is output ripple factor so critical for hard chromium deposition?
Unlike zinc or copper plating where current ripple tolerance can exceed 5%, chromium deposition exhibits exceptionally low cathode current efficiency (typically 12% to 20%).
High ripple causes current to dip below the critical threshold required to maintain the polarizing film, resulting in passivation, dull grey deposits, rough nodules, and non-uniform micro-crack density. Fenvix high-frequency IGBT rectifiers maintain ripple below 2% (and below 1% with secondary filtering options) across 10% to 100% of the output scale, guaranteeing superior Vickers hardness (>950 HV) and mirror finishes.
When should our facility select closed water cooling over forced air cooling?
Forced air cooling is economical and straightforward for light-duty, clean benchtop operations (under 500A) or when rectifiers are situated in a separate, pressurized, climate-controlled electrical switchroom.
However, for rectifiers rated above 1000A installed directly on the plating shop floor, closed-loop deionized water cooling is strongly recommended. Chromic acid mist, caustic fumes, and high ambient factory temperatures rapidly corrode cooling fans and circuit board traces in air-cooled chassis. Water-cooled systems feature sealed IP54/IP55 cabinets, transferring heat directly to chillers without drawing acid-laden air through internal components.
Can Fenvix rectifiers interface with our existing plant SCADA or PLC system?
Yes. Every Fenvix industrial rectifier can be equipped with standardized fieldbus interfaces. Standard protocols include RS485 Modbus-RTU, Profibus-DP, Modbus-TCP, and Profinet.
Additionally, we provide isolated analog interfaces (0–5V, 0–10V, or 4–20mA) for remote voltage/current setting and feedback monitoring, alongside digital dry-contact outputs for running status, fault alarms (phase loss, over-temperature, over-current), and emergency interlock stops.
What is the minimum order quantity (MOQ) and production lead time for custom units?
Fenvix maintains a strict Zero-MOQ policy. We engineer single-unit prototypes for pilot lines and specialty plating tanks, as well as production batches for multinational equipment builders.
Because we operate in-house CNC machining, metal plate shearing, and busbar processing workshops, our typical lead time for custom units (up to 6,000A) is 2 to 3 weeks, while ultra-heavy systems (8,000A–15,000A) typically ship within 3 to 4 weeks following schematic confirmation.
How does Fenvix support overseas commissioning, warranty, and replacement parts?
Every rectifier ships with comprehensive installation schematics, terminal connection maps, and an operation manual. We provide direct pre-sales technical sizing and real-time remote video commissioning support with senior electrical engineers.
Our modular hardware architecture allows easy field replacement of driver boards, control modules, and IGBT sub-assemblies. Spare parts kits are readily available for immediate global express delivery. Furthermore, on-site technical service capabilities have been independently assessed and verified by TÜV Rheinland.
Ready to Configure Your High-Performance Plating Power System?
Provide your target bath chemistry (Hard Chrome, Trivalent Chrome, Anodizing), continuous amperage, utility input voltage, and cooling preferences. Fenvix power engineers will deliver custom dimensional CAD drawings and a detailed factory quote within 24 hours.